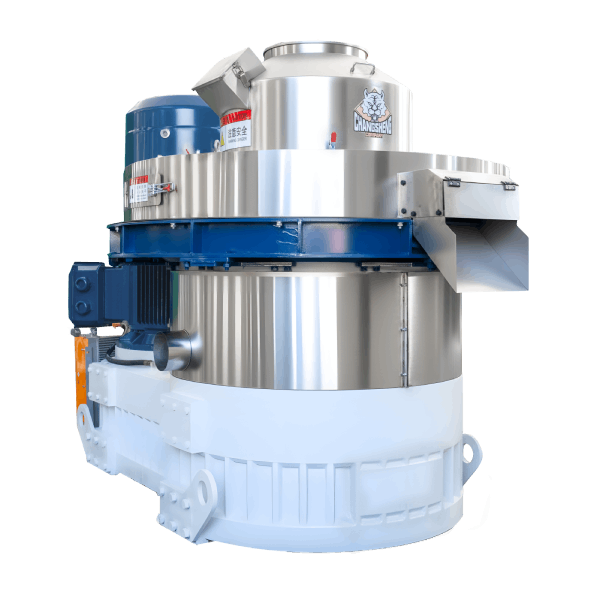
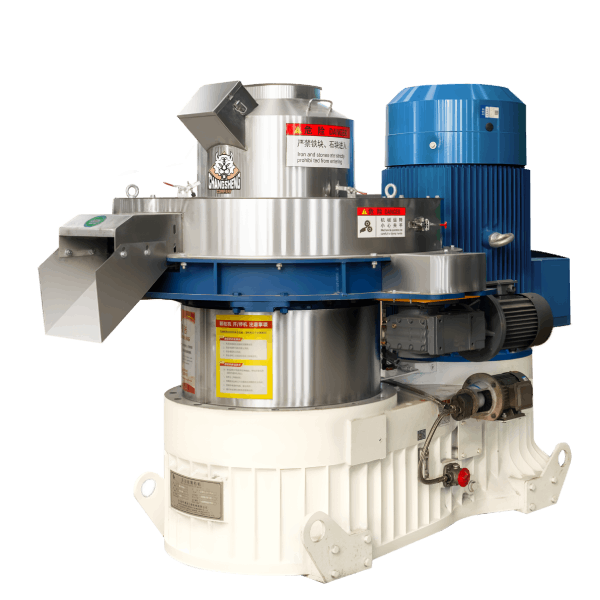
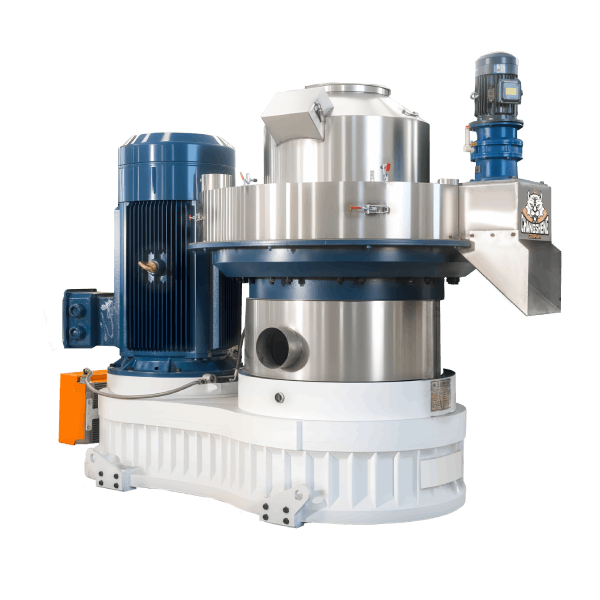
Pellet Making Machine: How to Choose the Right Machine for Your Feedstock and Production Scale
News 2026-10-04
A pellet making machine is not a single product. It is a family of machines that differ in die type, drive system, capacity, and automation. Two machines with the same nominal capacity can produce different output, different pellet quality, and different die life, depending on the feedstock and how the machine is configured.
The practical question for a buyer is not which machine is the cheapest. The real question is which machine fits the feedstock you have, the pellet quality you need, the power supply at your site, and the operating pattern of your project.
This guide explains pellet making machine types, how to choose between flat die and ring die, how feedstock affects machine selection, how capacity is stated, what determines cost, and what to confirm with the supplier before ordering. For feedstock-specific guidance such as wood, straw, rice husk, or palm fiber, see the separate material pages on this site. For the ring die machine family in detail, see the ring die pellet machine page on this site. For the general pellet mill concept, see the pellet mill guide on this site.
Pellet Making Machine vs Pellet Mill vs Pellet Machine
These three terms are often used interchangeably, but in engineering usage they differ slightly. A pellet mill or pellet machine usually refers to the core compression machine itself. A pellet making machine often refers to the machine plus its immediate feeding, conditioning, and discharge components, and sometimes refers to the whole production line. In this guide, pellet making machine is used to describe both the core machine and the surrounding configuration, because that is how buyers typically use the term in procurement.
What a Pellet Making Machine Does
A pellet making machine compresses ground material into dense cylindrical pellets using pressure and friction heat. The material is fed into the die chamber, pressed through die holes by rollers, heated by friction, and cut to length as pellets exit the die.
The machine is the core of a pellet production process. It is not the whole process. Depending on feedstock and target pellet quality, a complete line may also include a chipper, hammer mill, dryer, conditioner, cooler, screener, packing machine, and dust collection.
Pellet making machines are used for wood pellets, animal feed pellets, biomass fuel pellets, and other organic materials. The machine configuration is not the same for each application. Feed pellets, fuel pellets, and bedding pellets have different requirements for die compression ratio, conditioning, cooling, and screening.
Pellet Making Machine Types
Flat Die Pellet Making Machine
A flat die machine uses a flat plate die. It is simpler, lower in cost, and easier to maintain. It suits small capacity, varied feedstock, and intermittent operation. Flat die machines are common for small farms, workshops, and pilot projects.
Ring Die Pellet Making Machine
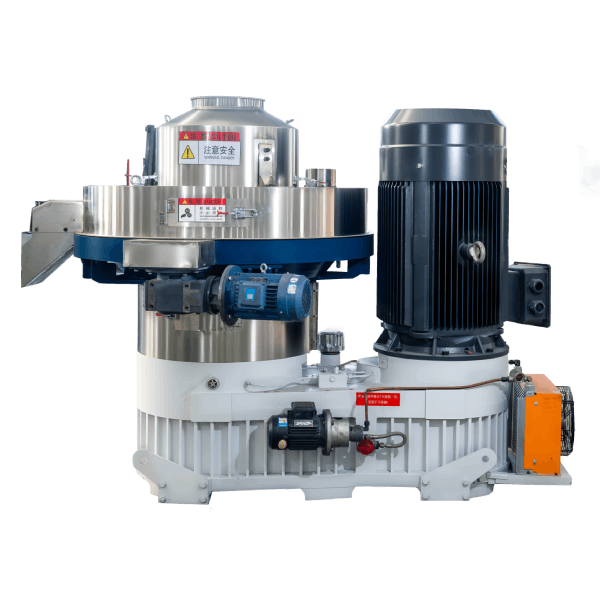
A ring die machine uses a vertical ring die. It provides higher capacity, more stable pellet quality, and better energy efficiency at scale. It suits commercial and industrial production. Ring die machines require more specialized maintenance and may need lifting equipment for die change.
Feed Pellet Making Machine
A feed pellet machine is configured for animal feed materials such as corn, soybean meal, and formulated feed ingredients. Feed pellets require feed-grade hygiene, formulation control, and usually steam conditioning. Feed pellet machines are used for poultry, cattle, pig, and aquaculture feed.
Biomass Pellet Making Machine
A biomass pellet machine is configured for biomass materials such as wood waste, agricultural residues, and energy crops. Biomass pellets require different die compression ratio, feeder design, and wear-resistant components compared with feed pellets.
Flat Die vs Ring Die Pellet Making Machine
Factor: Production scale
Flat Die: Small
Ring Die: Medium to large
Factor: Initial investment
Flat Die: Lower
Ring Die: Higher
Factor: Continuous operation
Flat Die: Limited
Ring Die: Suitable
Factor: Die structure
Flat Die: Flat plate
Ring Die: Vertical ring
Factor: Die surface area
Flat Die: Smaller
Ring Die: Larger, higher throughput
Factor: Maintenance
Flat Die: Simpler
Ring Die: More specialized
Factor: Die change
Flat Die: Easier, basic tools
Ring Die: May need lifting equipment
Factor: Typical use
Flat Die: Small farm or workshop
Ring Die: Commercial and industrial production
A flat die machine is often the better choice for small farms, workshops, and pilot projects with varied feedstock or intermittent operation. A ring die machine is often the better choice for commercial production, continuous operation, and consistent pellet quality.
How Feedstock Affects Pellet Making Machine Selection
Wood and Sawdust
Sawdust is usually the easiest wood feedstock to pelletize. Particle size is often already suitable, and the main requirement is moisture control. Wood chips and shavings require grinding before pelletizing.
Agricultural Residues
Straw, rice husk, and corn stover are more abrasive and often have lower lignin content. They usually require higher compression ratio and wear-resistant die and roller material. Grinding and drying requirements depend on feedstock condition.
Animal Feed Materials
Corn, soybean meal, and formulated feed ingredients usually pelletize more easily but require feed-grade hygiene and formulation control. Feed pellets often use steam conditioning to improve binding and pellet durability. Feed formulations usually use a lower compression ratio than biomass, because the goal is durability without excessive density.
Palm Fiber and EFB
Palm fiber and EFB have high moisture, residual oil content, and long fibers. They require shredding, drying, and oil management. EFB requires more preprocessing than palm fiber.
Other Biomass Materials
Coffee husk, peanut shell, cotton stalk, and coconut husk are more abrasive and require wear-resistant die and roller material. Each has its own moisture, ash, fiber, and mineral contamination profile.
Moisture and Particle Size
Typical target moisture before pelletizing is around 10 to 15 percent for most wood and biomass feedstocks, and around 12 to 14 percent for many feed formulations. This range depends on feedstock type, die compression ratio, and machine configuration. The exact target should be confirmed with a pelletizing test.
If moisture is too high, compression is poor, the die may block, and throughput drops. If moisture is too low, binding is poor, pellets are weak, and fines increase.
Particle size affects feeding stability, compression, pellet density, and die wear. Target particle size is usually in the range of 2 to 5 mm for biomass, depending on die specification. Feed pellets usually require finer particle size, often in the range of 1 to 3 mm, depending on animal type and feed formulation. If feedstock is too coarse, grinding is required. If too fine, bridging and die blockage risk increases.
Die Compression Ratio and Die Selection
Die compression ratio is the ratio of die hole length to die hole diameter. It determines how much resistance the material meets as it passes through the die. Higher compression ratio increases pellet density but also increases power demand and die wear.
The correct compression ratio depends on feedstock density, fiber content, moisture, and target pellet quality. Softwood and low-density materials usually require a lower compression ratio. Hardwood and high-density materials usually require a higher compression ratio. Feed pellets usually use a lower compression ratio than biomass fuel pellets. Biomass fuel pellets usually use a higher compression ratio to reach target density and durability.
Die selection should be confirmed with a pelletizing test using the actual feedstock. Die life varies widely by feedstock, so expected working hours should be confirmed with the supplier based on similar material and operating conditions, not assumed from a general figure.
Die Hole Diameter and Pellet Diameter
Die hole diameter determines pellet diameter. Common pellet diameters are 2 to 4 mm for small feed, 4 to 6 mm for poultry and cattle feed, and 6 to 8 mm for biomass fuel, with 10 mm and 12 mm available for some industrial applications. Pellet diameter should be selected against the boiler, stove, or feed system, not chosen independently. Die hole diameter and pellet diameter should be confirmed together with the supplier before ordering.
Die Temperature, Conditioning and Roller Clearance
Die temperature is the friction-generated temperature inside the die chamber. It affects binding and pellet durability. If temperature is too low, pellets are weak. If temperature is too high, material may scorch and die wear accelerates.
For feed pellets, steam conditioning is commonly used before pelletizing to raise temperature and moisture, which improves protein and starch binding. Steam conditioning parameters depend on feed formulation and target durability, and should be confirmed with the supplier and with feed formulation specialists.
For biomass pellets, die temperature is usually generated by friction, and feed rate is adjusted to keep temperature within the target range. A die temperature sensor and alarm are recommended.
Roller clearance is the gap between the roller and the die surface. If clearance is too large, material slips and output drops. If clearance is too small, rollers and die wear faster and motor load rises. Roller clearance should be set according to the supplier procedure and checked regularly.
Pellet Quality, Durability and Fines
Pellet durability and fines content are key quality indicators. Durability depends on binding, compression ratio, die temperature, moisture, and cooling. Fines are produced when pellets are weak, when cooling is insufficient, or when screening is inadequate.
For feed pellets, durability is often measured by a pellet durability index test. For biomass fuel pellets, durability and fines are key parameters for boiler compatibility and for export markets. To control durability and fines, the line should maintain correct moisture, use a die with the correct compression ratio, keep die temperature within the target range, and provide adequate cooling and screening.
Biomass Pellet Ash Content and Boiler Compatibility
For biomass fuel pellets, ash content matters for boiler design and ash handling. Ash content depends on feedstock and bark content. Clean wood has lower ash; bark, straw, and rice husk have higher ash. Boilers with ash removal systems can accept higher-ash pellets; home pellet stoves usually require low-ash pellets. Ash content should be confirmed by laboratory test for the specific feedstock.
Capacity and How It Is Stated
Pellet making machines typically range from about 30 kg/h for small flat die machines to several tons per hour for industrial ring die machines. Capacity is not a fixed number. It depends on feedstock type, moisture, particle size, pellet diameter, die specification, compression ratio, motor power, feed rate, and operating skill.
Rated capacity is only meaningful when feedstock, moisture, particle size, and die specification are stated. A capacity figure quoted without these conditions should not be treated as a guaranteed output for your project.
Required hourly capacity equals annual production target divided by annual operating hours. A capacity margin of about 20 to 30 percent is a practical starting point for feedstock variation, moisture changes, and maintenance. The exact margin depends on feedstock consistency, operating hours, and maintenance planning.
As an illustrative reference, a 500 kg/h machine running 2,000 hours per year produces approximately 1,000 tons per year. A 1 t/h machine running 4,000 hours per year produces approximately 4,000 tons per year. These figures are illustrative and should be adjusted for your actual feedstock and operating pattern.
Auxiliary Equipment for Pellet Production
Depending on feedstock and target pellet quality, a pellet production line may include:
Chipper or crusher for large pieces.
Hammer mill for grinding to consistent particle size.
Dryer for reducing moisture when it is above the suitable range.
Conditioner for adding heat and moisture, especially for feed pellets.
Pellet making machine for forming pellets.
Cooler for hardening pellets and reducing fines.
Screener for removing fines and oversize.
Packing machine for bagging or bulk loading.
Dust collection for health and explosion protection.
Not every project needs every piece of equipment. A project using dry sawdust may need only a pellet making machine, cooler, and screener. A project using wet wood chips may need a complete line with chipping, grinding, and drying. A feed pellet line may need conditioning and finer grinding.
Automation, Containerized and Mobile Configurations
A pellet making machine may be manual, semi-automatic, or automatic. Automation level affects both initial cost and labor cost. Feed pellet lines often require more complex automation for formulation control and conditioning. Biomass lines usually focus on durability, wear resistance, and continuous operation.
A pellet making machine can be supplied as a standalone unit, as part of a fixed production line, as part of a containerized line, or as part of a mobile unit. A containerized line is built into one or more shipping containers and is used for export projects, remote sites, or projects where site construction is limited. A mobile unit is mounted on a trailer or truck frame and is used where feedstock is scattered or where production is seasonal.
What Determines Pellet Making Machine Cost
Cost depends on machine type, capacity, motor power, die size and material, roller configuration, drive system, automation level, material compatibility, spare parts included, and auxiliary equipment scope.
A small flat die machine and a large ring die machine are in different price categories. A belt drive machine and a gearbox drive machine are also in different price categories. A machine for feed materials and a machine for abrasive biomass may differ in price because of die and roller specification.
Machine price is not the same as complete pellet production line cost. A complete line may include chipper, hammer mill, dryer, conditioner, pellet making machine, cooler, screener, packing machine, and dust collection. Final cost should be confirmed against a written scope of supply.
Energy Consumption and Operating Cost
Energy consumption per ton depends on feedstock type, moisture, particle size, die specification, compression ratio, feed rate, and motor efficiency. Abrasive and high-moisture feedstocks usually require more energy per ton than dry, low-density materials. Energy consumption should be confirmed with the supplier at your actual feedstock condition, not assumed from a catalog figure.
Operating cost includes raw material, power, labor, maintenance, spare parts, and downtime. Cost per ton of pellets is the figure that matters, not machine price alone.
Pellet Quality Standards and Export Documentation
For local use, pellet quality requirements are usually set by the boiler, stove, or feed system. For export or higher-grade markets, pellet quality may need to meet standards such as ISO 17225 for solid biofuels. Feed pellets may be subject to feed safety and hygiene regulations in the destination market. Some markets also use certification schemes such as ENplus for wood pellets, and some North American markets use PFI specifications.
Export documentation typically includes commercial invoice, packing list, bill of lading, certificate of origin, and declaration of conformity where applicable. Additional certification may be required by the destination country. All certification and documentation requirements should be confirmed with the supplier and with the import agent in the destination country before shipment.
Maintenance and Spare Parts
Dies and rollers are wear parts. Their life depends on feedstock abrasiveness, moisture, compression ratio, and operating conditions. For abrasive feedstocks, die and roller life may be shorter than for clean wood.
A practical spare parts plan includes at least one spare die, one or two spare roller shell sets, bearings, belts, seals, lubricants, and critical electrical spares.
Daily checks include lubrication, roller clearance, feeder condition, and motor current. Weekly checks include die and roller wear, belt tension, and electrical connections. Monthly checks include lubrication system condition, bearing temperature, and control panel inspection.
Die change frequency depends on feedstock abrasiveness, moisture, compression ratio, and operating conditions. Each die change requires production stop, die removal, roller inspection, die installation, clearance adjustment, and first production stabilization. Downtime cost depends on production rate, labor cost, and the value of lost output. A project without a spare die on site will face long downtime when the first die wears out.
Packing and Shipping Considerations
Pellet making machines are heavy equipment. Packing must protect against moisture and mechanical damage during sea transport. Frame container loading, reinforced crating, and moisture barrier film are common. The largest single piece should be identified before shipment so that lifting equipment at the destination can be planned. Shipping marks, case numbers, weight, and dimensions should match the packing list. Installation tools and special fixtures should be included. For overseas projects, documentation should include operation manual, electrical diagram, foundation drawing, and spare parts list.
Typical Project Scenario
The following summarizes typical project parameters from pellet making machine projects. Specific customer names, locations, and contact details are not included.
Typical project: wood and agricultural residue pellet production.
Raw material: mixed wood waste and agricultural residues in controlled mix ratio.
Configuration: ring die pellet making machine with hammer mill, dryer, cooler, screener, and packing.
Application: industrial fuel pellets and local fuel market supply.
Acceptance: trial run with actual material, output and pellet quality recorded before shipment.
The parameters above are typical ranges and should be confirmed with actual test records.
Procurement Checklist
Before signing a contract, confirm the following with the supplier:
Capacity with stated feedstock, moisture, particle size, and pellet diameter.
Die compression ratio and die material.
Die hole diameter and pellet diameter.
Roller shell material and hardness.
Drive system, gearbox or belt drive.
Feeder type and whether variable frequency control is included.
Grinding, conditioning, and drying scope.
Cooling, screening, and packing scope.
Dust collection and explosion protection scope, including reference to applicable NFPA or local standards where relevant.
Motor power, total connected load, voltage, phase, and frequency.
Spare parts list with part numbers and recommended first order.
Warranty scope, wear part definition, and response process.
Inspection and acceptance method before shipment.
Frequently Asked Questions
What is a pellet making machine?
A pellet making machine compresses ground material into dense cylindrical pellets using pressure and friction heat. It is the core machine in a pellet production line.
What is the difference between a flat die and ring die pellet making machine?
Flat die machines are simpler, lower in cost, and easier to maintain, and suit small production and varied materials. Ring die machines are more efficient at higher capacity and produce denser pellets, and suit commercial and industrial production.
What materials can a pellet making machine process?
Wood, sawdust, wood shavings, wood chips after grinding, agricultural residues, animal feed materials, palm fiber, EFB, coffee husk, peanut shell, cotton stalk, coconut husk, and rice husk can be pelletized with appropriate configuration.
What moisture is suitable for pelletizing?
Typical target moisture before pelletizing is around 10 to 15 percent for most wood and biomass feedstocks, and around 12 to 14 percent for many feed formulations. The exact range depends on feedstock and die specification, and should be confirmed with a pelletizing test.
Do I need a dryer for pellet production?
Drying is required when feedstock moisture is above the suitable range for pelletizing. Dry sawdust may not need a dryer. Wet wood chips, green wood, and high-moisture agricultural residues usually do.
How is pellet making machine capacity calculated?
Required hourly capacity equals annual production target divided by annual operating hours, plus a capacity margin of about 20 to 30 percent. Actual capacity depends on feedstock, moisture, particle size, and die specification.
How much does a pellet making machine cost?
Cost depends on machine type, capacity, motor power, die specification, drive system, automation, and scope of supply. A small flat die machine, a medium ring die machine, and a complete industrial line are in clearly different price categories. Final cost should be confirmed against a written scope of supply.
How long do dies and rollers last?
Die and roller life depends on feedstock abrasiveness, moisture, compression ratio, and operating conditions. Expected working hours should be confirmed with the supplier based on similar material, not assumed from a general figure.