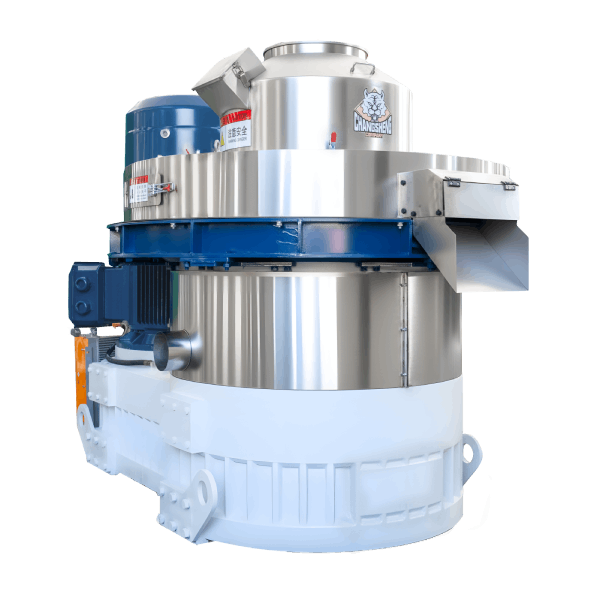
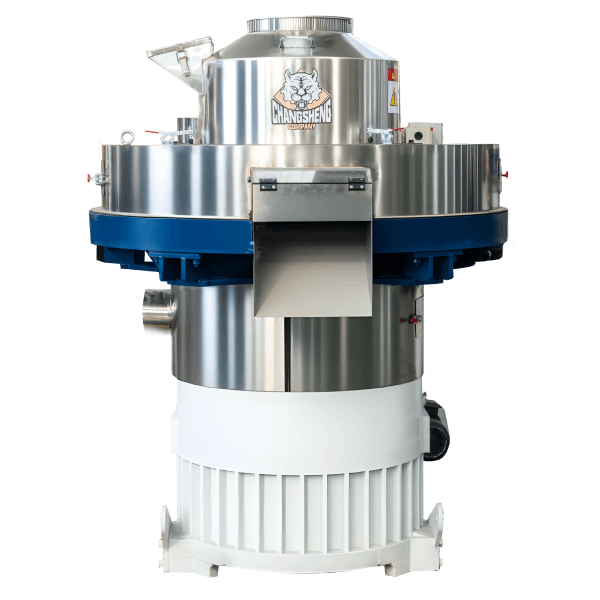
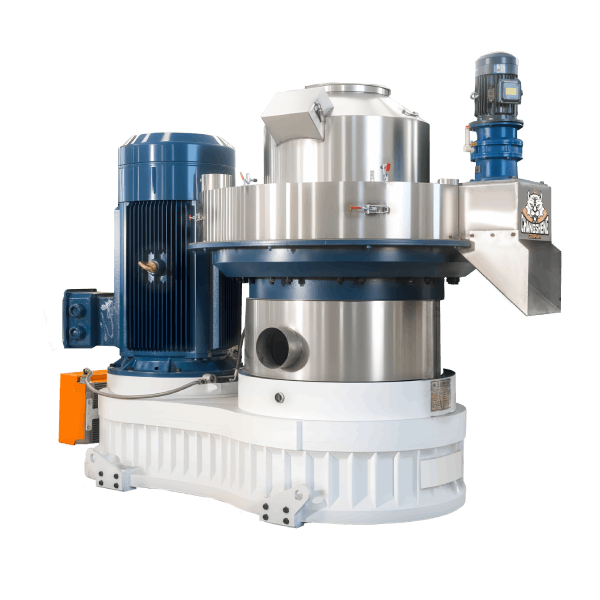
Ring Die Pellet Machine: Types, Working Principle, Die Selection and Procurement
News 2026-10-02
A ring die pellet machine is not a single product. It is a family of machines that differ in die structure, drive system, roller configuration, and automation level. Two machines with the same nominal capacity can differ in die life, pellet quality, energy consumption, and maintenance cost. The correct choice depends on the feedstock, the operating hours, the target pellet quality, and the maintenance capability at the site.
The practical question for a buyer is not which machine is the most powerful. The real question is which ring die configuration fits the feedstock and the operating pattern, and what must be confirmed with the supplier before ordering.
This guide explains ring die machine types, how a ring die machine works, how to choose die compression ratio and drive system, how capacity is stated and verified, and what to confirm before signing a contract. For feedstock-specific guidance such as hardwood, palm fiber, coffee husk, or rice husk, see the separate material pages on this site. For general pellet mill selection, see the pellet mill guide on this site.
Ring Die Pellet Machine Types
Ring die pellet machines differ in die structure, drive system, and roller configuration. These differences affect capacity, die life, maintenance, and cost.
Single-Layer Ring Die Machine
A single-layer die uses one ring die with one set of die holes. It is simpler and lower in cost than a double-layer design. It suits single-feedstock production and moderate capacity.
Double-Layer Ring Die Machine
A double-layer die allows two compression zones or two pellet specifications in one die body. It suits projects that need to switch between two pellet specifications or that need a longer service interval between die replacements. The trade-off is higher die cost and more complex die management.
Gearbox Drive Ring Die Machine
A gearbox drive uses a gear transmission between the motor and the main shaft. It provides higher torque transmission efficiency and better stability under continuous load. It is common in industrial ring die machines. Maintenance requires oil change, oil analysis, and gear inspection according to the supplier schedule.
Belt Drive Ring Die Machine
A belt drive uses belts to transmit power from the motor to the main shaft. It is simpler, lower in cost, and easier to maintain in locations without specialized service. Belt tension and alignment must be checked regularly, and belts must be replaced at planned intervals. Belt drive may be less suitable at higher capacity because of higher torque demand.
Single Roller, Double Roller, and Three Roller Configuration
A ring die machine may use one, two, or three rollers to press material into the die. More rollers provide more compression points and can improve output stability, but also increase maintenance complexity.
Roller configuration also affects feed distribution inside the die chamber. With multiple rollers, material must be distributed evenly between the rollers. If one roller receives more material than another, that roller wears faster and the die wears unevenly. Die and roller alignment, feeder position, and die speed all affect how evenly material is distributed across the rollers. Roller configuration should be matched to die size, feedstock, and target capacity, and should be confirmed with the supplier based on the actual feedstock.
How a Ring Die Pellet Machine Works
Material enters the die chamber through a feeder. Rollers press the material into the die holes. Friction between material and die generates heat, which softens natural binders such as lignin. The softened material binds particles together as it passes through the die. Pellets exit the die and are cut to length by the cutter.
Each step affects pellet quality and machine load. Feed rate affects stability. Die compression ratio affects density and power demand. Roller clearance affects compression and wear. Moisture affects binding and blockage risk.
Main Components
Die: the vertical ring that shapes pellets and determines compression ratio.
Rollers: press material into the die holes; roller pressure and clearance affect compression and wear.
Main shaft: transmits torque to the die or roller assembly.
Gearbox or belt drive: transmits torque from motor to main shaft.
Motor: powers the machine; motor power must match capacity and material density.
Feeder: controls material input; variable frequency feeding improves stability.
Conditioner: adds heat and moisture when needed; improves binding for dry or low-lignin materials.
Cutter: trims pellets to length.
Lubrication system: reduces wear and supports continuous operation.
Die Compression Ratio and Die Selection
Die compression ratio is the ratio of die hole length to die hole diameter. This is the common definition used in this guide. Some suppliers use effective length or taper-based definitions, so the definition should always be confirmed with the supplier before comparing dies.
Higher compression ratio increases pellet density but also increases power demand and die wear. Lower compression ratio reduces density and may cause soft pellets.
The correct compression ratio depends on material density, fiber content, and moisture. Softwood and other low-density materials usually require a lower compression ratio to avoid overloading the motor. Hardwood and other high-density materials usually require a higher compression ratio to reach target pellet durability. Fibrous and low-lignin materials such as straw and rice husk often require a higher compression ratio than wood, and may also require a wear-resistant die because of silica content.
Die selection should be confirmed with a pelletizing test using the actual feedstock. Die life varies widely by feedstock, so expected working hours should be confirmed with the supplier based on similar material and operating conditions, not assumed from a general figure.
Die Hole Diameter and Pellet Diameter
Die hole diameter determines pellet diameter. Common pellet diameters are 2 to 4 mm for small feed, 4 to 6 mm for poultry and cattle feed, and 6 to 8 mm for biomass fuel, with 10 mm and 12 mm available for some industrial applications.
Pellet diameter should be selected against the boiler, stove, or feed system, not chosen independently. A pellet that is too small may pass through the feed system too quickly; a pellet that is too large may not feed correctly. Die hole diameter and pellet diameter should be confirmed together with the supplier before ordering.
Die Temperature and Operating Control
Die temperature is the friction-generated temperature inside the die chamber during pelletizing. It affects lignin softening, binding, and pellet durability.
If die temperature is too low, lignin does not soften enough and pellets are weak. If die temperature is too high, material may scorch, die wear accelerates, and fire risk increases. Die temperature depends on feedstock type, moisture, compression ratio, and feed rate.
A ring die machine should include a die temperature sensor and alarm. Feed rate should be adjusted to keep temperature within the target range. The target range depends on feedstock and should be confirmed with a pelletizing test. For commercial lines, an automatic feed rate adjustment linked to die temperature is recommended.
Roller Clearance and Roller Adjustment
Roller clearance is the gap between the roller and the die surface. It affects compression, pellet quality, and wear on both roller and die.
If roller clearance is too large, material slips and output drops. If clearance is too small, rollers and die wear faster, and motor load rises. Roller clearance should be adjusted according to the supplier procedure and checked regularly.
As a practical reference, roller clearance for ring die machines is usually set within a narrow range that balances compression and wear, and the exact value depends on die size, roller size, feedstock, and machine design. The correct clearance should be confirmed with the supplier during commissioning and recorded as a baseline for future adjustment.
Ring Die vs Flat Die Pellet Machine
Factor: Production scale
Ring Die: Medium to large
Flat Die: Small to medium
Factor: Continuous operation
Ring Die: Suitable
Flat Die: More limited
Factor: Initial investment
Ring Die: Higher
Flat Die: Lower
Factor: Die structure
Ring Die: Vertical ring
Flat Die: Flat plate
Factor: Die surface area
Ring Die: Larger, higher throughput
Flat Die: Smaller, lower throughput
Factor: Drive system
Ring Die: Gearbox or belt drive
Flat Die: Simpler drive
Factor: Maintenance
Ring Die: More specialized
Flat Die: Simpler
Factor: Die change
Ring Die: May need lifting equipment
Flat Die: Easier, basic tools
Factor: Energy consumption
Ring Die: Lower per ton at scale
Flat Die: Higher per ton
Factor: Typical use
Ring Die: Commercial and industrial production
Flat Die: Small production and varied materials
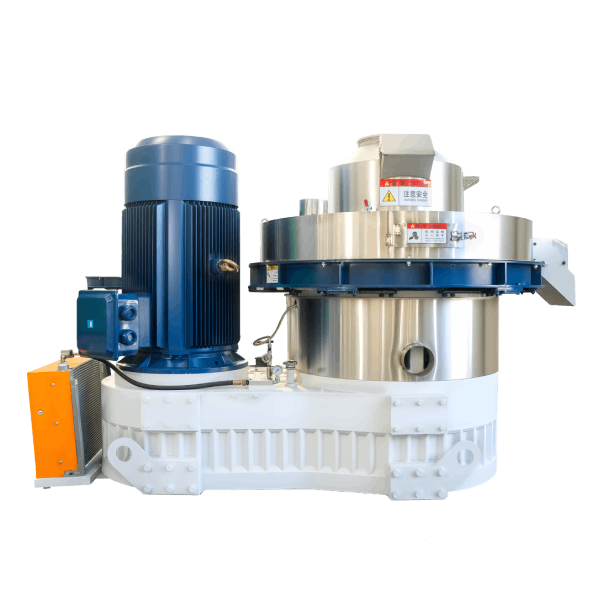
Ring Die Pellet Machine Technical Specifications
Specification: Capacity
Why It Matters: Determines production output; only meaningful with feedstock, moisture, and die conditions
Specification: Motor power
Why It Matters: Determines drive configuration; depends on capacity, material density, voltage, frequency, altitude, ambient temperature
Specification: Die diameter
Why It Matters: Affects production configuration
Specification: Die type
Why It Matters: Single-layer or double-layer; affects die cost and management
Specification: Die hole diameter
Why It Matters: Determines pellet diameter
Specification: Compression ratio
Why It Matters: Affects pellet density and die wear; depends on material density, fiber, and moisture
Specification: Roller configuration
Why It Matters: Single, double, or three rollers; affects compression and output stability
Specification: Drive system
Why It Matters: Gearbox or belt drive; affects efficiency, maintenance, and cost
Specification: Feed rate control
Why It Matters: Controls production stability; variable frequency recommended
Specification: Machine dimensions
Why It Matters: Installation planning
Specification: Weight
Why It Matters: Transport and foundation
Specification: Power supply
Why It Matters: Overseas installation and compatibility
Actual values should be confirmed in a written technical agreement, not estimated from catalog images.
Common Problems in Ring Die Pellet Machine Operation
Blockage
Blockage is usually caused by moisture too high, feed rate too fast, particle size too fine, or compression ratio mismatch. Check moisture, feed rate, and die selection before adjusting the machine.
Poor Pellet Formation
Poor formation is usually caused by wrong compression ratio, low moisture, low die temperature, or worn die and rollers. Review die selection, moisture, die temperature, and roller condition.
High Energy Consumption
High energy consumption is usually caused by die and roller mismatch, overload feed rate, worn die, or unstable power supply. Review die specification, feed rate, and motor load.
Short Die and Roller Life
Short die and roller life is usually caused by abrasive material, mineral contamination, wrong compression ratio, or incorrect roller clearance. Review material preparation, die material, and clearance adjustment.
Unstable Feed
Unstable feed is usually caused by variable moisture, variable particle size, feeder design, or material bridging. Review drying, grinding, and feeder configuration.
Gearbox or Belt Drive Problems
Gearbox problems may include oil contamination, oil level issues, or gear wear. Belt drive problems may include tension loss, misalignment, or belt wear. Both should be checked according to the supplier schedule. Gearbox drive generally has higher efficiency and lower maintenance frequency at higher capacity, but higher initial cost and more specialized service. Belt drive is simpler and cheaper to maintain, but belts must be replaced at planned intervals and belt drive may be less suitable at higher capacity.
Ring Die Pellet Machine Maintenance
Dies and rollers are wear parts. Their life depends on material abrasiveness, moisture, compression ratio, and operating conditions. Die life varies widely by material, so expected working hours should be confirmed with the supplier based on similar material and operating conditions, not assumed from a general figure.
Daily checks include lubrication, roller clearance, feeder condition, and motor current.
Weekly checks include die and roller wear, belt tension, and electrical connections.
Monthly checks include lubrication system condition, bearing temperature, gearbox oil condition, and control panel inspection.
Seasonal checks include spare parts stock review, die replacement planning, gearbox oil change, and electrical insulation check.
Keeping a maintenance log helps track die hours, power consumption, and output, and supports planned replacement instead of unplanned downtime.
Die Change Frequency and Downtime Cost
Die change frequency depends on feedstock abrasiveness, moisture, compression ratio, and operating conditions. For abrasive feedstocks, die change is more frequent than for clean wood. Each die change requires production stop, die removal, roller inspection, die installation, clearance adjustment, and first production stabilization.
Downtime cost depends on production rate, labor cost, and the value of lost output. A project without a spare die on site will face long downtime when the first die wears out. A practical plan includes a spare die and roller set on site, a planned maintenance window, and a maintenance log to track die hours.
Pellet Durability and Fines Control
Pellet durability and fines content are key indicators for biofuel pellets. Durability depends on lignin content, compression ratio, die temperature, moisture, and cooling. Fines are produced when pellets are weak, when cooling is insufficient, or when screening is inadequate.
To control durability and fines, the line should maintain correct moisture, use a die with the correct compression ratio, keep die temperature within the target range, and provide adequate cooling and screening. Durability and fines should be measured as part of the acceptance test, not assumed from general figures.
Pellet Quality and Standards
For export or higher-grade markets, pellet quality may need to meet standards such as ISO 17225 for solid biofuels. Key quality parameters include moisture, ash content, durability, fines, and pellet diameter. Ash content depends on feedstock and bark content. Durability depends on lignin content, compression ratio, die temperature, and cooling.
Exact grade limits should be confirmed against the current official standard, not assumed from a general figure. Certification requires testing and documentation that go beyond the pellet machine itself.
Packing and Shipping Considerations
Ring die pellet machines are large, heavy equipment. Packing must protect against moisture and mechanical damage during sea transport. Frame container loading, reinforced crating, and moisture barrier film are common. The largest single piece should be identified before shipment so that lifting equipment at the destination can be planned.
Shipping marks, case numbers, weight, and dimensions should match the packing list. Installation tools and special fixtures should be included. For overseas projects, documentation should include operation manual, electrical diagram, foundation drawing, and spare parts list. All shipping and packing requirements should be confirmed with the supplier and the freight forwarder before shipment.
Ring Die Pellet Machine Cost and What Determines It
Ring die pellet machine price is determined by machine type, capacity, motor power, die size and material, die type (single-layer or double-layer), roller configuration, drive system (gearbox or belt), automation level, material compatibility, spare parts included, and auxiliary equipment scope.
A small ring die machine and a large ring die machine are in different price categories. A belt drive machine and a gearbox drive machine are also in different price categories. A machine for feed materials and a machine for abrasive biomass may differ in price because of die and roller specification.
Machine price is not the same as complete pellet production line cost. A complete line may include a crusher or hammer mill, dryer, pellet mill, cooler, screener, packing machine, and dust collection. Final cost should be confirmed against a written scope of supply.
Do You Need a Ring Die Pellet Machine or a Flat Die Pellet Machine?
A flat die machine may be sufficient when production is small, material is varied, or budget is limited. A ring die machine is usually needed when production is medium to large, operation is continuous, pellet quality must be consistent, or the project requires automation and planned maintenance.
Decide based on material condition, required capacity, operating hours, and target pellet quality, not on price alone.
Procurement Checklist
Requirements: material type, moisture, particle size, target capacity, pellet diameter, power supply, operating hours, automation level.
Machine: die type, die diameter, die hole diameter, compression ratio, motor power, roller configuration, drive system, feeder type, lubrication, control mode.
Technical agreement: capacity with conditions, voltage, phase, frequency, control voltage, protection class, insulation class.
Spare parts: die, roller, bearings, belts or gearbox spare parts, seals, with part numbers and recommended stock.
Supplier: factory capability, export experience, reference projects with similar material, test run, inspection terms, warranty process.
Frequently Asked Questions
What is a ring die pellet machine?
A ring die pellet machine is a pellet mill that uses a vertical ring-shaped die to form pellets. Material is pressed through die holes by rollers, heated by friction, and cut to length.
What are the main types of ring die pellet machines?
Main types include single-layer and double-layer ring dies, gearbox drive and belt drive, and single-roller, double-roller, and three-roller configurations. The correct type depends on capacity, material, and operating hours.
What is the difference between a ring die and flat die pellet machine?
Ring die machines suit medium to large capacity and continuous operation, and use a vertical ring die with larger die surface area. Flat die machines suit small to medium capacity and varied materials, and use a flat plate die with simpler maintenance.
How do I choose between a ring die and flat die pellet machine?
Consider production scale, required capacity, operating hours, material consistency, pellet quality requirement, maintenance capability, and budget.
How is ring die pellet machine capacity calculated?
Required hourly capacity equals annual production target divided by annual operating hours, plus a capacity margin of about 20 to 30 percent. Actual capacity depends on material, moisture, particle size, die specification, and machine configuration.
What determines ring die pellet machine output?
Output depends on material type, moisture, particle size, pellet diameter, die specification, compression ratio, machine efficiency, and operating skill.
How do I choose the correct die?
Die selection depends on material density, fiber content, moisture, and target pellet quality. A pelletizing test with your actual material is the most reliable method.
What motor power does a ring die pellet machine need?
Motor power depends on capacity, material density, voltage, frequency, altitude, and ambient temperature. A written technical agreement should state main motor power and total connected load.
How much does a ring die pellet machine cost?
Price depends on type, capacity, motor power, die specification, die type, drive system, automation, and scope of supply. A small ring die machine, a medium ring die machine, and a complete industrial line are in clearly different price categories. Final price should be confirmed against a written scope of supply.
How often do dies and rollers need maintenance?
Die and roller life depends on material abrasiveness, moisture, and operating conditions. Die life varies widely by material, so expected working hours should be confirmed with the supplier based on similar material, not assumed from a general figure.
Do I need a complete production line?
It depends on material condition, target pellet quality, and sales channel. Dry and uniform material may only need a pellet mill and cooler. Wet, coarse, or mixed material usually requires a complete line.