Machine to Make Wood Pellets: How to Choose the Right System for Your Wood Feedstock
News 2026-10-07
A machine to make wood pellets is not a single product. It is a system that includes a pellet mill, and usually a combination of grinding, drying, cooling, screening, and packing equipment. The machine itself is only one part of the process. What determines output, pellet quality, and die life is how the whole system is matched to your wood feedstock.
The practical question for a buyer is not which machine is the cheapest. The real question is which configuration fits your wood species, moisture, particle size, target pellet quality, power supply, and operating pattern, and what must be confirmed before ordering.
This guide explains how a machine to make wood pellets works, how wood feedstock affects machine selection, how to choose between flat die and ring die, how capacity is stated, what auxiliary equipment is required, and what to confirm with the supplier before purchase. For wood-specific pricing, see the wood pellet making machine price page on this site. For general pellet making machine selection, see the pellet making machine page on this site.
Wood Pellet Machine, Wood Pellet Mill and Wood Pellet Press
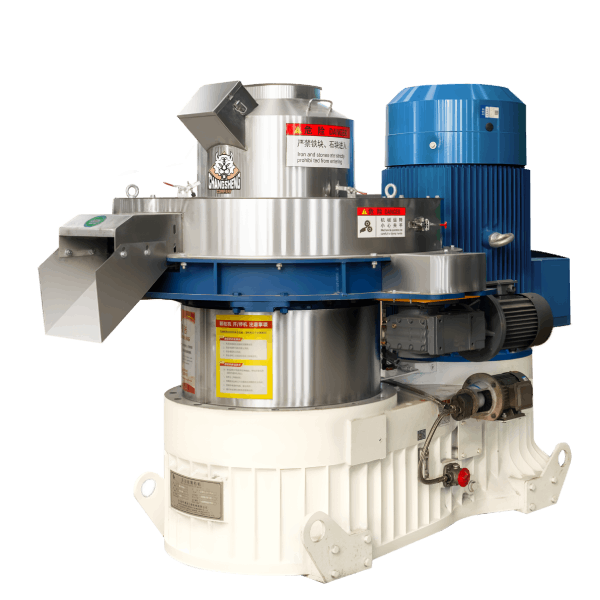
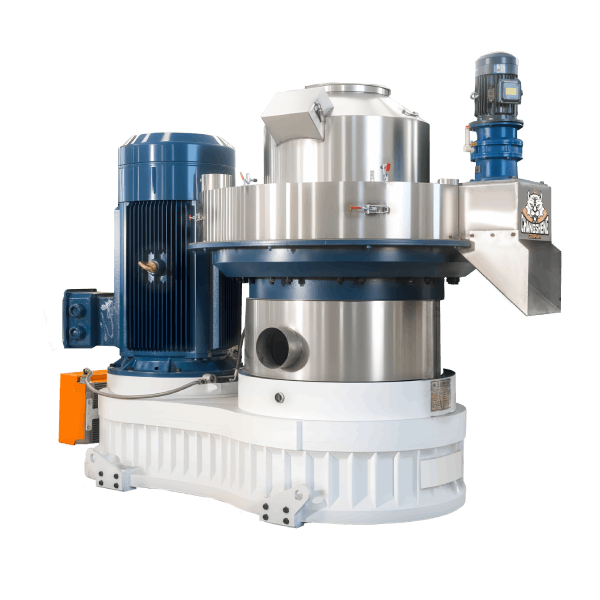
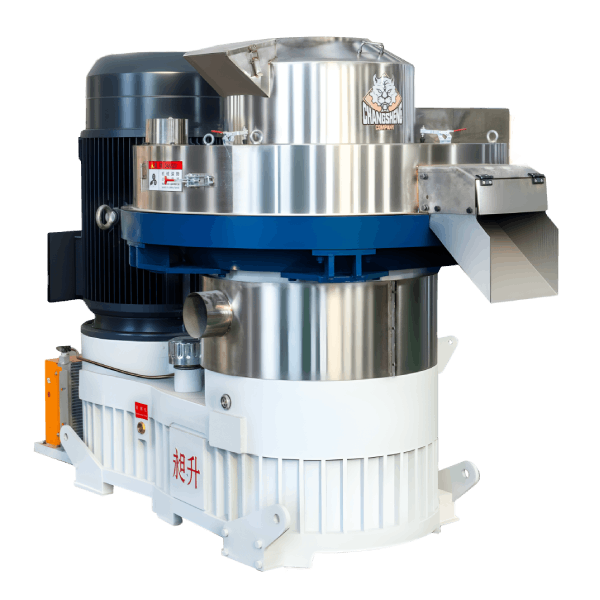
These three terms are often used interchangeably, but in engineering usage they differ slightly. A wood pellet machine usually refers to the core compression machine. A wood pellet mill usually refers to the same machine, and in some markets it also refers to the whole production line. A wood pellet press is a term more common in Europe and North America, and it usually emphasizes the pressing function of the die and roller assembly.
In this guide, machine to make wood pellets is used to describe both the core machine and the surrounding system, because that is how buyers typically use the term in procurement.
What a Machine to Make Wood Pellets Actually Includes
A complete wood pellet system usually includes:
A chipper or crusher for large wood pieces.
A hammer mill for grinding to consistent particle size.
A dryer for reducing moisture when it is above the suitable range.
A pellet mill for forming pellets.
A cooler for hardening pellets and reducing fines.
A screener for removing fines and oversize.
A packing machine for bagging or bulk loading.
Dust collection for health and explosion protection.
Not every project needs every piece. A project using dry sawdust may need only a pellet mill, cooler, and screener. A project using wet wood chips may need a complete line with chipping, grinding, and drying. The correct scope depends on feedstock and target pellet quality, not on a fixed template.
How a Wood Pellet Machine Works
Wood material is fed into the die chamber, pressed through die holes by rollers, heated by friction, and bound by natural binders such as lignin. Pellets exit the die and are cut to length, then cooled and screened.
The working principle is the same for flat die and ring die machines. What makes wood pellet production different is the raw material preparation, especially moisture control, grinding, and die selection.
Flat Die vs Ring Die for Wood Pellets
Factor: Production scale
Flat Die: Small
Ring Die: Medium to large
Factor: Initial investment
Flat Die: Lower
Ring Die: Higher
Factor: Continuous operation
Flat Die: Limited
Ring Die: Suitable
Factor: Die structure
Flat Die: Flat plate
Ring Die: Vertical ring
Factor: Maintenance
Flat Die: Simpler
Ring Die: More specialized
Factor: Die change
Flat Die: Easier, basic tools
Ring Die: May need lifting equipment
Factor: Typical use
Flat Die: Small farm or workshop
Ring Die: Commercial and industrial production
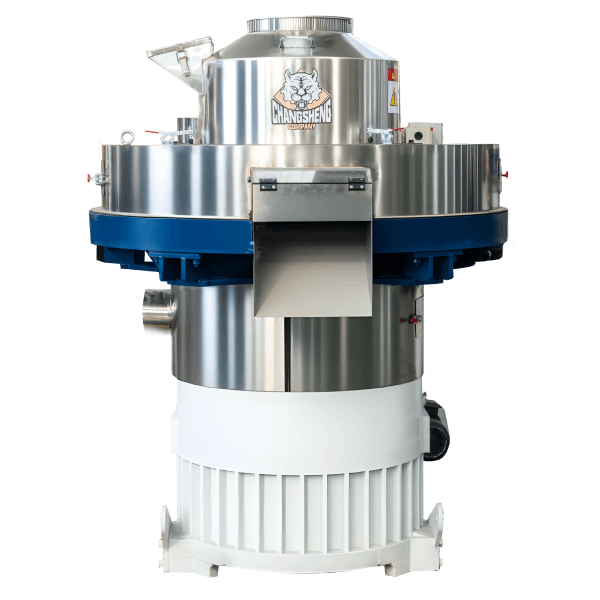
A flat die machine is often the better choice for small farms, workshops, and pilot projects with varied feedstock or intermittent operation. A ring die machine is often the better choice for commercial production, continuous operation, and consistent pellet quality.
How Wood Feedstock Affects Machine Selection
Sawdust
Sawdust is usually the easiest wood feedstock to pelletize. Particle size is often already suitable, and the main requirement is moisture control. If sawdust is dry and consistent, a pellet mill with a cooler and screener may be enough.
Wood Shavings
Wood shavings are longer and bulkier than sawdust. They require grinding before pelletizing. If shavings are not ground to a consistent size, feeding becomes uneven and pellet quality varies.
Wood Chips
Wood chips require chipping and grinding before pelletizing. Moisture is often high, so drying may be required. Chips from fresh timber are usually wetter than chips from dry wood.
Hardwood
Hardwood is denser and more abrasive than softwood. It requires more compression force, more motor power, and a die with higher wear resistance. Hardwood also often has lower lignin content, which may require a higher compression ratio to reach the same pellet durability.
Softwood
Softwood is generally easier to pelletize because of higher lignin content. Pine, fir, and spruce produce strong pellets. Softwood is often the preferred feedstock for premium wood pellet production.
Mixed Wood Waste
Mixed wood waste may include sawdust, shavings, chips, bark, and sanding dust. Mix ratio should be consistent. Variable mix causes variable compression, feeding, and pellet quality. Preprocessing requirements are higher for mixed wood waste.
Moisture and Particle Size
Typical target moisture before pelletizing is around 10 to 15 percent for most wood feedstocks, depending on species, die compression ratio, and machine configuration. The exact target should be confirmed with a pelletizing test.
If moisture is too high, compression is poor, the die may block, and throughput drops. If moisture is too low, binding is poor, pellets are weak, and fines increase.
Particle size affects feeding stability, compression, pellet density, and die wear. Target particle size is usually in the range of 2 to 5 mm, depending on die specification. If feedstock is too coarse, grinding is required. If too fine, bridging and die blockage risk increases.
Die Compression Ratio and Die Selection
Die compression ratio is the ratio of die hole length to die hole diameter. It determines how much resistance the material meets as it passes through the die. Higher compression ratio increases pellet density but also increases power demand and die wear.
The correct compression ratio depends on wood species, moisture, and target pellet quality. Softwood and low-density materials usually require a lower compression ratio. Hardwood and high-density materials usually require a higher compression ratio to reach target pellet durability. Die selection should be confirmed with a pelletizing test using the actual wood feedstock.
The definition of compression ratio can vary between suppliers, so it should always be confirmed before comparing dies. Die life varies widely by feedstock, so expected working hours should be confirmed with the supplier based on similar material and operating conditions, not assumed from a general figure.
Feed Pellets vs Fuel Pellets from Wood Feedstock
A machine to make wood pellets may be configured for two different applications: feed pellets and fuel pellets. The configuration is not the same.
For fuel pellets, the process relies mainly on lignin and friction heat. Die compression ratio is usually higher, and durability and fines are the key quality parameters. Ash content matters for boiler compatibility, and bark content should be controlled.
For feed pellets, steam conditioning is commonly used before pelletizing to raise temperature and moisture, which improves protein and starch binding. Die compression ratio is usually lower than for fuel pellets. Moisture recovery after cooling is often used to bring pellets to the target moisture. Durability is usually measured by a pellet durability index test.
Some wood-based materials are used for animal bedding rather than fuel or feed. Bedding pellets usually require low dust, moderate hardness, and low fines. Configuration for bedding pellets is different again.
Die Temperature, Conditioning and Roller Clearance
Die temperature is the friction-generated temperature inside the die chamber. It affects lignin or protein binding and pellet durability. If temperature is too low, pellets are weak. If temperature is too high, material may scorch and die wear accelerates.
For fuel pellets, die temperature is usually generated by friction, and feed rate is adjusted to keep temperature within the target range. For feed pellets, steam conditioning is used to raise temperature and moisture before pelletizing. In both cases, a die temperature sensor and alarm are recommended.
Roller clearance is the gap between the roller and the die surface. If clearance is too large, material slips and output drops. If clearance is too small, rollers and die wear faster and motor load rises. Roller clearance should be set according to the supplier procedure and checked regularly.
Capacity and How It Is Stated
Wood pellet machines typically range from about 30 kg/h for small flat die machines to several tons per hour for industrial ring die machines. Capacity is not a fixed number. It depends on wood species, moisture, particle size, pellet diameter, die specification, compression ratio, motor power, feed rate, and operating skill.
Rated capacity is only meaningful when feedstock, moisture, particle size, and die specification are stated. A capacity figure quoted without these conditions should not be treated as a guaranteed output for your project.
Required hourly capacity equals annual production target divided by annual operating hours. A capacity margin of about 20 to 30 percent is a practical starting point for feedstock variation, moisture changes, and maintenance. The exact margin depends on feedstock consistency, operating hours, and maintenance planning.
Auxiliary Equipment and Line Configuration
A wood pellet line may be configured as a small system, a medium line, or an industrial line.
A small system usually includes a hammer mill, pellet mill, and cooler. Drying may be done separately or by natural drying. This configuration suits small farms, pilot projects, and dry, uniform material.
A medium line usually includes a crusher or hammer mill, dryer, pellet mill, cooler, screener, and packing machine. This configuration suits small commercial production and cooperatives.
An industrial line includes full material receiving, crushing, grinding, drying, conditioning, pelletizing, cooling, screening, packing, and dust collection. Automation and control systems are usually included. This configuration suits commercial fuel production and export-oriented plants.
A wood pellet line may also be supplied in containerized or mobile configuration. A containerized line is built into one or more shipping containers and is used for export projects, remote sites, or projects where site construction is limited. A mobile unit is mounted on a trailer or truck frame and is used where feedstock is scattered or where production is seasonal. These configurations are useful in remote locations such as islands, mountain sites, and off-grid farms.
Energy Consumption and Operating Cost
Energy consumption per ton depends on wood species, moisture, particle size, die specification, compression ratio, feed rate, and motor efficiency. Hardwood and high-moisture feedstock usually require more energy per ton than dry softwood. Energy consumption should be confirmed with the supplier at your actual feedstock condition, not assumed from a catalog figure.
Operating cost includes raw material, power, labor, maintenance, spare parts, and downtime. Cost per ton of pellets is the figure that matters, not machine price alone. Die change frequency and downtime cost also affect cost per ton: a project without a spare die on site will face long downtime when the first die wears out, even if the die price itself was low.
Wood Pellet Quality
For local use, pellet quality requirements are usually set by the boiler or stove. For export or higher-grade markets, pellet quality may need to meet standards such as ISO 17225 for solid biofuels. Some markets also use certification schemes such as ENplus, and some North American markets use PFI specifications. Key quality parameters include moisture, ash content, durability, fines, and pellet diameter.
Durability depends on lignin content, compression ratio, die temperature, and cooling. Fines are produced when pellets are weak, when cooling is insufficient, or when screening is inadequate. Ash content depends on wood species and bark content. Higher-grade pellets usually require lower ash content, which means cleaner feedstock, tighter process control, and better cooling and screening. These requirements often increase equipment cost and operating cost. Exact grade limits should be confirmed against the current official standard, not assumed from a general figure.
Maintenance and Spare Parts
Dies and rollers are wear parts. Their life depends on wood abrasiveness, moisture, bark content, compression ratio, and operating conditions. For hardwood and bark-containing feedstocks, die and roller life may be shorter than for clean softwood.
A practical spare parts plan includes at least one spare die, one or two spare roller shell sets, bearings, belts, seals, lubricants, and critical electrical spares.
Daily checks include lubrication, roller clearance, feeder condition, and motor current. Weekly checks include die and roller wear, belt tension, and electrical connections. Monthly checks include lubrication system condition, bearing temperature, and control panel inspection.
What Determines Machine Cost
Cost depends on machine type, capacity, motor power, die size and material, roller configuration, drive system, automation level, material compatibility, spare parts included, and auxiliary equipment scope.
Machine price is not the same as complete line cost. A complete line may include chipper, hammer mill, dryer, pellet mill, cooler, screener, packing machine, and dust collection. Final cost should be confirmed against a written scope of supply.
Destination Country Compliance and Documentation
For export projects, destination country compliance may apply. This can include certification, labeling, electrical standards, and documentation. Electrical standards such as voltage, phase, and frequency must match the destination country. Documentation typically includes commercial invoice, packing list, bill of lading, certificate of origin, and user manual in the destination language where required. Additional certification may be required by the destination country. All compliance and documentation requirements should be confirmed with the supplier and with the import agent in the destination country before shipment.
Typical Project Scenario
The following summarizes typical project parameters from wood pellet machine projects. Specific customer names, locations, and contact details are not included.
Typical project: softwood sawmill pellet production.
Raw material: softwood sawdust from pine, fir, and spruce.
Moisture: reduced by drying to the range suitable for pelletizing.
Pellet diameter: 6 to 8 mm.
Configuration: ring die pellet machine with hammer mill, dryer, cooler, screener, and packing.
Application: industrial fuel pellets and local fuel market supply.
Acceptance: trial run with actual sawdust, output and pellet quality recorded before shipment.
The parameters above are typical ranges and should be confirmed with actual test records.
Procurement Checklist
Before signing a contract, confirm the following with the supplier:
Capacity with stated wood species, moisture, particle size, and pellet diameter.
Die compression ratio and die material.
Die hole diameter and pellet diameter.
Roller shell material and hardness.
Drive system, gearbox or belt drive.
Feeder type and whether variable frequency control is included.
Grinding and drying scope, including hammer mill screen size and dryer capacity.
Cooling, screening, and packing scope.
Dust collection and explosion protection scope, including reference to applicable NFPA or local standards where relevant.
Motor power, total connected load, voltage, phase, and frequency.
Spare parts list with part numbers and recommended first order.
Warranty scope, wear part definition, and response process.
Inspection and acceptance method before shipment.
Frequently Asked Questions
What machine is used to make wood pellets?
A wood pellet machine is the core of the process. A complete system usually includes a chipper or crusher, hammer mill, dryer, pellet mill, cooler, screener, and packing machine, depending on feedstock and target pellet quality.
What is the difference between a flat die and ring die wood pellet machine?
Flat die machines are simpler, lower in cost, and easier to maintain, and suit small production and varied materials. Ring die machines are more efficient at higher capacity and produce denser pellets, and suit commercial and industrial production.
What wood feedstocks can be pelletized?
Sawdust, wood shavings, wood chips after grinding, hardwood, softwood, and mixed wood waste can be pelletized. Treated, painted, or contaminated wood should be avoided.
What moisture is suitable for wood pelletizing?
Typical target moisture before pelletizing is around 10 to 15 percent, depending on wood species, die compression ratio, and machine configuration. The exact target should be confirmed with a pelletizing test.
Do I need a dryer to make wood pellets?
Drying is required when wood moisture is above the suitable range for pelletizing. Dry sawdust may not need a dryer. Wet wood chips or green wood usually do.
How much capacity do I need?
Required hourly capacity equals annual production target divided by annual operating hours, plus a capacity margin of about 20 to 30 percent. Actual capacity depends on wood species, moisture, particle size, and die specification.
How much does a machine to make wood pellets cost?
Cost depends on machine type, capacity, motor power, die specification, drive system, automation, and scope of supply. A small flat die machine, a medium ring die machine, and a complete industrial line are in clearly different price categories. Final cost should be confirmed against a written scope of supply.
How long do dies and rollers last?
Die and roller life depends on wood abrasiveness, moisture, bark content, compression ratio, and operating conditions. Expected working hours should be confirmed with the supplier based on similar material, not assumed from a general figure.