Page SEO Summary: This troubleshooting guide helps pellet mill operators diagnose and solve capacity drop problems—covering causes, immediate solutions, component inspection, and prevention strategies.
A pellet machine that once produced 1 ton per hour is now producing only 700 kg per hour. Production targets are missed. Operating costs are rising. The machine seems to be running, but something is wrong.
Capacity drop is one of the most common—and most frustrating—problems in pellet production. It can be caused by die wear, roller wear, material changes, operational issues, or a combination of factors. This guide provides a systematic approach to diagnosing and solving capacity drop.
Quick Diagnosis: Where to Start
The Diagnostic Flow
Step
Check
What It Tells You
1
Amperage
Is the motor drawing normal current?
2
Die condition
Are die holes worn or clogged?
3
Roller condition
Are rollers worn or misadjusted?
4
Material moisture
Is moisture content optimal?
5
Particle size
Is grind consistent?
6
Feed rate
Is feed rate consistent?
7
Temperature
Is conditioning optimal?
Amperage Check
Amperage Reading
What It Means
Action
Normal
Motor drawing normal current
Check other factors
Low
Motor not loaded—feed issue or die issue
Check feed, die
High
Motor overloaded—feed too high or die clogged
Reduce feed, inspect die
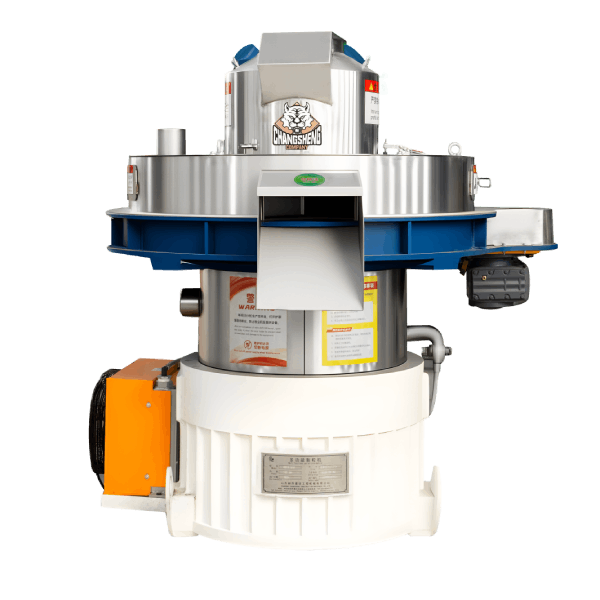
A pellet machine capacity drop from a manufacturer like Shandong Changsheng Machinery Co., Ltd. can be diagnosed systematically—starting with amperage, then working through the components.
Common Causes of Capacity Drop
1. Die Wear
Symptom
What It Means
Solution
Enlarged holes
Die is worn; material passes too easily
Replace die
Uneven hole wear
Roller gap incorrect
Adjust gap, replace die
Clogged holes
Material blocking die
Clean die
Cracked die
Structural damage
Replace die
Die Wear Impact: As die holes enlarge, material passes through with less compression. The machine produces pellets, but at lower density and lower throughput. Die wear is a normal consumable—but it directly reduces capacity.
2. Roller Wear
Symptom
What It Means
Solution
Rollers slipping
Insufficient grip on material
Replace rollers
Uneven roller wear
Incorrect alignment
Align or replace
Excessive roller gap
Reduced compression
Adjust gap
Roller bearing noise
Bearing wear
Replace bearings
Roller Wear Impact: Worn rollers cannot grip and compress material effectively. Material slips instead of being forced through the die, reducing throughput.
3. Material Changes
Change
Impact on Capacity
Solution
Higher moisture
Reduced throughput; steam issues
Dry material
Lower moisture
Poor binding; more fines
Add moisture
Coarser grind
Poor compression
Grind finer
Higher fiber
More energy required
Adjust parameters
Different material
Different compression requirements
Adjust die/operation
4. Operational Issues
Issue
Impact
Solution
Feed rate too low
Underutilized capacity
Increase feed
Feed rate inconsistent
Fluctuating production
Stabilize feed
Temperature too low
Poor binding; lower throughput
Increase conditioning
Roller gap incorrect
Poor compression
Adjust gap
5. Mechanical Issues
Issue
Impact
Solution
Bearing wear
Increased friction; reduced speed
Replace bearings
Gearbox wear
Reduced efficiency
Inspect/repair
Belt slippage
Reduced drive efficiency
Adjust/replace belts
Motor issues
Reduced power output
Test motor
Immediate Solutions: How to Restore Capacity
Step-by-Step Recovery
Step
Action
Details
1
Check amperage
Determine if motor is loaded
2
Inspect die
Check for wear, clogging, damage
3
Inspect rollers
Check wear, gap, alignment
4
Check material
Moisture, particle size
5
Check feed rate
Consistent, adequate
6
Check temperature
Conditioning optimal
7
Adjust and test
Make one change at a time
What to Do First
Priority
Action
Why
1
Check die condition
Most common cause
2
Check roller condition
Second most common
3
Check material moisture
Affects flow
4
Check roller gap
Affects compression
5
Check feed rate
Affects loading
When to Replace vs. Adjust
Condition
Action
Die holes enlarged >10%
Replace die
Die cracked
Replace die
Rollers worn flat
Replace rollers
Roller gap too wide
Adjust gap
Material too wet
Dry material
Material too coarse
Grind finer
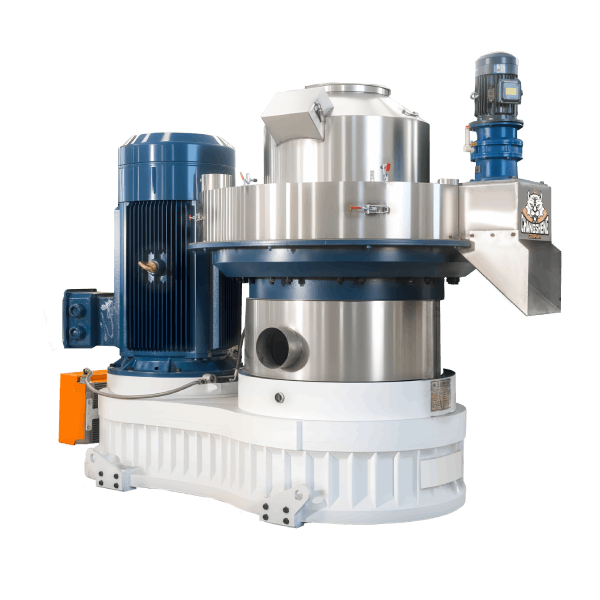
A pellet machine capacity drop from Shandong Changsheng Machinery Co., Ltd. can often be solved by replacing the die and rollers—the most common wear parts.
Component Inspection Guide
Die Inspection
Check
What to Look For
Action
Hole diameter
Enlarged holes
Replace if >10%
Hole clogging
Blocked holes
Clean
Surface condition
Cracks, wear
Replace if damaged
Compression ratio
Correct for material
Verify specification
Roller Inspection
Check
What to Look For
Action
Surface wear
Flat spots, grooves
Replace if worn
Bearing play
Excessive movement
Replace bearings
Roller gap
Correct setting
Adjust
Alignment
Uneven wear
Align or replace
Other Component Checks
Component
Check
Action
Bearings
Noise, play, temperature
Replace if worn
Gearbox
Noise, oil condition
Service or repair
Belts
Tension, wear
Adjust or replace
Motor
Amperage, temperature
Test or repair
Material and Operational Optimization
Moisture Control
Moisture Level
Effect on Capacity
Action
<10%
Poor binding; lower throughput
Add moisture
10-12%
Optimal
Maintain
12-15%
Reduced throughput
Dry material
>15%
Significant reduction
Dry material
Particle Size Control
Particle Size
Effect on Capacity
Action
<2 mm
Good flow; good capacity
Maintain
2-5 mm
Acceptable
Monitor
>5 mm
Poor compression; lower capacity
Grind finer
Feed Rate Optimization
Feed Rate
Effect
Action
Too low
Underutilized capacity
Increase
Optimal
Maximum capacity
Maintain
Too high
Overload; potential clogging
Reduce
Temperature Optimization
Temperature
Effect on Capacity
Action
<80°C
Poor binding; lower capacity
Increase conditioning
80-100°C
Optimal
Maintain
>120°C
Material degradation
Reduce conditioning
Case Study: Restoring Capacity in a Feed Mill
The Situation
A feed mill in Southeast Asia was experiencing a 30% capacity drop—from 1.2 t/h to 0.85 t/h. Production targets were missed, and operating costs were rising.
The Diagnosis
Investigation
Finding
Amperage
Low—motor not fully loaded
Die condition
Holes enlarged by 15%
Roller condition
Worn flat spots
Roller gap
Too wide (1.5 mm)
Material moisture
14% (too high)
Particle size
Variable (2-8 mm)
The Solution
Action
Implementation
Die replacement
Installed new premium die
Roller replacement
Installed new rollers
Roller gap
Adjusted to 0.3 mm
Moisture control
Installed moisture meter; adjusted drying
Grinding
Improved hammer mill screen maintenance
The Result
Metric
Before
After
Capacity
0.85 t/h
1.15 t/h
Amperage
Low
Normal
Pellet quality
Variable
Consistent
Production uptime
70%
92%
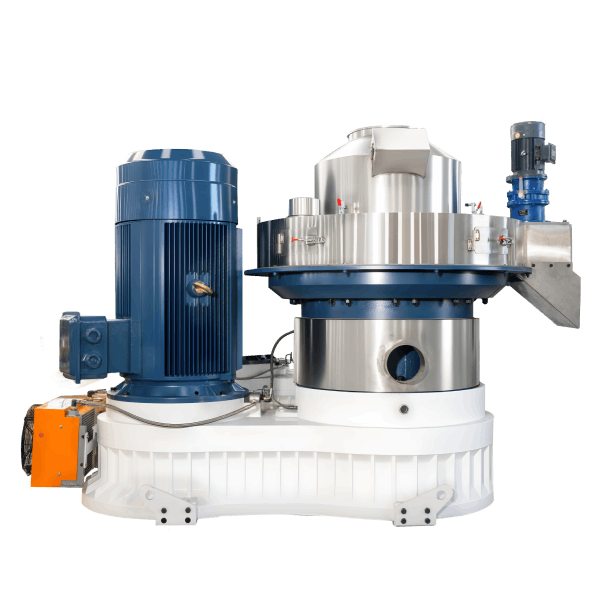
A pellet machine capacity drop from Shandong Changsheng Machinery Co., Ltd. can be restored through systematic diagnosis and component replacement.
Prevention: Maintaining Full Capacity
Daily Checks
Check
Frequency
Purpose
Amperage
Hourly
Detect overload early
Pellet quality
Each batch
Verify operation
Feed rate
Continuous
Consistent production
Temperature
Hourly
Optimal conditioning
Weekly Checks
Check
Frequency
Purpose
Die inspection
Weekly
Detect wear early
Roller inspection
Weekly
Detect wear early
Roller gap
Weekly
Verify adjustment
Material moisture
Weekly
Verify consistency
Monthly Checks
Check
Frequency
Purpose
Bearing condition
Monthly
Detect wear
Gearbox oil
Monthly
Check condition
Belt tension
Monthly
Verify drive
Motor condition
Monthly
Verify performance
Annual Maintenance
Task
Frequency
Purpose
Full inspection
Annually
Comprehensive check
Die replacement
As needed
Based on wear
Roller replacement
As needed
Based on wear
Bearing replacement
As needed
Based on condition
Procurement Checklist: Capacity Drop Prevention
Material Assessment
□ Moisture controlled (10-12%)
□ Particle size controlled (2-5 mm)
□ Material consistency verified
□ Foreign material removed
Component Inspection
□ Die condition checked
□ Roller condition checked
□ Bearing condition checked
□ Gearbox inspected
□ Belts inspected
Operational Parameters
□ Amperage monitored
□ Feed rate consistent
□ Temperature optimal
□ Roller gap correct
Maintenance
□ Daily checks performed
□ Weekly checks performed
□ Monthly checks performed
□ Annual maintenance scheduled
Frequently Asked Questions
1. What causes pellet machine capacity drop?
Capacity drop is caused by die wear, roller wear, material changes (moisture, particle size), operational issues (feed rate, temperature), and mechanical issues (bearings, gearbox).
2. How do I diagnose capacity drop?
Check amperage first, then inspect die and rollers, check material moisture and particle size, verify roller gap, and check feed rate and temperature.
3. What is the most common cause?
Die wear and roller wear are the most common causes. As die holes enlarge and rollers wear, compression decreases and capacity drops.
4. How do I restore capacity?
Replace worn die and rollers, adjust roller gap, control material moisture, maintain consistent feed rate, and optimize temperature.
5. How do I know when to replace the die?
Replace the die when holes are enlarged by >10%, when the die is cracked, or when pellet quality declines significantly.
6. How do I know when to replace the rollers?
Replace rollers when they have flat spots, grooves, or excessive wear. Check roller gap and bearing condition.
7. How does moisture affect capacity?
High moisture (>15%) reduces capacity by causing steam issues and poor flow. Low moisture (<10%) causes poor binding and more fines. Optimal is 10-12%.
8. How does particle size affect capacity?
Coarse particles (>5 mm) reduce compression and capacity. Fine particles (2-5 mm) flow better and compress more efficiently.
9. Can capacity drop be prevented?
Yes. Regular maintenance, proper operation, material control, and timely component replacement prevent capacity drop.
10. What is the best way to maintain capacity?
Monitor amperage daily, inspect die and rollers weekly, control material moisture and particle size, and replace worn components before they affect production.
Zhang Wei has over 12 years of experience in the biomass and feed pellet mill industry, with a background in mechanical engineering and international project execution. He has helped clients across Southeast Asia, the Middle East, Africa, Europe, and Latin America diagnose and solve capacity drop problems.
With hands-on experience in both the manufacturing workshop and client-side operations, Zhang brings practical insights into successful troubleshooting—from the factory floor to the customer’s production site.