How to Choose an Industrial Biomass Pellet Mill
News 2026-08-04
Choosing a pellet mill is a sequence of decisions, not a single comparison. The raw material decides the preprocessing and the die, the production target decides the capacity, the capacity decides the machine type, and the machine type decides what the specifications should be. Buyers who start from a price and a power figure usually end up with a machine that does not match their material, and the mismatch shows up after commissioning as low output, poor pellet quality, or excessive wear.
This page sets out the selection sequence for an industrial biomass pellet mill, from the raw material assessment through the capacity calculation, the machine type, the specifications, the performance checks, the manufacturer verification, the warranty, and the total cost. It is written for project developers and procurement teams who need to make a decision they can defend, and it applies the general selection logic to the specific case of industrial biomass production. Shandong Changsheng Machinery supplies industrial ring die pellet mills and complete biomass lines to overseas buyers, and the guidance below reflects how those machines are specified and where buyers most often misjudge them.
1. Identify your biomass raw materials
The raw material is the first decision because it drives everything that follows. The same machine cannot be expected to run all materials equally well on the same configuration, and the raw material assessment should be written down before any machine is compared.
Sawdust and wood chips. Sawdust is the most predictable material because it is already close to the particle size the die needs, and it usually needs drying rather than grinding. Wood chips are much coarser and need a hammer mill or a chipper. The two lead to different line configurations, and the quotation should state which one the line is designed for.
Rice husk. Rice husk is abrasive and high in ash, and it wears dies and rollers faster than wood. The die material and the wear parts plan should be set for the abrasiveness, and the ash of the finished pellet should be checked against the market.
Corn stover and straw. These materials are fibrous and bulky, and they usually need grinding before pelletizing and often a binder or a blend with a better-binding material. They are harder to pelletize than sawdust, and the die specification and the preprocessing should be confirmed by testing the actual material.
Peanut shell. Peanut shell is denser and more abrasive than sawdust, and it needs grinding and a die specification suited to the material. Its ash and abrasiveness should be checked before the line is specified.
EFB and coir pith. Empty fruit bunches and coir pith are high in moisture and need dewatering and drying before pelletizing, and EFB is also long-fibered and needs grinding. Coir pith may carry soluble salts that have to be tested and, where necessary, washed out before the material is pelletized.
Why raw material testing matters. A material name is not a specification. Two sawdust streams from different sources can differ in particle size, moisture, and abrasiveness, and the same machine will behave differently on each. The test on your actual material is what establishes the achievable output, the pellet durability, the power consumption, and the wear rate, and it is the only reliable basis for choosing between two machines. A supplier who quotes a specification without a test on your material is working from assumption, and that assumption is likely to be tested in production.
2. Determine your required production capacity
Daily production target. Start from the tonnage the project needs to sell, not from the tonnage a machine can produce. The market the pellets are sold into sets the volume the operation can absorb, and a line that produces more than the market can take ties up capital in inventory.
Operating hours. The daily target divided by the operating hours gives the average hourly output the line has to sustain. The operating hours should be realistic, allowing for start-up, shutdown, maintenance, and the interruptions that occur in any plant.
Actual output versus rated capacity. The rated capacity of a machine is not the output it will deliver on your material. The actual output depends on the material, its moisture, the particle size, the die specification, and the stability of the feed, and it should be confirmed in a trial on the actual material. A capacity quoted without a stated material and moisture is not a specification.
Capacity calculation example. Take a project that plans to produce 20 tonnes of biomass pellets per day and to run the line for 10 hours per day. The average output required is 20,000 kg divided by 10 hours, which is 2,000 kg per hour. That figure is the average across the operating hours, and it is not the same as the rated capacity of the machine, because the machine has to cover start-up, shutdown, and the interruptions, and because the output on the actual material may be lower than the rated figure. The calculation gives the target; the trial gives the machine.
Production line expansion. The capacity decision should also allow for the future. If the project is likely to increase its output, the machine should be selected with the expansion in mind, either because the model can be upgraded with a larger drive or die, or because the layout and the electrical supply leave room for a second line. A machine that is sized exactly to today’s target and has no headroom is usually the more expensive choice over the life of the project.
3. Choose the right type of pellet mill
Flat die pellet mill. A flat die machine has a horizontal die with rollers on top, and it suits smaller operations, intermittent duty, and materials that are already well prepared. It is simpler and cheaper to build, and its limitation is that the die area is smaller relative to the machine size.
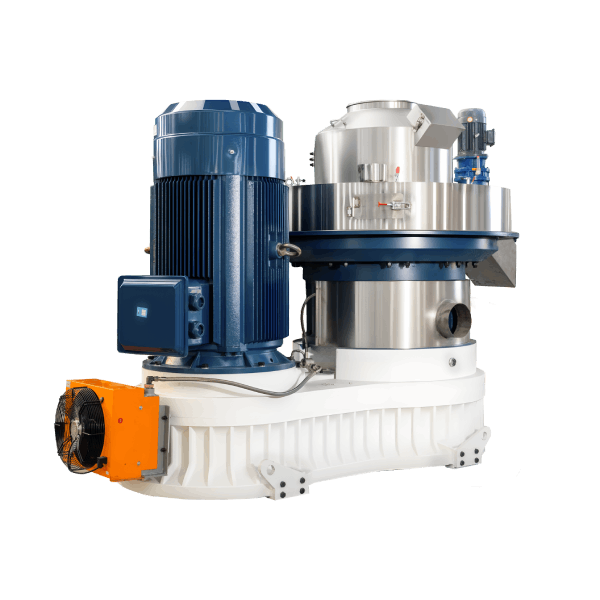
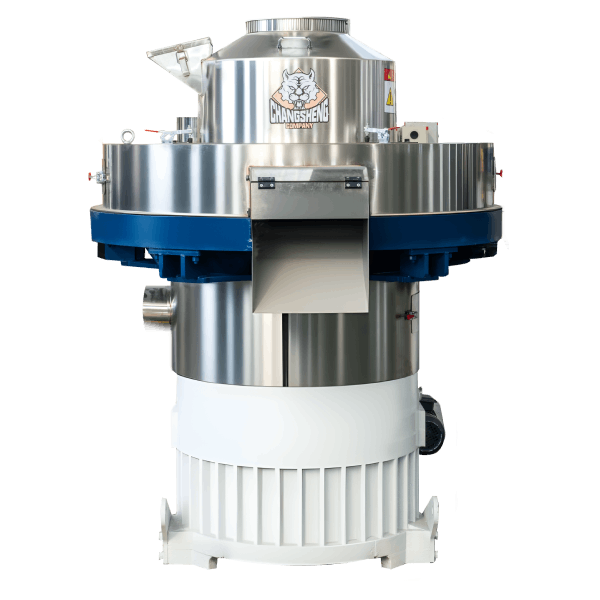
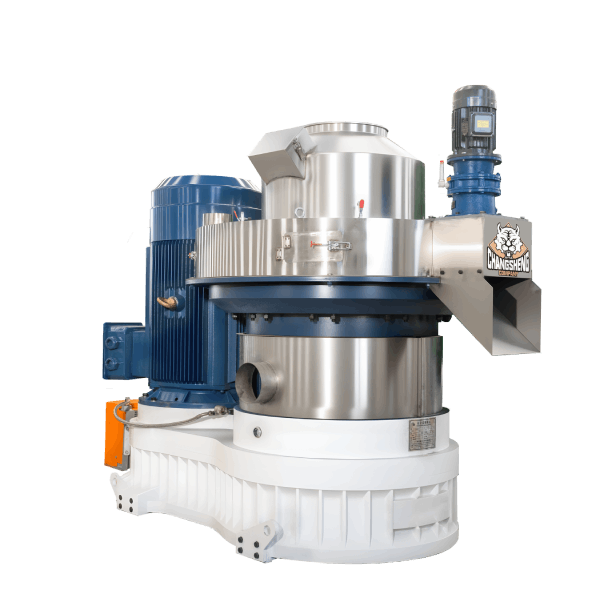
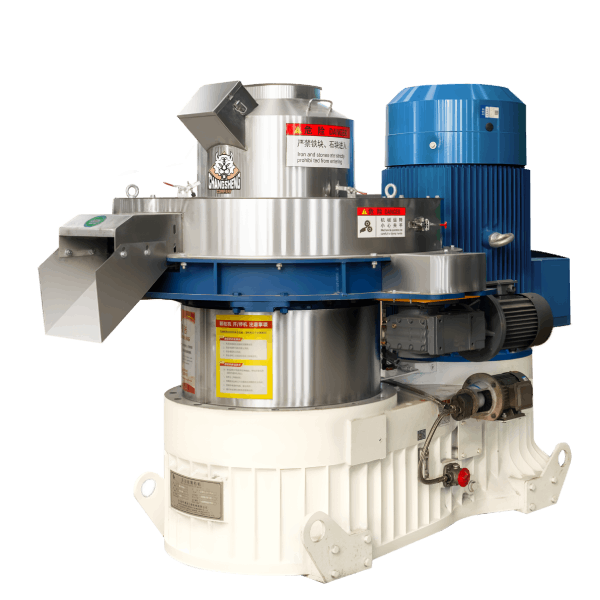
Ring die pellet mill. A ring die machine has a circular die with rollers inside it, and the larger die area and the even wear allow it to run continuously at commercial output and to hold a steady pellet quality over a shift. It is the standard design for industrial biomass production, and it costs more.
Flat die vs ring die. The two designs differ in several practical ways, and each difference points to a different operating pattern.
Structure. The flat die has a horizontal die with rollers on top, and the ring die has a vertical die with rollers inside. The ring die gives a larger die area and more even wear; the flat die is simpler and cheaper to build.
Pressing action. The flat die presses the material through the die from above, and the ring die presses it through from the inside out. The pressing action affects how evenly the material is distributed across the die and how the wear is spread.
Application. The flat die suits small and intermittent production, and the ring die suits continuous commercial and industrial production at higher output.
Maintenance. The flat die has a simpler maintenance routine and smaller wear parts, while the ring die has a larger die and roller set that is replaced less often per ton but at a higher cost per replacement. The maintenance plan and the spare parts budget should be set for the design that is chosen.
Selection focus. For the flat die, the selection focus is on the output, the material fit, and the operating pattern. For the ring die, the selection focus adds continuous operation, steady feed, and a maintenance schedule.
The choice should be made on the production scale and the duty cycle for the project, not on a general claim that one design is better than the other.
When to choose an industrial ring die pellet mill. The ring die is the right choice when the line has to run continuously at commercial output, when the feed has to be steady for hours at a time, when the drive and the gearbox have to carry the load without interruption, and when the die and roller set has to be planned for a maintenance schedule rather than replaced when it fails. Where those conditions do not apply, the flat die may be the more appropriate and more economical choice.
4. Check the key technical specifications
Motor and gearbox. The motor should be checked on its rated power, its efficiency class, its protection rating, and its voltage and frequency for the destination. The gearbox should be checked on its transmission structure, its rated torque, its lubrication, and its cooling, and the rated torque should be checked against the motor power and the duty cycle.
Die and roller. The die should be checked on its material and heat treatment, its diameter and working width, its hole diameter and compression ratio, and its machining precision, and the specification should be matched to your material and pellet diameter. The roller assembly should be checked on the roller material, hardness, and surface condition, on the bearing arrangement, and on the adjustment mechanism, and the replacement cost should be part of the comparison.
Feeding system. The feeder should be checked on its type and its suitability for the flow behavior of the material, because a feeder designed for a free-flowing material may bridge or surge on a light, fibrous one.
Electrical control system. The control system should be checked on its electrical protection, its monitoring of the main parameters, its fault alarms, and the degree of automation, and it should be specified for the operation and the labor cost at the site.
Installation requirements. The machine dimensions, weight, foundation, and electrical supply should be checked against the site, and the quotation should state what the supplier provides and what the buyer has to provide.
5. Evaluate pellet mill performance and quality
Production capacity test. The capacity should be measured on a continuous run on your material, at the moisture the line will deliver at the die, not on a short burst on prepared material.
Pellet quality. The pellet should be tested after cooling and resting for moisture, ash, durability, bulk density, and diameter and length, using the methods the customer will use.
Power consumption. The power draw at the operating load should be recorded during the trial, so that the specific energy consumption per ton can be estimated and compared with another machine.
Continuous operation. The machine should be run long enough to show that it holds its output and its pellet quality over a shift, not only for the first twenty minutes.
Wear parts and maintenance. The die and roller consumption, the spare parts, and the maintenance routine should be part of the evaluation, because they determine the operating cost over the life of the machine.
6. Choose a reliable pellet mill manufacturer
A manufacturer should be able to show that it makes the machine, not only that it sells it. The useful checks are whether there is an actual production workshop, whether the die, rollers, gearbox, and main shaft can be shown, whether a continuous running video can be provided, whether there are test records from projects with similar material and capacity, whether a material test and a finished pellet quality report can be provided, whether a complete equipment list and a wear parts list are available, and whether installation, commissioning, and overseas technical support are within the supplier’s capability.
ISO 9001 is a voluntary quality management system certification, and it says something about how the manufacturer organizes its processes, not about the performance of a particular machine. CE marking is a mandatory market access requirement for machinery placed on the EU market, and it is not a quality grade or a performance ranking. Both should be verified for authenticity and applicability to the machine being supplied, rather than counted as quality points.
7. Check the warranty terms before you sign
The warranty is part of the price, and it should be checked in the same way as the specification. The items to confirm in writing are the warranty period and its start date, what the warranty covers and what it excludes, whether wear parts such as dies and rollers are inside or outside the warranty, how a claim is made and how quickly the supplier is expected to respond, whether replacement parts are shipped free or at cost, and whether labor and travel for a warranty repair are included. A general statement that the machine is covered for a period is not a warranty term until those items are written down, and the warranty scope varies between suppliers and contracts.
8. Calculate the total investment and operating cost
The total cost is built from the equipment purchase cost, the shipping, the installation and commissioning, the electricity, the die and roller replacement, the spare parts and maintenance, the labor, and the cost of downtime. The operating and maintenance parts can exceed the purchase price over the life of the machine, and the comparison should be made on the total rather than on the invoice.
The calculation is best done with a worked example that the buyer fills in with their own figures. Take the rated power, the average load as a fraction of the rated power, the running hours per day, the running days per year, and the local electricity tariff, and the annual electricity cost is the product of those figures. The die and roller cost is the number of replacements per year times the replacement cost, and the number of replacements per year is the running hours divided by the expected life of the die on your material. The maintenance and labor cost is the routine labor hours times the labor rate, plus the cost of unplanned downtime.
The buyer who fills in those figures gets a five-year cost that is specific to their project, and it is that figure, not the invoice price, that should be compared between suppliers. A supplier who cannot provide the average load, the expected die life, and the wear parts consumption on your material has not given you the inputs for the calculation.
9. Pellet mill purchasing checklist
- Define the raw material, its form, its moisture range, its particle size, and its abrasiveness.
- Test the material for moisture, particle size, ash, and abrasiveness.
- Define the daily production target and the operating hours, and calculate the average hourly output.
- Decide whether the site needs a standalone machine or a complete line.
- Select the machine type against the production scale and the duty cycle.
- Review the motor, gearbox, die, roller assembly, feeder, and control system against the material and the duty cycle.
- Request a trial on your material with pre-agreed acceptance criteria, including output, pellet durability, and power consumption.
- Verify the manufacturer’s workshop, components, running records, and references.
- Check the warranty terms, the wear parts, and the technical support in writing.
- Compare quotations on scope, exclusions, warranty terms, and total cost, not on price alone.
Bottom line
Choosing an industrial biomass pellet mill is a sequence: the raw material sets the preprocessing and the die, the production target sets the capacity, the capacity and the duty cycle set the machine type, and the machine type sets the specifications. Test the material, calculate the capacity from the production target rather than from the machine rating, allow for the expansion you expect, select the type against the duty cycle, check the specifications against the material, and verify the performance in a trial on your own material. Verify the manufacturer’s workshop and running records, treat ISO 9001 and CE marking as process and compliance signals rather than quality grades, and check the warranty terms in writing rather than accepting a general statement. Compare the total cost over the life of the machine rather than the invoice, and specify the material, the capacity, the die, the warranty, and the acceptance test in the quotation before you sign.
If you are selecting an industrial biomass pellet mill and want a quotation you can compare item by item, send the material, the target daily production, the pellet diameter, and the destination, and the Shandong Changsheng Machinery team can propose a machine or line configuration with the die specification, the scope, and the exclusions stated.