Pellet Mill Roller Slipping: Causes, Diagnosis and Fixes
News 2026-10-20
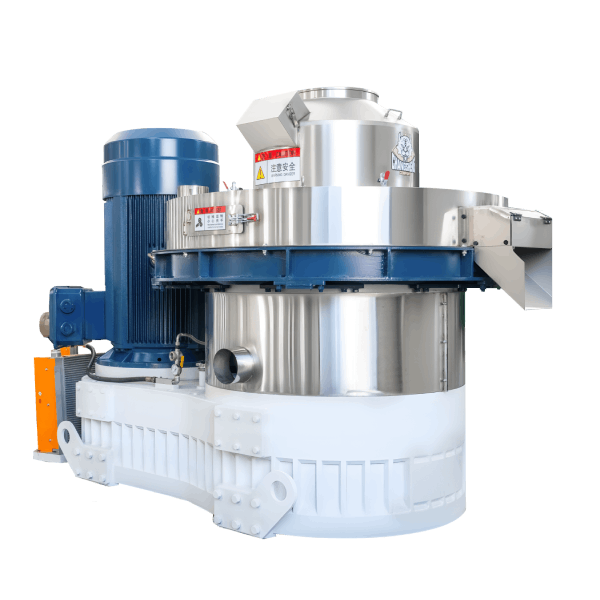
A slipping roller in a pellet mill usually shows up as lost compression, not lost rotation. The roller is still turning, but it is no longer gripping material and pressing it into the die. Output falls, pellet quality drops, and motor current often falls with it because the die is underloaded. There is an exception: if a roller bearing has seized or a roller shaft is damaged, the roller may stop rotating or rotate intermittently, and the symptom then looks like drive slip. That case is covered in the comparison below.
This matters because replacing the roller is often the wrong first move. Roller slip is a symptom of one of four conditions: clearance too large, roller surface worn or glazed, material too dry or too fine, or the roller assembly not turning freely. Each has a different fix. Two of them do not require a new roller at all.
This article covers how to separate roller slip from drive slip, how to check each cause in order, how roller type affects what you see, how slip and die wear reinforce each other, when adjustment is enough and when replacement is required, and what to verify after the fix.
Roller Slip or Drive Slip: Decide This First
The two failures look similar from the control panel: output falls and pellet quality drops. They require different actions, and treating one as the other wastes parts.
| Symptom | Roller slip | Drive slip |
|---|---|---|
| Roller rotation | Turning, but not gripping material | Not turning, or turning intermittently |
| Motor current | Below the normal range stated in the machine manual, because the die is underloaded | Fluctuating, with possible spikes |
| Noise | No new noise from the drive | Belt squeal, gearbox noise, or coupling noise |
| Output | Falls gradually | Falls suddenly or stops |
| Inspection | Roller surface glazed or worn, clearance too large | Belt tension low, coupling worn, gearbox fault |
If motor current falls below the manual range while output falls, the die is underloaded. That points to roller slip, not drive slip. If motor current fluctuates and there is new noise from the drive, check the belt, coupling, and gearbox before touching the rollers.
What Roller Type Changes
Roller type affects how slip appears and what to inspect. The machine manual takes precedence over this section.
| Roller type | How slip usually appears | What to inspect |
|---|---|---|
| Grooved roller | Material stops being drawn into the grooves; grooves fill with compacted material | Groove depth and groove edges; packed material in the grooves |
| Smooth roller | Grip depends on surface texture and pressure; slip appears as polished surface and lost compression | Surface roughness and glazing; clearance against the manual specification |
| Toothed roller | Teeth wear or break; material is not drawn in and compression is lost unevenly | Tooth condition and tooth height; wear pattern across the roller face |
A roller with filled grooves or broken teeth can still rotate freely and still look intact from a distance. Check the surface, not only the rotation.
Four Causes of Roller Slipping
Check in this order. The first two account for most cases.
1. Roller Clearance Too Large
Why it causes slip: Clearance is the gap between the roller and the die surface. If the gap is too large, the roller cannot press material into the die holes with enough force. Material sits at the die surface instead of being pushed through. The roller turns, but it is not doing compression work.
What to check: Measure clearance against the machine manual specification. Check all rollers, not just one, because uneven clearance causes uneven compression and localized wear.
What to do: Adjust clearance to the manual specification. Do not set clearance tighter than the manual range to compensate for worn rollers or a die problem. Tighter clearance increases friction and heat, can damage the die surface, and does not restore the roller’s ability to grip material.
2. Roller Surface Worn or Glazed
Why it causes slip: The roller surface grips material through a combination of shape and surface texture. A worn roller has a surface that slides over material instead of gripping it. Wear usually shows as a flattened surface, grooves, or a surface that has become bright and smooth. A glazed roller has a polished, hardened surface layer that produces the same effect. Both conditions reduce the force transmitted to the material.
What to check: Inspect the roller surface for flattening, grooving, or a shiny, polished appearance. Compare against a new roller if available. Check the wear pattern across all rollers; uneven wear points to a clearance or alignment problem, not just normal wear. Match the inspection to the roller type in the table above.
What to do: Replace worn or glazed rollers. Do not attempt to restore grip by roughing the surface outside the manufacturer procedure. An incorrectly roughened roller can damage the die.
3. Material Too Dry or Too Fine
Why it causes slip: Roller grip depends partly on the material. Dry material produces excessive fines, and fines behave like a lubricant between the roller and the die. The roller turns on a layer of fine powder instead of gripping and compressing material. Material that is too fine has the same effect, even at correct moisture.
What to check: Moisture at the pellet mill inlet, not at the raw material storage pile. Particle size distribution after grinding. Fines proportion in the material entering the die chamber.
What to do: Correct moisture or particle size before adjusting the machine. If moisture is within the die working range but the material still slips, check whether the grinding stage is producing excessive fines. Whether a given moisture level or fines proportion is acceptable depends on the material and the die specification, and must be confirmed by a pelletizing test, not assumed from a general figure. A useful test record should include material type, moisture, particle size, pellet diameter, die specification, test duration, and output result.
4. Roller Assembly Not Turning Freely
Why it causes slip: If a roller does not rotate freely on its shaft, it drags instead of rolling. The result looks like slip because compression is lost, but the cause is mechanical, not surface-related. Worn bearings, insufficient lubrication, or a damaged shaft can all produce this condition.
What to check: With the machine stopped and locked out, check whether each roller rotates freely by hand. Check bearing condition and lubrication according to the machine manual. Check for abnormal play or noise.
What to do: Replace worn bearings and restore lubrication according to the machine manual. If the shaft is damaged, replace it according to the manufacturer procedure. Do not return the machine to service with a roller that does not rotate freely, because the drag loads the drive and damages the die unevenly.
Diagnostic Order
Use this order to avoid replacing parts before the cause is confirmed.
- Confirm whether the symptom is roller slip or drive slip, using the comparison table above.
- Check roller clearance against the machine manual specification.
- Inspect roller surfaces for wear, glazing, filled grooves, or broken teeth, according to the roller type.
- Check moisture and particle size at the pellet mill inlet.
- Check that each roller rotates freely with the machine locked out.
- If all five are within specification and slip continues, inspect the die surface for wear or glazing.
Slip and Die Wear Reinforce Each Other
Roller slip is not only a symptom. It also causes damage that makes slip worse.
When the roller does not grip material, compression at the die surface is reduced. Material sits at the die hole entrance longer than it should. That extends the time the hole entrance is exposed to friction and heat, and the entrance wears faster. A worn hole entrance reduces roller grip further, because the material has less resistance to push against. The result is a cycle: slip causes die wear, and die wear causes more slip.
This is why a worn die reduces roller grip even when the rollers are correct. It is also why restoring roller grip without checking the die surface often produces a short-lived fix.
What to check on the die surface: Look for a bright or polished hole entrance, a smoothed hole interior, and any change in hole entrance diameter compared with the die supplier specification. Confirm with the die supplier documentation whether the die is still within service limits. Do not apply a value from one die model or one material as a general standard.
Adjust or Replace: Decision Points
| Condition found | Action |
|---|---|
| Clearance outside the manual range, roller surface good | Adjust clearance to the manual specification |
| Roller surface worn or glazed, clearance correct | Replace the rollers |
| Clearance outside range and roller surface worn | Replace the rollers, then set clearance to the manual specification |
| Material too dry or too fine | Correct moisture or particle size before adjusting the machine |
| Roller does not rotate freely | Replace bearings or shaft according to the machine manual |
| All checks within specification, slip continues | Inspect the die surface for wear or glazing, and confirm against die supplier limits |
Do not combine a clearance adjustment with a roller replacement unless both are needed. Adjusting clearance on worn rollers produces uneven compression and accelerates die wear.
New Roller Break-In
New rollers do not reach full grip immediately. The surface needs to seat against the die and the material.
Follow the machine manual for break-in feed rate and duration. If the manual does not specify a procedure, the general approach is to run at reduced feed rate for the first period of operation and check motor current, pellet quality, and roller surface condition before returning to normal rate. Do not judge a new roller’s performance at full feed rate on the first run.
If motor current stays below the manual range after break-in, recheck clearance before assuming the roller is faulty.
What to Check After the Fix
Restoring grip is not the same as confirming the fix. Check the following before returning to normal feed rate. Limits must come from the machine manual and the die supplier documentation.
| Check item | What to confirm |
|---|---|
| Motor current | Returning to the normal range stated in the machine manual at normal feed rate |
| Output | Returning to the expected level for the material and die specification |
| Pellet quality | Density and durability consistent with normal production |
| Roller rotation | All rollers rotating freely and evenly under load |
| Die surface | No new glazing, grooving, or heat marks |
| Noise and vibration | No abnormal sound from the roller assembly or drive |
If motor current stays below the manual range after the fix, compression is still insufficient. Recheck clearance and roller condition before increasing feed rate.
Preventing Roller Slip
Roller slip is usually a maintenance and material condition problem, not a sudden failure.
| Check | Suggested frequency | Purpose |
|---|---|---|
| Roller clearance | Weekly, or after roller replacement | Confirm clearance within specification |
| Roller surface condition | Weekly | Detect wear, glazing, filled grooves, or broken teeth before output falls |
| Roller free rotation | Weekly, with the machine locked out | Detect bearing or shaft problems early |
| Moisture at pellet mill inlet | Each shift, or at material source change | Prevent fines from acting as a lubricant |
| Particle size and fines proportion | Daily, or at material source change | Detect excessive fines before they cause slip |
| Motor current at normal operation | Each shift | Detect underloading before output falls |
| Die hole entrance condition | Weekly, or after any slip event | Detect die wear that reduces roller grip |
General maintenance intervals should follow the machine manufacturer manual.
Spare Parts to Hold for Roller Slip
Repeated roller slip consumes parts faster than normal operation. Exact part numbers and recommended stock levels must come from the machine manual and the roller supplier documentation.
| Spare part | Why it is needed after roller slip |
|---|---|
| Rollers | Surface wear, glazing, filled grooves, or broken teeth from repeated slip |
| Roller bearings | Wear from dragging or uneven load |
| Roller shaft | Damage from a roller that does not rotate freely |
| Roller assembly seals | Dust and heat exposure during slip |
| Die | Accelerated wear from uneven compression and extended material dwell at the hole entrance |
Whether the die needs replacement depends on hole entrance diameter change, hole interior smoothness, and pellet density decline. The limit must come from the die supplier documentation or the machine manual.
Holding these parts does not prevent slip, but it reduces downtime when slip requires replacement rather than adjustment.
When Roller Slip Is a Configuration Problem
If slip continues despite clearance, roller condition, material condition, and roller rotation all being confirmed by test and manual, the roller or die configuration may not match the material. This is more common when a machine selected for one material is now running a different material with different density, fiber content, or fines behavior.
In that case, adjustment and replacement will keep production running but will not eliminate the slip. The options are to change the roller or die configuration, or to change the material preparation so it grips correctly. A pelletizing test with the actual material is the most reliable way to confirm which option is suitable before making a change.
If the slip cannot be resolved on site, send the material type, moisture, particle size, roller clearance, roller condition, die specification, and motor current at normal operation for a configuration review.
Maintenance parameters, roller clearance values, wear limits, and acceptance criteria in this article must be confirmed against the machine manual and the roller and die supplier documentation. This article does not provide universal values for these items.