Wood Waste to Fuel: Conversion Options & Buyer Guide
News 2026-10-09
Wood Waste to Fuel: How to Convert Wood Waste into a Usable Fuel Stream
Wood waste to fuel is not a single process. It is a family of conversion routes that turn sawdust, shavings, chips, bark, and other wood residues into a fuel that can be burned in a boiler, kiln, furnace, or pellet stove. The right route depends on the wood waste type, moisture, particle size, contamination level, available volume, and the heat demand at the site.
The practical question for a buyer is not which equipment is the cheapest. The real question is which conversion route fits the specific wood waste, the existing or planned combustion equipment, and the local regulatory environment, and which route has a defensible cost or revenue case over several years.
This guide is written for sawmills, woodworking plants, plywood and board plants, furniture factories, pallet workshops, wood processing facilities, and biomass fuel producers. It covers the wood waste types, fuel conversion routes, technical requirements, cost factors, regulatory considerations, and procurement steps. For disposal option comparison in general, see the dispose of wood waste page on this site. For the process of turning sawdust into pellets, see the turn sawdust into pellets page on this site.
What Counts as Wood Waste for Fuel
Wood waste for fuel is not a single material. It includes several categories with different characteristics.
Sawdust and fine wood dust from sawing, sanding, and cutting.
Wood shavings from planing and profiling.
Wood chips and offcuts from milling, joinery, and pallet production.
Bark from debarking operations.
Construction and demolition wood, which may include treated, painted, or contaminated wood.
Pallet and crate wood, which may include nails, staples, and treated wood.
Plywood, MDF, and board plant residue, which may contain resin and glue.
Each category has different moisture, particle size, contamination level, and suitability for fuel conversion. A conversion route that works for clean softwood sawdust may not work for treated construction wood or resin-containing board residue.
Wood Waste by Species and Treatment for Fuel
Species affects moisture, ash content, and fuel quality. Softwood sawdust from pine, fir, and spruce usually pelletizes more easily because of higher lignin content and produces strong pellets with lower ash. Hardwood sawdust from oak, maple, and beech is denser and more abrasive, and may require a higher compression ratio to reach the same pellet durability. Ash content is usually lower in clean softwood and higher in mixed wood waste with bark or soil.
Treatment status affects fuel suitability and, in most regions, waste classification. Clean, untreated wood is usually suitable for fuel. Treated wood may contain preservatives that produce harmful emissions during combustion and may not be suitable for fuel. Painted wood may contain heavy metals. Glued wood, such as plywood and MDF, may contain resins and adhesives that affect combustion and ash behavior. These categories may be subject to different regulatory requirements and may not be suitable for fuel conversion.
Waste classification is the regulatory framework that distinguishes clean wood from treated, painted, or glued wood, and from mixed construction and demolition waste. In most regions, these categories have different disposal and processing rules. For a fuel project, this means that the wood waste must be classified correctly, and that the fuel conversion route must be compatible with the classification. This classification also affects documentation, transport, and end use of the finished fuel.
Before choosing a fuel conversion route, confirm the species mix, treatment status, and waste classification of the wood waste.
Wood Waste Supply Chain
Wood waste supply chain affects feedstock consistency. Sawmill sawdust is usually consistent in species and particle size, and supply follows the sawing schedule. Furniture factory sawdust may contain mixed species and glue residue, and supply follows the furniture production schedule. Plywood and board plant residue may contain resin and glue, and supply follows the board production schedule. Pallet and crate wood may contain nails and staples, and supply follows the pallet repair and production schedule. Construction and demolition wood is the most variable, with mixed species, treatment status, and contamination.
Construction and demolition wood is also seasonal in many regions, because demolition activity follows construction cycles and weather. Other wood waste sources, such as sawmill and furniture factory residue, are usually less seasonal.
For a fuel project, feedstock consistency affects the die selection, the drying requirement, the contamination control, and the market. A project running on a single consistent sawdust source can use a simpler configuration than a project running on mixed construction and demolition wood.
Fuel Conversion Routes for Wood Waste
Direct Combustion of Wood Chips
Clean wood chips can be burned directly in biomass boilers, kilns, and some industrial furnaces. This route requires the boiler to be designed for the chip size and moisture. Direct combustion is common in sawmills, board plants, and wood processing facilities with continuous heat demand. It requires the least preprocessing of the fuel conversion routes, but it also produces the least uniform fuel and requires the largest combustion chamber.
Pelletizing
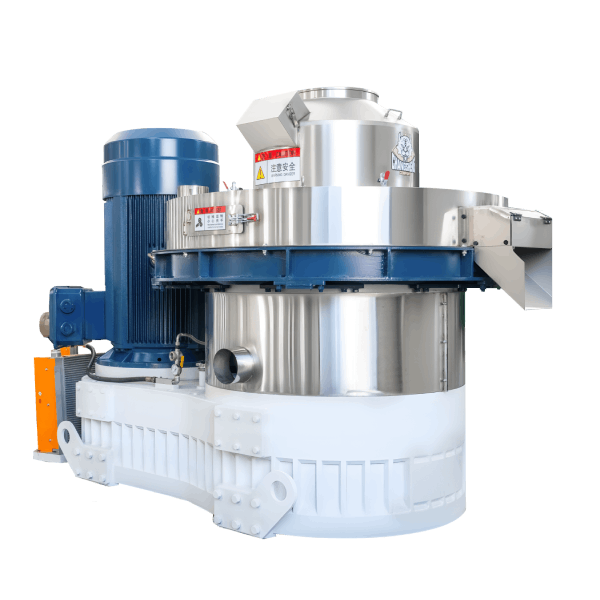
Pelletizing converts wood waste into dense, uniform pellets for fuel. Pellets are used in pellet stoves, pellet boilers, industrial boilers, and power generation. Pelletizing requires a production line with grinding, drying, pelletizing, cooling, screening, and packing. Pellets have higher density, more uniform size, and lower moisture than wood chips, which makes them suitable for markets that require a consistent fuel.
Briquetting
Briquetting compresses wood waste into larger briquettes for industrial furnaces, kilns, and some heating systems. Briquetting can accept a wider range of particle sizes and moisture than pelletizing, and may require less drying in some cases. Briquettes are less uniform than pellets and are usually sold into industrial markets rather than residential markets.
Torrefaction and Carbonization
Torrefaction and carbonization convert wood waste into a higher-energy, more coal-like fuel. Torrefied wood is hydrophobic and easier to grind, which makes it suitable for co-firing with coal in power plants. Carbonized wood produces charcoal and charcoal briquettes. Both routes require additional equipment and process control compared with pelletizing and briquetting, and are usually applied at larger scale.
Comparison of Wood Waste to Fuel Routes
Route: Direct Combustion of Wood Chips
Fuel Form: Chips
Preprocessing: Low
Typical Use: On-site biomass boilers and kilns
Main Constraint: Boiler fuel specification
Route: Pelletizing
Fuel Form: Pellets
Preprocessing: Medium to high
Typical Use: Pellet stoves, pellet boilers, industrial boilers
Main Constraint: Moisture, particle size, contamination, market
Route: Briquetting
Fuel Form: Briquettes
Preprocessing: Medium
Typical Use: Industrial furnaces and kilns
Main Constraint: Industrial market access
Route: Torrefaction
Fuel Form: Torrefied pellets or powder
Preprocessing: High
Typical Use: Co-firing with coal in power plants
Main Constraint: Capital cost and process control
Route: Carbonization
Fuel Form: Charcoal and charcoal briquettes
Preprocessing: High
Typical Use: Charcoal markets and some industrial uses
Main Constraint: Capital cost and emission control
The preprocessing level in this table depends on the wood waste type, moisture, particle size, and contamination level. A sawdust feedstock may require only drying and pelletizing, while mixed construction and demolition wood may require sorting, shredding, grinding, and metal removal before pelletizing or briquetting.
The correct route depends on the specific wood waste, the existing or planned combustion equipment, the local market, and the project economics.
Technical Requirements for Wood Waste to Fuel
Moisture
Moisture is the most important variable.
For direct combustion in biomass boilers, wood chips can often be burned in the range of about 20 to 45 percent moisture, depending on boiler design and combustion technology.
For pelletizing, target moisture before pelletizing is usually around 10 to 15 percent, depending on wood species, die compression ratio, and machine configuration.
For briquetting, moisture requirements are usually between those of chips and pellets, depending on briquette press design.
The exact target should be confirmed with a pelletizing, briquetting, or combustion test on the actual wood waste.
Particle Size
Particle size affects feeding, combustion, compression, and pellet quality.
For direct combustion in biomass boilers, chip size is usually specified by the boiler manufacturer.
For pelletizing, target particle size is usually in the range of 2 to 5 mm, depending on die specification.
For briquetting, larger particle sizes may be acceptable, depending on briquette press design.
Grinding is required if the wood waste contains chips, shavings, or offcuts that exceed the target size.
Contamination
Contamination affects both equipment life and emissions. Nails, staples, and stones must be removed by magnetic separation and screening. Treated, painted, and glued wood may need to be excluded, depending on fuel application and local regulations. Air classification removes sand and stones where mineral contamination is high.
Density and Energy Content
Density and energy content affect transport cost and combustion behavior. Pellets have higher bulk density than chips, which reduces transport cost per unit of energy. Briquettes have intermediate density. Torrefied fuel has higher energy content per unit mass than raw wood. The exact values depend on wood species, moisture, and process, and should be confirmed by laboratory test for the specific wood waste.
Local Market and Fuel Route Choice
Local market affects the economics of each fuel conversion route. Direct combustion for on-site boilers requires an internal heat demand. Pelletizing requires a market for pellets, which may be local, regional, or export. Briquetting requires a market for briquettes, usually industrial. Torrefaction and carbonization require specific markets, such as coal co-firing or charcoal, and are usually applied at larger scale.
Where the local market is weak, the project may need to sell into regional or export markets, which adds transport cost and quality requirements. Pellets have an advantage in export markets because of higher bulk density and lower moisture. Briquettes and torrefied fuel have specific market requirements that should be confirmed before planning.
Pellet Quality Standards for Fuel
For export or higher-grade markets, wood pellet quality may need to meet standards such as ISO 17225 for solid biofuels. Some markets also use certification schemes such as ENplus, and some North American markets use PFI specifications. Key quality parameters include moisture, ash content, durability, fines, and pellet diameter.
Ash content depends on wood species, bark content, and contamination. Boilers with ash removal systems can accept higher-ash pellets. Home pellet stoves usually require low-ash pellets. Exact grade limits should be confirmed against the current official standard, not assumed from a general figure.
Cost Structure of Wood Waste to Fuel
The cost of converting wood waste to fuel depends on the route.
For direct combustion of wood chips, the cost includes boiler equipment, fuel preparation, and maintenance. The saving is the avoided purchase of fossil fuel or purchased biomass. Payback depends on heat demand, fuel price, and boiler efficiency.
For pelletizing, the cost includes the production line, drying and grinding equipment, electrical infrastructure, civil works, installation, spare parts, and operating cost. The revenue depends on pellet price, market access, and product quality. Cost per ton of pellets is the figure that matters, not machine price alone.
For briquetting, the cost is usually lower than pelletizing because less drying and grinding may be required, but the product value is usually lower.
For torrefaction and carbonization, the cost is higher because of additional equipment and process control, but the product may sell at a higher price in specific markets.
Regulatory Considerations
Wood waste to fuel is regulated in most regions. Key regulatory areas include:
Waste classification, which distinguishes clean wood from treated, painted, or glued wood.
Air quality regulations, which restrict emissions from combustion.
Fuel quality standards for pellets and briquettes.
Fire and explosion safety regulations for wood dust.
Transport and storage regulations for wood fuel.
Subsidy and incentive programs for renewable energy, where applicable.
Regulations vary by country and by region. For example, some European countries have specific fuel quality standards under ISO 17225 and ENplus, and specific air quality regulations for wood-fired boilers. Some North American regions have specific combustible dust standards under NFPA. All regulatory requirements should be confirmed with the relevant authority and with a qualified advisor before choosing a fuel conversion route.
Common Mistakes in Wood Waste to Fuel Projects
First, choosing a fuel conversion route before testing the wood waste. Moisture, contamination, particle size, treatment status, and waste classification determine which routes are feasible.
Second, ignoring combustion equipment compatibility. A pellet stove, a pellet boiler, and an industrial boiler each require different pellet specifications.
Third, underestimating drying and grinding requirements. These stages often represent a significant part of total project cost.
Fourth, ignoring contamination and treatment status. Treated, painted, and glued wood may not be suitable for fuel, and may produce harmful emissions.
Fifth, ignoring regulatory requirements. Air quality, waste classification, fuel quality, and fire safety regulations affect which routes are allowed.
Sixth, buying equipment before confirming volume and market. A pellet line that cannot run at design capacity or cannot sell its output has a poor cost case.
Seventh, ignoring storage and safety. Wood dust and fine wood waste create fire and explosion risk, and storage of wood fuel creates moisture regain and self-heating risk.
Typical Project Scenario
The following summarizes typical project parameters from wood waste to fuel projects. Specific customer names, locations, and contact details are not included.
Typical project: wood waste to fuel at a sawmill.
Wood waste: softwood sawdust and shavings from pine, fir, and spruce.
Fuel route: pelletizing into fuel pellets for on-site boiler and local market.
Moisture: reduced by drying to the range suitable for pelletizing.
Pellet diameter: 6 to 8 mm.
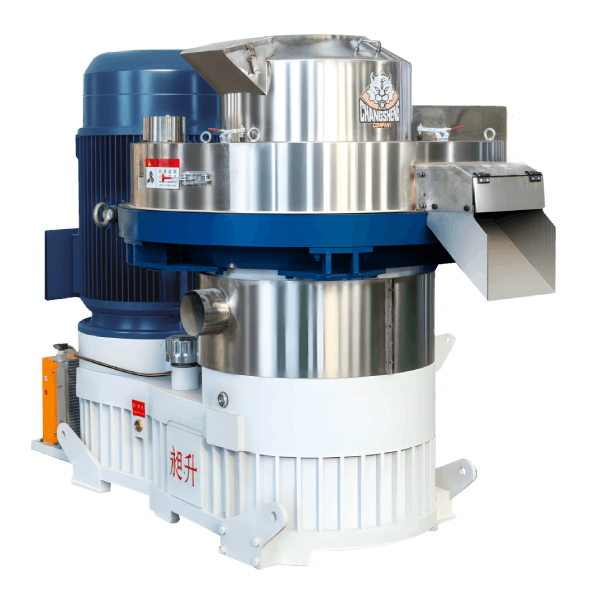
Configuration: ring die pellet machine with hammer mill, dryer, cooler, screener, and packing.
Application: industrial fuel pellets and local fuel market supply.
The parameters above are typical ranges and should be confirmed with actual test records.
What to Confirm Before Choosing a Fuel Route
Confirm wood waste type, species, moisture, particle size, contamination level, treatment status, and waste classification.
Confirm available volume per day, per week, and per year, including seasonal variation where relevant.
Confirm existing or planned combustion equipment and its fuel specification.
Confirm local regulatory requirements for waste classification, air quality, fuel quality, and fire safety.
Confirm market for pellets, briquettes, torrefied fuel, or charcoal, including quality standards.
Confirm power supply, site space, and labor availability.
Confirm capital budget and operating cost tolerance.
Confirm supplier capability for the chosen equipment, including test run and after-sales support.
Confirm inspection and acceptance method for the equipment.
Frequently Asked Questions
What is the best way to convert wood waste to fuel?
There is no single best way. Direct combustion of wood chips, pelletizing, briquetting, torrefaction, and carbonization are different routes with different technical and economic requirements. The right choice depends on wood waste type, treatment status, volume, existing combustion equipment, local market, and regulations.
Can all wood waste be converted to fuel?
No. Clean, untreated wood is usually suitable for fuel. Treated, painted, and glued wood may not be suitable for fuel because of emissions and regulatory requirements. Moisture, particle size, contamination, and waste classification also affect feasibility.
What is the difference between pelletizing and briquetting for wood waste?
Pelletizing produces smaller, denser, more uniform pellets. Briquetting produces larger briquettes and can accept a wider range of particle sizes and moisture. Pellets are usually sold into residential and industrial markets. Briquettes are usually sold into industrial markets.
Can wood chips be burned directly without pelletizing?
Yes. Clean wood chips can be burned directly in some biomass boilers. The boiler must be designed for the chip size and moisture. Pelletizing is required when the fuel must be denser, more uniform, or suitable for markets that require pellets.
What moisture is suitable for wood waste to fuel?
For direct combustion in biomass boilers, wood chips can often be burned in the range of about 20 to 45 percent moisture, depending on boiler design. For pelletizing, target moisture before pelletizing is usually around 10 to 15 percent. For briquetting, moisture requirements are usually between those of chips and pellets. The exact target should be confirmed with a test.
What regulations apply to wood waste to fuel?
Regulations vary by country and region. Key areas include waste classification, air quality, fuel quality standards, fire and explosion safety, transport and storage, and renewable energy incentives. All requirements should be confirmed with the relevant authority and with a qualified advisor.
How much does it cost to convert wood waste to fuel?
Cost depends on the route. Direct combustion cost includes boiler equipment, fuel preparation, and maintenance, offset by avoided fuel purchase. Pelletizing cost includes equipment, drying, grinding, electrical infrastructure, civil works, installation, spare parts, and operating cost, offset by pellet revenue. Cost per ton of fuel is the figure that matters, not equipment price alone. Final cost should be confirmed against a written scope of supply.