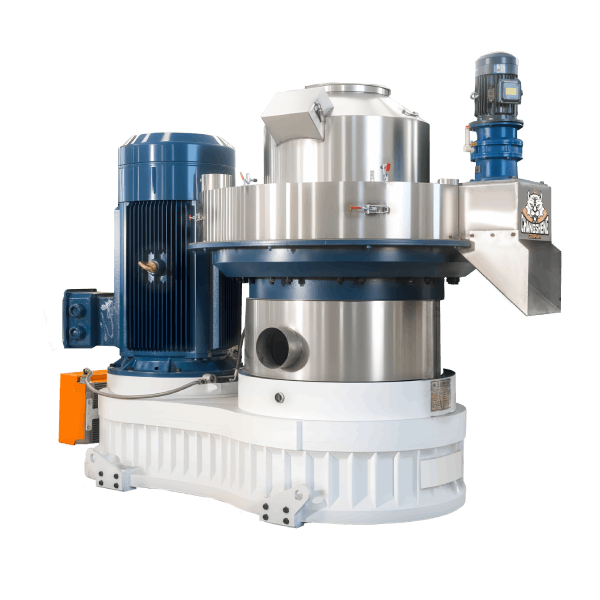
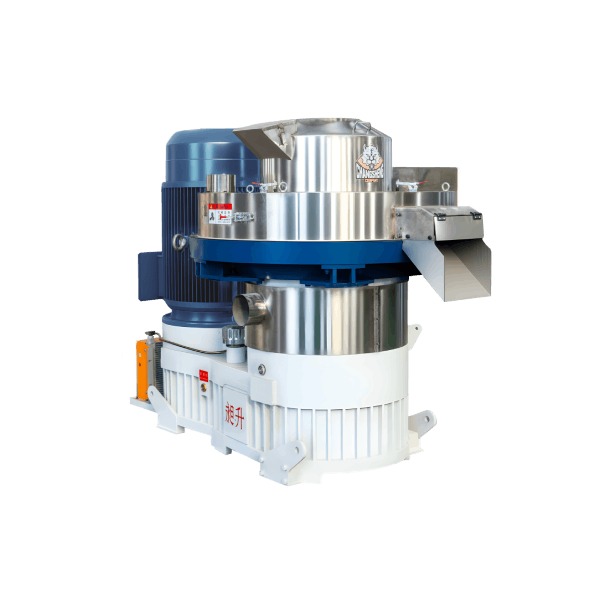
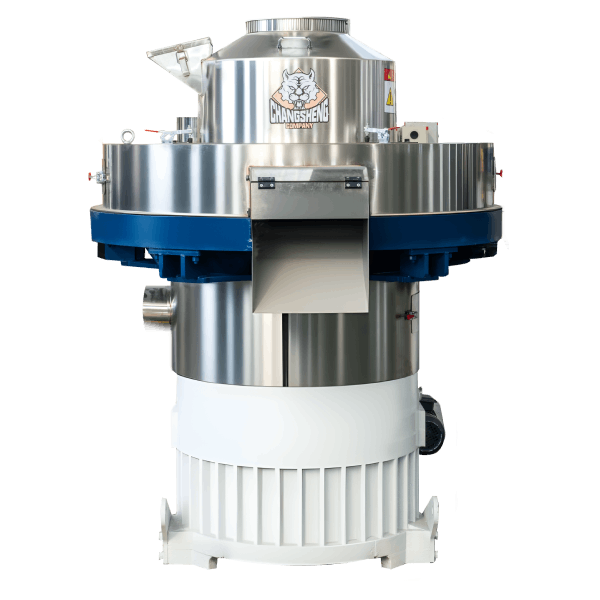
Coconut Husk Rice Husk Pelletizing Machine: Feedstock Differences, Configuration and Procurement
News 2026-09-29
A coconut husk rice husk pelletizing machine is not a single standard product. Coconut husk and rice husk behave differently in a pellet mill because of differences in fiber structure, ash content, silica content, moisture, and bulk density. A machine configured for one may run the other, but not at the same efficiency, die life, or pellet quality.
The practical question for a buyer is not whether one machine can process both materials. The real question is what must be confirmed before ordering, so that the machine runs both feedstocks without unexpected die wear, blockage, or unstable output.
This guide explains the engineering differences between coconut husk and rice husk, how those differences affect die and roller selection, what auxiliary equipment is required, and what to confirm with the supplier before purchase.
Can One Pelletizing Machine Handle Coconut Husk and Rice Husk?
In principle, a ring die pellet machine can process both coconut husk and rice husk. In practice, the configuration is not identical. The die compression ratio, roller shell material, feeder design, moisture control, and dust handling may all need to be adjusted.
There are three common project approaches.
Single feedstock, single configuration. The machine is configured for coconut husk only, or rice husk only. This gives the most stable output and the longest die life for that specific material.
Mixed feedstock, single configuration. The machine is configured for a fixed mix ratio of coconut husk and rice husk. This works when the mix ratio is consistent and the die is selected for the more challenging component.
Alternating feedstock, dual configuration. The machine runs one material at a time, with separate dies and possibly separate feeder settings. This requires more planning and more spare parts, but gives better performance on each material.
The correct approach depends on feedstock supply, mix ratio control, target pellet quality, and how often the material changes.
How Coconut Husk and Rice Husk Differ as Pelletizing Feedstock
Fiber Structure and Bulk Density
Coconut husk is fibrous and bulky. It has low bulk density, which affects feeder design and storage volume. Coconut husk fibers are long and tend to tangle, so shredding and grinding are usually required before pelletizing.
Rice husk is also fibrous but more uniform in particle size. Its bulk density is higher than coconut husk, which improves feeding stability. Rice husk does not usually require shredding, but grinding may be needed depending on target pellet quality.
Because of the difference in bulk density, a feeder designed for rice husk may not feed coconut husk evenly. A feeder designed for coconut husk may overfeed rice husk. This is one of the main reasons a single configuration does not perform equally well on both materials.
Ash and Silica Content
Rice husk is one of the most abrasive biomass feedstocks. It contains high silica content, which accelerates die and roller wear. Coconut husk also contains silica and mineral contamination, but usually at a lower level than rice husk.
Because of this difference, a die and roller configuration that works for coconut husk may wear faster on rice husk. A configuration that works for rice husk may be unnecessarily expensive for coconut husk. The die material and roller shell hardness should be selected based on the material with the higher abrasiveness if the machine will run both.
Ash and silica content vary by origin. Typical ash content for rice husk is often in the range of about 15 to 20 percent, and silica content may be in the range of about 15 to 20 percent of ash. Coconut husk ash content is usually lower, often in the range of about 5 to 10 percent, depending on origin and contamination. These ranges should be confirmed by laboratory test for the specific feedstock, because ash and silica directly affect die and roller selection. This test is one of the most important inputs for die selection.
Moisture Content and Drying Requirement
Fresh coconut husk can have high moisture, depending on storage and processing. Rice husk is usually drier when received from rice mills, but moisture still varies by region and storage condition.
Typical target moisture before pelletizing is around 12 to 15 percent for both materials, but this range depends on feedstock type, die compression ratio, and machine configuration. The exact target should be confirmed with a pelletizing test.
If moisture is above the suitable range, drying is required. Coconut husk often requires drying because of its higher initial moisture, which may be above 30 percent in some storage conditions. Rice husk may not require drying if it is already within range. The exact target should be confirmed with a pelletizing test.
Particle Size and Grinding Requirement
Particle size affects feeding stability, compression, pellet density, and die wear. Coconut husk requires shredding and grinding because of its long fibers and bulky structure. Rice husk is already relatively uniform, but grinding may still be needed to reach the target particle size for the die.
Screen size in the hammer mill determines final particle size. A 4 to 6 mm screen is common for both materials, but the exact size depends on feedstock and target pellet quality.
Die and Roller Selection for Coconut Husk and Rice Husk
Die Compression Ratio
Die compression ratio is the ratio of die hole length to die hole diameter. It determines how much resistance the material meets as it passes through the die. Higher compression ratio increases pellet density but also increases power demand and die wear.
Rice husk usually requires a lower compression ratio than coconut husk in some applications, because its silica content increases die load and wear. Coconut husk, being more fibrous and lower in silica, may tolerate a slightly higher compression ratio to improve pellet density. However, the correct compression ratio depends on feedstock origin, moisture, particle size, and die specification, and should always be confirmed with a pelletizing test. The definition of compression ratio can vary between suppliers, so it should always be confirmed before comparing dies.
Die Material and Heat Treatment
Die material and heat treatment affect die life. For abrasive feedstocks such as rice husk, a die with higher wear resistance is usually required. Common industrial options include case-hardened alloy steel dies and coated dies. The correct choice depends on ash content, silica content, moisture, and target die life.
Expected die life varies widely by feedstock and contamination level. It should be confirmed with the supplier based on similar material and operating conditions, not assumed from a general figure. As a practical reference, die life on rice husk is often shorter than on coconut husk under the same operating conditions, and the cost per ton of pellets is the figure that matters for procurement comparison.
Roller Shell Material and Hardfacing
Roller shells wear with the die. For high-silica feedstocks, roller shells with hardfacing or carbide overlay are commonly used to extend roller life. The roller material and hardness should match the die and the feedstock.
Roller clearance should be checked regularly because abrasive feedstocks change clearance quickly. Incorrect clearance causes uneven wear and unstable pellet quality.
Auxiliary Equipment for a Mixed-Feedstock Line
Magnetic Separation
Magnetic separators remove ferrous metal such as nails, wire, and staples. Metal contamination damages dies and rollers. Double-stage separation is common in commercial lines handling agricultural residues.
Air Classification and Sand Removal
Sand and stones are common in coconut husk and rice husk, especially when material is stored or handled outdoors. Air classification or gravity separation removes heavy particles before grinding and pelletizing. This step extends die life and reduces blockage.
Drying System
Drying reduces moisture to the range suitable for pelletizing. A rotary dryer is commonly used. Drying capacity should be matched to line capacity, not to peak output only. If drying capacity is too small, moisture will vary and pellet quality will fluctuate. If drying capacity is too large, energy cost increases unnecessarily.
Dryer inlet temperature should be controlled to avoid burning the material.
Cooling, Screening, and Packing
Cooling hardens pellets and reduces fines. Screening removes fines and oversize particles. Packing prepares finished pellets for storage or sale. These downstream steps are required for commercial production and for pellets that will be stored or transported.
Dust Collection and Explosion Protection
Coconut husk and rice husk dust is fine and poses both health and explosion risks. Dust collection with high-efficiency cyclone and filters is required. Explosion venting, spark detection, grounding, and where applicable ATEX-rated equipment are recommended for commercial lines. Local regulations should always be confirmed.
Moisture and Particle Size: What to Test Before Ordering
Before requesting a quotation, the buyer should collect the following data:
Feedstock type and mix ratio.
Moisture content as received.
Moisture content after drying.
Ash content.
Silica content, if available.
Particle size distribution.
Bulk density.
Target pellet diameter.
Target capacity.
Operating hours per day or per year.
Available power supply.
This data allows the supplier to recommend a suitable configuration and to state capacity with conditions. A capacity figure without these conditions is not a technical commitment.
Capacity Planning for Coconut Husk and Rice Husk
Capacity is usually expressed in kg/h or t/h. Required hourly capacity equals annual production target divided by annual operating hours. A capacity margin of about 20 to 30 percent is a practical starting point for feedstock variation, moisture changes, and maintenance.
Actual capacity depends on feedstock type, moisture, ash content, silica content, particle size, pellet diameter, die specification, compression ratio, machine efficiency, and operating skill. Rice husk usually produces lower output than coconut husk under the same motor power because of its higher abrasiveness and different fiber structure.
Rated capacity is only meaningful when feedstock, moisture, particle size, and die specification are stated. A capacity figure quoted without these conditions should not be treated as a guaranteed output for your project.
Spare Parts Planning for High-Silica Feedstocks
Dies and rollers are wear parts. Their life depends on feedstock abrasiveness, moisture, compression ratio, and operating conditions. For high-silica feedstocks such as rice husk, die and roller life is usually shorter than for wood-based feedstocks.
A practical spare parts plan for a mixed coconut husk and rice husk project includes at least one spare die, one or two spare roller shell sets, bearings, belts, seals, lubricants, and critical electrical spares such as contactors and relays.
Cost per ton of pellets is the figure that matters, not die price alone. A die that costs more but lasts significantly longer may reduce cost per ton. Expected die and roller life should be confirmed with the supplier based on similar material and operating conditions, not assumed from a general figure.
Procurement Checklist
Before signing a contract, confirm the following with the supplier:
Capacity with stated feedstock, moisture, particle size, and pellet diameter.
Die compression ratio and die material.
Roller shell material and hardness.
Feeder type and whether variable frequency control is included.
Magnetic separation and air classification scope.
Drying system capacity and dryer inlet temperature control.
Cooling, screening, and packing scope.
Dust collection and explosion protection scope.
Motor power, total connected load, voltage, phase, and frequency.
Spare parts list with part numbers and recommended first order.
Warranty scope, wear part definition, and response process.
Inspection and acceptance method before shipment.
Frequently Asked Questions
Can coconut husk and rice husk be pelletized on the same machine?
Yes, but the configuration is not identical. Die compression ratio, roller material, feeder design, and moisture control may need to be adjusted. A single configuration can be used for a fixed mix ratio, but performance will depend on the more challenging component in the mix.
Which material wears dies faster, coconut husk or rice husk?
Rice husk is generally more abrasive because of its higher silica content. Die and roller life is usually shorter on rice husk than on coconut husk. Actual life depends on ash and silica content, which should be confirmed by laboratory test.
Do I need a dryer for coconut husk and rice husk?
Drying is required when moisture is above the suitable range for pelletizing. Coconut husk often requires drying because of higher initial moisture. Rice husk may not require drying if it is already within range. The exact target should be confirmed with a pelletizing test.
What die material is suitable for high-silica feedstock?
For high-silica feedstock such as rice husk, a die with higher wear resistance is usually required. Common industrial options include case-hardened alloy steel dies and coated dies. Roller shells with hardfacing or carbide overlay are commonly used. Expected die life should be confirmed with the supplier based on similar material.
What auxiliary equipment is needed for a mixed-feedstock line?
A complete line may include magnetic separation, shredder, hammer mill, dryer, pellet mill, cooler, screener, packing, and dust collection. Scope depends on feedstock condition and target pellet quality.
How is capacity calculated for a mixed-feedstock project?
Required hourly capacity equals annual production target divided by annual operating hours, plus a capacity margin of about 20 to 30 percent. Actual capacity depends on feedstock type, moisture, ash, silica, particle size, and die specification. Rated capacity is only meaningful when these conditions are stated. A capacity figure quoted without feedstock, moisture, particle size, and die specification should not be treated as a guaranteed output for your project.