Pellet Mill for Carpenter: Small-Scale Selection & Cost Guide
News 2026-09-16
If you run a carpentry shop, you know the routine: every job generates sawdust, shavings, and offcuts. You sweep it up, bag it, and either give it away or pay to have it hauled off. What many carpenters do not realize is that this waste has a measurable energy value—and with the right equipment, it can be converted into pellets that heat your workshop or generate a small income.
This guide is written for carpenters, joinery owners, and small woodworking businesses evaluating whether a pellet mill makes sense. It covers feedstock feasibility, equipment selection, realistic costs, installation, maintenance, and the procurement decisions that determine whether the investment works or becomes a costly mistake.
A note before we begin: this article is written for small-scale operators. If you are running an industrial sawmill or a commercial pellet plant, the scale and economics are different. Here we focus on the carpenter who works with wood every day and wants a practical solution for waste.
Why Carpenters Are Looking at Pellet Mills
The Real Cost of Wood Waste in a Small Shop
Wood waste costs you money in three ways. First, handling and storage consume time and floor space. Second, disposal—whether through a waste service or a trip to the landfill—has a direct cost. Third, and most importantly, you are losing a material that could offset your heating bill or be sold locally.
A one-person carpentry shop processing solid wood can generate 50–200 kg of sawdust and shavings per week, depending on the type of work. A small crew or a shop doing significant planing and milling can generate several hundred kilograms per week. Over a year, that adds up to several tonnes of material with real energy value.
Heating Savings vs Pellet Sales
There are two main ways a pellet mill pays for itself in a carpentry shop:
- Heating your workshop: If you currently heat with oil, gas, or electricity, pellets can displace a significant portion of that cost. The payback is usually faster because you are avoiding retail energy prices.
- Selling pellets locally: Bagged pellets sold to neighbors, farms, or small businesses create income. However, selling requires consistent quality, storage, and some marketing effort.
For most carpenters, heating is the more straightforward path. It uses the pellets directly, avoids quality certification requirements, and produces immediate savings.
When a Pellet Mill Is Not Worth It
A pellet mill is not the right choice for every carpenter. It may not make sense if:
- Your waste volume is very small (under 20–30 kg per week).
- Your waste is mostly MDF, plywood, or treated lumber.
- You have no use for pellets and no local market.
- Your workshop has limited power capacity and no budget for an upgrade.
- You are not prepared to manage moisture, maintenance, and material handling.
Be honest about these constraints. A pellet mill that sits unused is worse than no pellet mill at all.
What Wood Waste Can a Carpenter Actually Pelletize?
Sawdust, Shavings, and Sanding Dust Compared
Not all carpentry waste behaves the same way in a pellet mill. The table below summarizes common materials.
| Material | Pelletability | Notes |
|---|---|---|
| Solid wood sawdust (pine, oak, birch, etc.) | Excellent | Natural lignin acts as binder |
| Planer shavings | Good | Larger particles may need grinding |
| Jointer chips | Good | Consistent size, good for pelletizing |
| Router chips | Good | Consistent size, good for pelletizing |
| Sanding dust | Fair | Very fine; may need blending with coarser material |
| MDF/HDF dust | Not recommended | Resins cause emissions and die wear |
| Plywood dust | Not recommended | Glue content contaminates pellets |
| Treated lumber | Prohibited | Chemical contamination, regulatory violation |
| Mixed sweepings | Not recommended | Contaminants damage dies and reduce quality |
The ideal feedstock is clean, untreated solid wood sawdust and shavings. Segregating waste at the source—keeping MDF and treated wood separate—is the single most effective way to ensure consistent pellet quality.
Materials to Avoid
Some materials should never go into a pellet mill. MDF and HDF contain adhesives that release harmful emissions during pelletizing and contaminate the final product. Plywood dust contains glue that increases die wear and reduces pellet quality. Treated lumber contains chemicals that are regulated in most markets and must not be burned or pelletized.
If your shop works with these materials, you must segregate waste streams. Do not assume that a small amount of contamination is acceptable. Even low levels of MDF dust can accelerate die wear and degrade pellet quality.
The Moisture Challenge for Small Shops
Moisture is the most common reason small-scale pellet operations fail. For wood pellets, the ideal moisture range entering the pellet mill is 12–15% (wet basis). Above 18%, pellets become soft and the mill may choke. Below 10%, the material may not bind properly and die wear increases.
Carpentry shops face a particular challenge because waste moisture varies with the material being processed. Green lumber produces wet sawdust. Kiln-dried lumber produces dry sawdust. If you work with both, you will need to manage moisture variability.
Options for small shops include:
- Natural air drying: Spread sawdust in a covered, ventilated area. Slow but low-cost.
- Blending: Mix wet and dry material to reach target moisture. Requires careful measurement.
- Small batch dryer: Suitable for consistent production but adds capital cost.
- Source segregation: Keep waste from green and dry lumber separate, then blend as needed.
Do not underestimate moisture control. Many small-scale pellet operations fail because the feedstock is too wet or too variable, not because the pellet mill is inadequate.
Flat Die vs Ring Die for Carpenter Workshops
Flat Die: The Default Choice for Small Shops
Flat die pellet mills are the standard choice for carpenters and small woodworking shops. They offer:
- Lower capital cost
- Simpler construction and easier maintenance
- Suitable for capacities under 500 kg/h
- Easier to operate without specialized training
- Compact footprint
Flat die machines have limitations. Die life is shorter than ring die machines, typically 300–600 hours depending on feedstock and operation. Pellet quality can be more variable. Energy consumption per tonne is higher.
For a carpenter producing less than 500 kg/h of pellets, a flat die machine is usually the correct choice.
When Ring Die Becomes Necessary
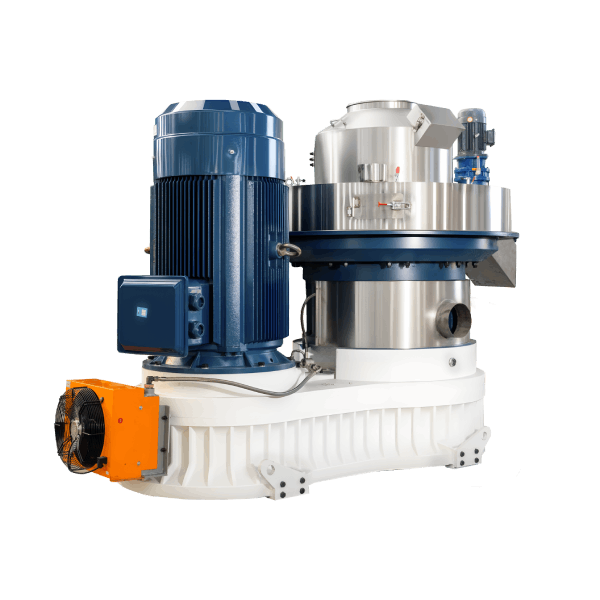
Ring die pellet mills are designed for industrial-scale production. They become necessary when:
- Production exceeds 1 tonne per hour
- Consistent pellet quality is required for sale or certification
- Feedstock is consistent and production runs are long
- Capital budget allows for higher investment and more complex maintenance
For most carpenters, ring die is not the right fit. The capital cost, power requirement, and complexity are difficult to justify at small scale.
Comparison Table
| Factor | Flat Die | Ring Die |
|---|---|---|
| Typical capacity | 0.1–0.5 t/h | 1–20 t/h |
| Pellet quality | Moderate, variable | High, consistent |
| Die life | 300–600 hours | 800–1,500 hours |
| Specific energy | Higher per tonne | Lower at scale |
| Capital cost | Lower | Higher |
| Maintenance complexity | Low | Moderate |
| Best for | Small workshops | Commercial production |
How to Size a Pellet Mill for a Carpenter’s Output
Measuring Your Actual Waste Volume
Sizing begins with your actual waste generation, not your desired output. Follow this sequence:
- Collect and weigh your waste. For one or two typical weeks, bag and weigh all sawdust and shavings. Calculate daily and weekly averages.
- Account for moisture loss. If your waste is at 25% moisture and you dry to 14%, you lose roughly 13% of incoming weight.
- Determine operating hours. A pellet mill running 2 hours per day at 100 kg/h produces 200 kg per day. Running 4 hours produces 400 kg.
- Match capacity to feedstock. Do not size the mill larger than your reliable waste supply. Intermittent operation wastes energy and accelerates wear.
- Add a margin. A 10–15% capacity buffer accommodates variability and maintenance downtime.
Power Supply Constraints
Pellet mills require significant electrical power. A small flat die machine may need 7.5–30 kW, depending on capacity. Confirm your workshop’s electrical supply can handle the connected load, including the pellet mill motor, any hammer mill, and auxiliary equipment.
If your power supply is limited, you may need to:
- Operate the pellet mill during off-peak hours
- Upgrade your electrical service
- Choose a smaller machine with lower power demand
- Use a diesel-powered option if grid power is unavailable
Do not overlook this step. Electrical upgrades can be expensive and time-consuming.
Common Sizing Errors
- Sizing for peak waste generation, not average. Carpentry waste fluctuates with project type. Size for reliable average, not best-case peak.
- Ignoring moisture variability. A mill sized for dry sawdust will struggle with green or wet material.
- Underestimating power requirements. Confirm the actual connected load, not just the pellet mill motor.
- Forgetting about storage. Pellets need protected storage. Fines and moisture degrade quality quickly.
- Overlooking labor. Small-scale pellet production still requires operator attention, material handling, and maintenance.
Complete Small-Scale Setup
Process Flow for a Carpenter Shop
The standard process flow for a small-scale pellet operation is:
Waste collection → Storage → Grinding (if needed) → Moisture adjustment → Pellet mill → Cooling → Screening → Storage/Bagging
Each stage has a defined function. Skipping or undersizing any stage creates a bottleneck that limits real output.
Drying Without Expensive Equipment
Drying is often the most challenging part of a small-scale pellet operation. Options for carpenters include:
- Natural air drying: Low cost but slow and weather-dependent. Suitable for small volumes and dry climates.
- Small rotary dryer: Heated by gas, biomass, or waste wood. Suitable for consistent production.
- Blending: Mixing wet and dry material to reach target moisture. Requires careful measurement and mixing.
For many carpenters, a well-designed air drying system or simple blending is sufficient. The key is to ensure consistent moisture entering the pellet mill.
Cooling, Screening, and Storage
Freshly made pellets are hot (70–90°C) and soft. They must be cooled before storage or bagging. A simple counter-flow cooler or perforated tray system can work for small volumes. Screening removes fines and oversize particles; fines can be recycled into the next batch.
Bagging can be manual for small operations. For larger volumes, a semi-automatic bagging system improves efficiency and reduces labor.
Investment and Payback for a Carpenter
CAPEX Breakdown
Capital cost for a small-scale pellet operation varies widely. As a general reference for a 100–300 kg/h line:
| Item | Approximate Share |
|---|---|
| Pellet mill | 30–40% |
| Hammer mill (if needed) | 5–10% |
| Dryer (if needed) | 15–25% |
| Cooler and screener | 5–10% |
| Conveyors and feeding | 5–10% |
| Electrical and control | 5–10% |
| Installation and commissioning | 10–15% |
These are indicative ranges. Actual costs depend on specifications, local labor, import duties, and freight.
OPEX Breakdown
Operating cost per tonne of pellets typically includes:
- Electricity: The largest single cost. Wood pelletizing consumes roughly 80–120 kWh per tonne, depending on feedstock and equipment efficiency.
- Thermal energy for drying: If you use gas or biomass, this is significant. Using your own waste wood as fuel can reduce this cost.
- Labor: A small carpentry shop line may need 1 operator, depending on automation.
- Wear parts: Dies and rollers are the main consumables. Die life varies with feedstock, moisture, and operation.
- Maintenance: Bearings, belts, screens, and lubrication.
Payback Calculation Example
Assume a carpenter produces 100 tonnes per year of dry sawdust and shavings. After processing, yield is approximately 90 tonnes of pellets.
If pellets are used for heating and displace $200/tonne of heating oil, the annual savings are $18,000. If operating cost is $60/tonne, the net savings are $12,600 per year. If total capital investment is $40,000, simple payback is approximately 3.2 years.
If pellets are sold instead of used, the calculation changes. At $150/tonne, gross revenue is $13,500. After operating costs of $5,400, gross margin is $8,100. Payback is approximately 4.9 years.
The self-supply model usually offers faster payback because you are displacing retail energy prices.
Key Technical Parameters for Small Pellet Mills
Motor Power, Die Size, and Compression Ratio
- Motor power: Must match the die and feedstock. Undersized motors stall; oversized motors waste energy. For a 100–300 kg/h flat die machine, typical motor power is 7.5–30 kW.
- Die diameter and compression ratio: The ratio of die hole length to diameter. Higher ratio increases pellet density but also energy consumption and die wear. For wood pellets, compression ratios of 1:5 to 1:8 are common.
- Die speed: Affects pellet quality and throughput. Higher speed increases capacity but may reduce density.
These parameters must be specified together. A pellet mill is not a commodity—it is a system that must be matched to your material and production targets.
Die and Roller Material
Dies are typically made from alloy steel or stainless steel. For wood pellets, hardened alloy steel with proper heat treatment offers the best balance of wear life and cost. Rollers should be matched to the die material and surface hardness.
Ask the supplier for material certificates and hardness test reports. This is a standard procurement practice for industrial equipment.
Safety and Compliance
Depending on your location, the equipment may need to comply with:
- CE marking (European Union)
- UL or CSA standards (North America)
- Local electrical codes
- Dust hazard classification (if applicable)
Confirm compliance requirements before purchase. Retrofitting for compliance is expensive and delays commissioning.
Installation and Workshop Integration
Space, Dust, and Noise
A small pellet mill (100–300 kg/h) typically requires 20–80 m² of covered space, depending on configuration and storage needs. Allow access for maintenance, material handling, and pellet storage.
Dust collection is essential for safety, environmental compliance, and housekeeping. Noise levels vary by machine type and can exceed 85 dB. Hearing protection and sound enclosure may be required.
Commissioning Checklist
- Foundation and anchor bolt drawings approved
- Power supply capacity confirmed
- Dust collection ductwork planned
- Material handling access clear
- Spare parts and tools on site
- Operator training scheduled
Maintenance and Troubleshooting
Daily and Weekly Checks
- Daily: Inspect die and rollers, check lubrication, monitor motor current, verify moisture.
- Weekly: Check belts, bearings, screens, and dust collection.
- Monthly: Inspect gearbox oil, coupling alignment, and electrical connections.
Wear Parts and Replacement
- Die: Replace when pellet quality drops, energy consumption rises, or visible wear exceeds limits.
- Rollers: Replace when surface wear reduces pellet density or throughput.
- Bearings: Monitor temperature and vibration. Replace at first sign of failure.
Common Problems and Fixes
- Pellets too soft: Check moisture, die compression ratio, and feedstock particle size.
- Machine choking: Reduce feed rate, check moisture, inspect die holes for blockage.
- Excessive die wear: Verify feedstock cleanliness, moisture, and compression ratio.
- High fines: Check cooler operation, screener condition, and pellet durability.
Most early-stage issues trace back to moisture control, feedstock consistency, or incorrect operating parameters. Supplier technical support is critical during this phase.
How to Evaluate a Pellet Mill Supplier
Questions to Ask
- What is the rated capacity for wood sawdust?
- What die and roller material are used?
- What is the expected die life for my feedstock?
- What is the warranty and spare parts pricing?
- What technical support is available after purchase?
- Can you provide references from similar small-scale installations?
Test Reports and Sample Validation
Before purchase, request:
- Material test report for die and roller
- Performance test data for similar feedstock
- Sample pellets produced from your material
- Warranty terms and spare parts pricing
After-Sales Support
Confirm:
- Installation and commissioning support
- Operator training availability
- Remote troubleshooting capability
- Spare parts delivery time
- Response time for technical issues
A supplier who cannot provide these is a risk, regardless of price.
Case Study: Carpenter Shop in Northern Europe
Project Background
A one-person carpentry shop in Northern Europe producing custom furniture and built-in cabinetry faced rising heating costs and sawdust disposal fees. The shop generated approximately 80 tonnes per year of mixed hardwood and softwood sawdust and shavings.
Configuration and Results
The installed line included a small hammer mill, a simple air drying system, a flat die pellet mill (150 kg/h), a counter-flow cooler, and manual bagging. Feedstock was dried to 14% moisture and pelletized without binders.
Results after one year:
- Pellet output: approximately 70 tonnes per year
- Pellets used for workshop heating, displacing heating oil
- Annual savings: approximately €12,000
- Payback period: 3.1 years
- Disposal cost eliminated
Lessons Learned
- Moisture control was the most critical factor for consistent pellet quality.
- Segregating waste streams improved pellet quality and reduced die wear.
- A simple air drying system was sufficient for the shop’s volume.
FAQ
Can I pelletize sawdust directly from my carpentry shop without drying?
No. Most sawdust from green or semi-dry lumber is too wet for direct pelletizing. Drying to 12–15% moisture is almost always required.
What is the minimum capacity for a pellet mill in a one-person carpentry shop?
For self-supply heating, 50–100 kg/h can be viable. For selling pellets, 200–300 kg/h is generally the minimum for commercial viability.
How long does a pellet die last in a small pellet mill?
Die life varies with feedstock, moisture, and operation. For wood pellets in a flat die machine, 300–600 hours is typical.
Can I pelletize MDF or plywood dust?
No. MDF, HDF, and plywood contain adhesives and resins that cause emissions, increase die wear, and contaminate the final product.
What certifications should I look for?
CE for Europe, UL or CSA for North America, and ISO 9001 for quality management. Confirm requirements for your market.
How much space does a small pellet mill need?
A 100–300 kg/h line typically requires 20–80 m², including storage and access.
What is the biggest mistake carpenters make when buying a pellet mill?
Underestimating moisture control and feedstock preparation. The pellet mill is only one part of the system; the upstream and downstream equipment must be sized correctly.
About the Author
This article was prepared by the engineering and international trade team at Shandong Changsheng Machinery Co., Ltd. With over a decade of experience in biomass pelletizing equipment, the team has supported carpenters, joinery shops, sawmills, and pellet producers across Europe, Southeast Asia, and the Americas. Our engineers specialize in feedstock assessment, equipment selection, line configuration, and commissioning support for small to industrial-scale pellet production. The company provides flat die and ring die pellet mills, complete pellet lines, and technical consulting for international clients.
CTA:
If you are evaluating a pellet mill for your carpentry shop and want a technical assessment based on your actual waste stream and heating needs, contact our engineering team to request a preliminary configuration and budgetary estimate. We can also arrange a video factory tour and provide reference installations in your region.