Corn Stover Pellet Mill: Equipment Selection and Production Process
News 2026-07-28
Corn stover is the stalks, leaves, husks, and cobs left in the field after corn harvest. It is one of the most abundant agricultural residues in the world, and it is also one of the more awkward feedstocks to pelletize. The material is bulky and fibrous, it carries soil and stones from the field, its ash and silica content are high, and its lignin content is lower than wood, so it does not bind as readily under pressure.
This page is written for project developers and procurement teams who need to answer a practical question: how do you turn corn stover into pellets that meet a buyer’s specification, with equipment that will run reliably? It focuses on raw material preparation, pellet mill selection, production line configuration, and the cost factors that actually move a project. Shandong Changsheng Machinery works with agricultural residue projects of this type, and the guidance below reflects how those lines are configured and where projects typically go wrong.
What is corn stover biomass?
Corn stover is the above-ground residue left after the grain is harvested. It is usually described as a mix of stalks, leaves, husks, and cobs. Published proportions such as stalks at 40–60 percent, leaves at 15–25 percent, husks at 10–15 percent, and cobs at 10–15 percent are reference ranges only. The actual mix depends on the corn variety, the combine settings, how much stubble is left in the field, and which fractions are collected. For project planning, the composition should be measured on the material you will actually receive.
Corn stover is not wood. Its lignin content is generally lower, its ash content is generally higher, and it usually carries more silica and field contamination. Those differences drive most of the equipment decisions in a stover line. Comparing corn stover with wood is useful for orientation, but published comparison tables should be treated as indicative rather than as specifications for your project.
Corn production figures, stover yield figures, collectable residue figures, and the volume actually available as a commercial feedstock are four different numbers. National corn output does not translate directly into usable stover, because collection rates, competing uses such as animal bedding and soil retention, and the economics of baling all reduce the amount that reaches a plant. For procurement purposes, the relevant figure is the stover you can contract within an economic transport distance, not an industry total.
Challenges of corn stover pelletizing
Long fibers and feeding problems. Stalks and leaves are long and stringy. They bridge in hoppers, wrap around shafts, and feed unevenly into the mill. Uneven feed destabilizes die temperature and produces inconsistent pellet quality, so feeding is a design issue, not an operating detail.
High ash and silica content. Corn stover carries soil from the field and silica in the plant structure. Both accelerate wear on dies, rollers, and hammer mill parts, and both raise the ash content of the finished pellet. Ash is the main quality constraint for stover pellets in markets with strict limits.
Moisture and binding challenges. Stover moisture at collection varies widely with weather and harvest timing. The moisture level at the die affects binding, and because stover binds less readily than wood, the workable moisture window is narrower and the die specification matters more.
Raw material contamination. Soil, stones, and metal can enter with the bales. A stover line needs cleaning and destoning ahead of the grinder, or the grinder and the pellet mill will pay for it in wear and downtime.
Corn stover pre-processing requirements
Baling and collection. Stover is normally baled to make transport practical. Bale type, density, and moisture at baling affect everything downstream, and collection logistics often set the practical limit on plant size. The harvest window is short, so storage capacity and covered storage need to be planned alongside the process equipment.
Cleaning and shredding. Bales are broken up and the material is cleaned of soil and stones before size reduction. A destoner or similar cleaning stage is not optional in most stover projects. Shredding then reduces the bales to a size the dryer and grinder can handle.
Drying and moisture control. Drying is required when the incoming moisture is above what the die can work with, which depends on the bale moisture and the season. A rotary dryer is common; the sizing basis should be the actual incoming moisture range and the target moisture at the die, not an average. The moisture target at the die should be established by testing the actual stover rather than taken from a table. A reference range is sometimes quoted around 12–15 percent at the die, but this is a starting point for trials, and the correct value depends on the die, the pellet diameter, the fiber condition, and whether additives or conditioning are used.
Grinding and particle size. A hammer mill reduces the dried material to a particle size the die can accept. Final particle size should be matched to die hole diameter and confirmed in trial production. Over-grinding raises energy cost and can make feeding worse; under-grinding leaves long fibers that bridge and blind. The right target is the one that feeds steadily and forms a durable pellet on your die. Grinding also affects throughput indirectly: finer, more uniform material generally feeds more steadily and supports higher output, while coarse or variable material reduces effective capacity and raises the risk of blocking, even though the mill itself has not changed.
Corn stover pellet production process
A complete stover line typically runs through baling and reception, bale breaking and cleaning, shredding, drying where required, grinding, mixing and conditioning where used, pelletizing, cooling, screening, and storage or packaging.
Configuration is not identical for every project, and incoming moisture is the main reason. A line receiving wet stover in a humid climate needs enough drying capacity to handle the wet end of the range, and the dryer, not the pellet mill, becomes the throughput bottleneck when moisture is high. A line receiving dry bales may be able to reduce or skip thermal drying and direct capital toward cleaning, grinding, and dust control instead. A line receiving a mix of wet and dry bales needs storage and blending flexibility so the dryer is not sized for the worst case and then idle for most of the year. Where stover is blended with wood or another residue, a mixing stage is added and the die specification is set for the blend rather than for stover alone. Shandong Changsheng Machinery configures stover lines around the actual incoming moisture, the target output, the pellet diameter, and the site conditions, rather than around a standard equipment list.
How to choose a corn stover pellet mill
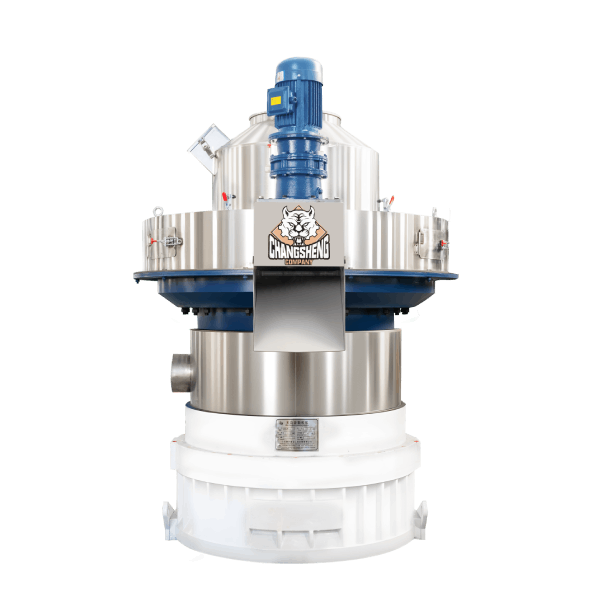
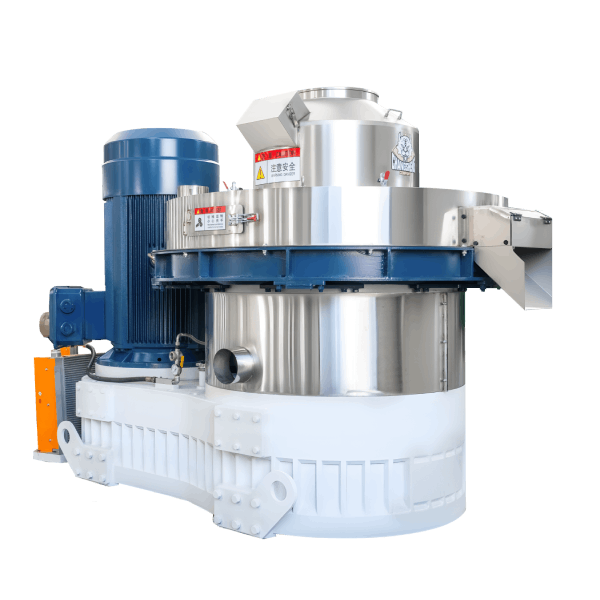
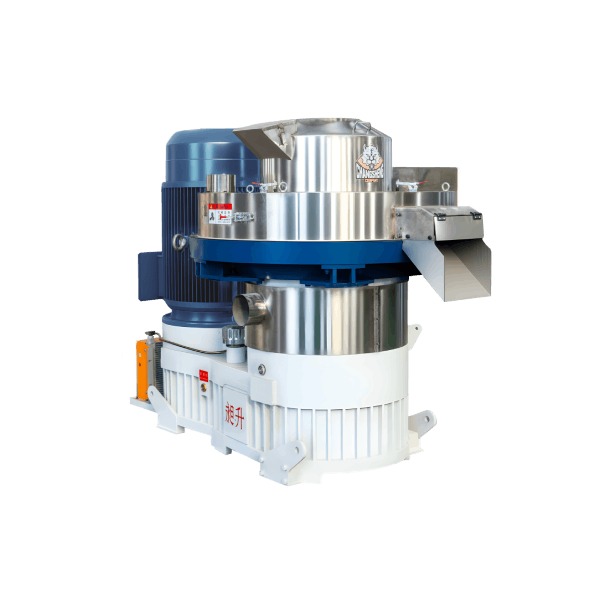
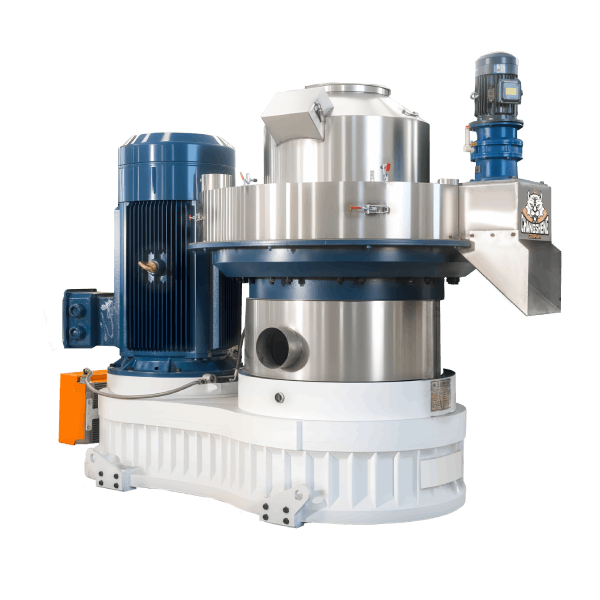
Motor power and production capacity. Motor power does not determine output by itself. Real capacity depends on the feedstock, its moisture at the die, fiber condition, pellet diameter, die specification, and how steadily the line is fed. A mill rated at a given capacity on wood will not deliver the same figure on stover. Ask for capacity to be stated against a defined feedstock and moisture, and expect the figure to be confirmed in trial production. Where a supplier quotes capacity, confirm whether it refers to raw material throughput or finished pellet output. Blending stover with wood changes the practical capacity again, because the blend binds differently and feeds differently from either material alone, so a capacity figure quoted for pure stover should not be assumed to hold for a blend.
Ring die and roller configuration. Die material, hole diameter, open area, and compression ratio all need to match the stover being run. The ring die compression ratio should be selected according to corn stover characteristics, moisture content, pellet diameter, and actual trial results. It should not be treated as a universal specification, and it should not be derived from lignin content alone. Abrasion-resistant die and roller materials are relevant because of silica and soil contamination, but the specific grade should be chosen against actual wear conditions rather than adopted as a blanket standard.
Feeding and conditioning system. Because stover is bulky and stringy, stable feeding is critical. Whether a force feeder or assisted feeding is needed depends on the bulk density of the material and on trial results with the specific mill. Conditioning with heat or steam can improve binding, but the need for conditioning, the temperature, and the settings depend on the material and the mill and should be confirmed in trials rather than assumed.
Wear resistance and maintenance. Stover wears parts faster than clean wood. Die and roller life, hammer mill component life, and the spare parts plan should be discussed at the quotation stage. A buyer who has not planned for wear parts will see unplanned downtime early in production.
Corn stover pellet quality and applications
Pellet quality should be described through test parameters rather than fixed promises. The relevant tests are moisture content, ash content, calorific value, bulk density, pellet durability, and pellet diameter and length. Published ranges for stover pellets often place calorific value around 15–17 MJ/kg and ash at roughly 5–10 percent, with durability and bulk density varying with the line and the material. These are indicative and should be confirmed by laboratory testing on pellets made from your stover.
Ash is the main quality constraint. Stover pellets suit industrial combustion and power generation, including co-firing, where ash handling is available. They are a poor fit for residential heating where ash limits are strict. Blending with wood or other low-ash material can improve binding and reduce ash, and screening removes some fines and dirt, but neither is a substitute for a specification that matches the end market.
Corn stover pellet production line cost factors
Project cost in a stover line is driven by collection logistics and pre-processing more than by the pellet mill itself. The main cost elements are stover collection, baling, and transport, reception and storage, bale breaking and cleaning, shredding, drying system and its heat source, grinding, mixing and conditioning where used, the pellet mill and its die and roller configuration, cooling, screening, dust collection, storage and packaging, civil works, and electrical infrastructure. Collection distance and bale price can dominate the operating economics, and drying energy is the largest process cost when drying is required.
Investment is best built from a defined scope rather than quoted as a generic range. A developer should ask for a quotation that states the equipment scope, the capacity basis, the dryer sizing basis, the die specification, and the acceptance test, and should compare quotations on that basis rather than on headline price.
A payback period should not be quoted without a full cost and revenue model. It depends on the stover cost and collection distance, the equipment investment, the pellet selling price in the target market, the capacity utilization, and the cost of energy and labor. The practical approach is to build the model with local figures for each of these inputs and to test how sensitive the result is to the two or three that carry the most uncertainty.
How to select a corn stover pellet machine supplier
Corn stover is not a feedstock where general biomass experience transfers automatically. A supplier should be able to explain how they would handle the long fibers, the ash and silica, the contamination, and the moisture variation, and should be willing to test your material rather than quote from a catalog. Ask whether the supplier has experience with stover or comparable agricultural residues, whether they can supply the complete line rather than the pellet mill alone, and how they will confirm capacity and pellet quality before shipment. A supplier who cannot describe the cleaning, grinding, and feeding stages in detail is a warning sign worth taking seriously, because those stages decide whether a stover line runs steadily.
Frequently asked questions
Can corn stover be pelletized? Yes, but it requires cleaning, grinding, and often drying before pelletizing, and it usually needs a die specification and sometimes additives that differ from wood. It is more demanding than wood and generally less demanding than high-silica straws such as rice straw.
Why is corn stover difficult to pelletize? The main reasons are long and stringy fibers that feed unevenly, high ash and silica that increase wear and lower pellet quality, moisture variation at collection, and soil and stone contamination from the field.
Are corn stover pellets suitable for residential heating? Generally not. The higher ash content makes them a poor fit for most residential stoves. They are better suited to industrial boilers and power generation with ash handling.
What should I test before choosing a pellet mill for stover? Test your actual stover for moisture range, ash and silica content, and contamination level, and run trial production on the proposed die to confirm capacity and pellet durability. Published parameters are a starting point, not a substitute for your own test results.
How does corn stover compare with wheat straw for pelleting? Corn stover generally has slightly higher lignin and lower silica than wheat straw, so it is often somewhat easier to pelletize, but it is still significantly more challenging than wood.
Is corn stover pelleting economically viable? It can be, where stover is available at low cost within a short collection distance and there is a market for industrial-grade pellets. Viability depends on collection logistics, drying energy, pellet price, and realistic output, and should be assessed with a project-specific cost model rather than a generic estimate.