Pellet Mill Motor Trips Repeatedly: Causes, Diagnosis and Fixes
News 2026-11-17
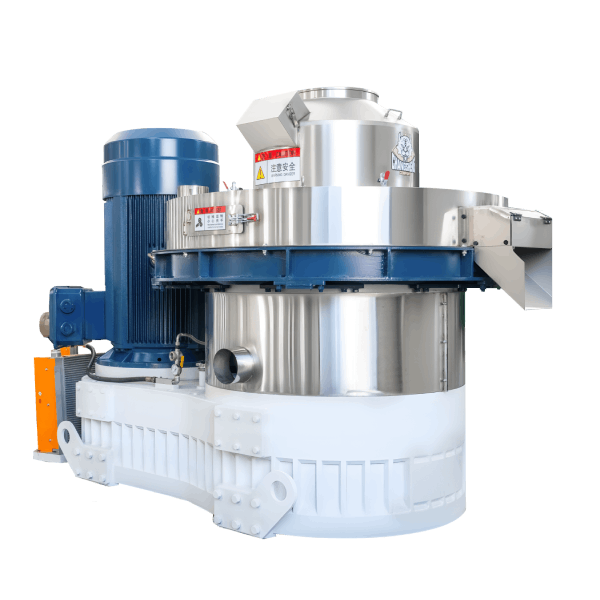
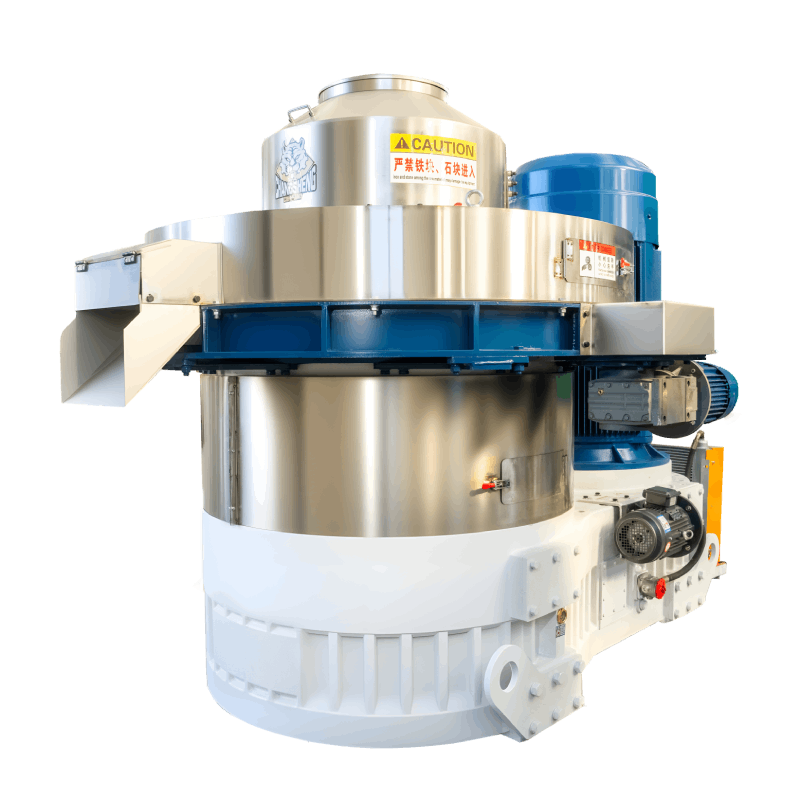
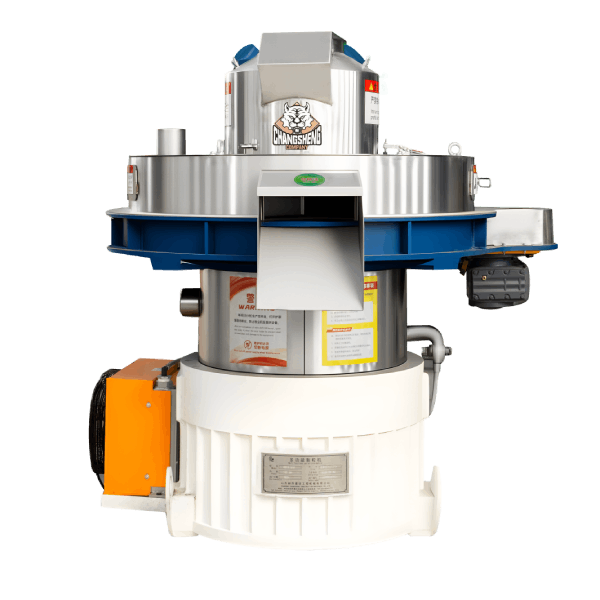
A pellet mill motor that trips repeatedly is protecting itself from something. The trip is not the fault; it is the motor’s response to an overload, a supply problem or a protection setting that is wrong for the machine. Resetting the breaker and restarting without finding the cause is what turns a correctable fault into a burnt motor or a damaged drive.
The cause is usually one of five things: a mechanical overload in the mill, a material problem that raises the load, a supply or electrical fault, a protection setting that is too tight for the application, or a motor or drive fault. Which one it is decides the fix, and the first step is to note exactly when the trip happens: at startup, under load, after a period of running, or at random.
This article covers how to tell those cases apart, the electrical and mechanical causes, the diagnostic sequence, what the trip record tells you, the safety procedure for working on the electrical side, and what to confirm when buying a mill.
What the Trip Pattern Tells You
The moment the trip happens narrows the cause before any measurement is taken.
| Trip pattern | Likely area | What to check first |
|---|---|---|
| Trips immediately on startup, before material is fed | Electrical, protection setting, or mechanical jam | Supply voltage, protection setting, free rotation of the mill |
| Trips under load, after a period of normal running | Mechanical overload or material problem | Feed rate, material moisture, die condition, roller gap |
| Trips at random, with no clear pattern | Supply fault, loose connection, intermittent protection | Supply quality, terminals, protection device |
| Trips after a specific change | The change itself | What was changed — die, roller, material, electrical work |
| Trips with high current before the trip | Genuine overload | The mechanical and material causes below |
| Trips with normal current before the trip | Protection or supply fault | Protection setting, supply, motor winding |
The current reading before the trip is the single most useful piece of information. A trip with high current is an overload; a trip with normal current is a protection or supply fault. If the panel records current, read it before resetting.
Mechanical Overload
A mechanical overload is the most common cause of repeated tripping, and it is the one that is most often a symptom of a different problem.
Material moisture
Wet material raises the load because it compresses but does not flow through the die. The mill works harder for the same output, and the current rises until the protection trips.
Feed rate too high
More material than the die can consume backs up in front of the rollers, raises the load and trips the motor. This often follows a change in material bulk density, which changes the mass flow at the same feeder setting.
Die condition
A die with blocked holes, or a die whose holes have worn, changes the load. Blocked holes reduce open area and raise the load; worn holes can lower it. Either way, a die that has changed since the last good run should be checked.
Roller gap
A roller gap that is too small over-compresses the material and raises the load without a matching output gain. A gap that is uneven loads the mill unevenly and can trip on one station.
Foreign matter or a jam
A foreign object, or material packed between roller and die, can lock the mill and trip the motor immediately on startup.
Bearing or drive fault
A failing bearing or a drive fault adds load to the motor. This is usually accompanied by noise, heat or vibration, and is a separate diagnosis.
Electrical and Protection Causes
Supply voltage
Low supply voltage raises the current for the same load, and can trip the motor. High voltage stresses the insulation. The supply should be measured at the motor terminals under load, not only at the panel.
Protection setting
A protection device set too tight for the application trips on normal load. A device set too loose does not protect the motor and allows damage. The setting should match the motor’s rated current and the manufacturer’s specification, and should be verified after any motor or drive change.
Loose or corroded connections
A loose terminal or a corroded connection increases resistance and heat, and can cause intermittent trips. The terminals at the motor and at the protection device should be checked and tightened to specification.
Motor winding fault
A motor with a winding fault draws high current, runs hot and trips. Winding insulation resistance and winding resistance should be measured by a qualified electrician.
Protection device fault
The protection device itself can fail and trip at the wrong current. The device should be tested, or replaced with a known good unit, before the motor is assumed to be at fault.
Diagnosing Repeated Trips
Work through these steps. The electrical steps should be done by a qualified electrician.
- Record the trip pattern. At startup, under load, at random, or after a change. Record the current at the moment of the trip if the panel shows it.
- Check the mechanical side first. With the mill isolated and locked out, confirm the mill turns freely by hand. A mill that does not turn freely has a mechanical jam and should not be restarted.
- Check the material. Moisture, particle size and feed rate against the specification. Wet material and a high feed rate are the two most common causes.
- Check the die and rollers. Blocked holes, uneven wear, and the roller gap on every station.
- Check the supply voltage at the motor terminals under load, by a qualified electrician.
- Check the protection setting against the motor’s rated current and the manufacturer’s specification.
- Check the terminals and connections for tightness and corrosion.
- Check the motor winding insulation resistance and winding resistance if the mechanical and supply checks are clear.
- Check what changed. A die change, a roller change, a material change, electrical work or a protection setting change explains most sudden trips.
If the trip continues with the mechanical side clear, the supply correct and the protection setting correct, the motor or the protection device is the likely cause.
Safety on the Electrical Side
Electrical diagnosis carries risks that mechanical diagnosis does not.
- Isolate and lock out before working on the motor or the protection device. Confirm zero energy at the motor terminals.
- Electrical work should be done by a qualified electrician, following the site’s electrical safety procedure.
- Do not bypass or increase a protection setting to stop the tripping. The protection is doing its job; bypassing it allows the motor to overheat and fail.
- Do not reset a tripped breaker repeatedly. Each reset applies a high current to a motor that may already be hot.
- Allow the motor to cool before restarting after a trip, because a hot motor has a lower tolerance for the next overload.
- Check the motor temperature before restarting. A motor that is hot to the touch after a trip should be left to cool, not restarted.
What the Trip Record Tells You
A written trip record turns a repeating fault into a diagnosable one.
| Record item | Why it matters |
|---|---|
| Time and date of each trip | Shows whether the trips are increasing in frequency |
| Operating condition at the trip (startup, load, material) | Narrows the cause |
| Current before the trip | Distinguishes overload from protection fault |
| Motor temperature after the trip | Indicates whether the motor is overloaded or the protection is too tight |
| Material type and moisture at the time | Links the trip to a material change |
| What was changed since the last good run | Links the trip to a recent change |
| Action taken after the trip | Shows whether the fix worked |
The record is also what a supplier or an electrician needs in order to help, because it shows the pattern rather than a single event.
Ring Die and Flat Die Differences
The causes are similar on both machine types, but the drive arrangement differs.
| Cause | More common on ring die mills | More common on flat die mills |
|---|---|---|
| Mechanical overload from material | Common | Common |
| Die condition | Common | Common |
| Roller gap | Common | Common |
| Gearbox or main shaft fault | Common | Less common |
| Belt drive fault | Less common where the drive is by gearbox | More common where the drive is by belt |
| Motor or protection fault | Common | Common |
On both types, confirm the actual drive arrangement on the specific machine before deciding where to look first.
When Repeated Trips Signal a Wrong Selection
Repeated trips with material that should be within the mill’s capability, and with the mechanical and electrical checks clear, point to selection.
Signs that point to selection:
- The motor power is marginal for the material at the required throughput.
- The die specification does not match the material, so the mill works harder than it should.
- The feeder cannot control the feed rate finely enough for the material.
- The supply capacity at the site is below the motor’s starting or running demand.
- The protection setting cannot be made to suit both the motor and the actual load.
In these cases, the motor, die, feeder or supply specification needs review against the material and the site, not repeated adjustment.
Preventing Repeated Trips
- Keep a trip record, and review it when the trips increase in frequency.
- Control material moisture and feed rate within the specification.
- Check the die and roller gap at each shift or at the interval the manufacturer specifies.
- Check the protection setting after any motor or drive change, and verify it against the motor rating.
- Check terminals and connections at scheduled maintenance.
- Measure supply voltage under load at intervals, and investigate any change.
- Train operators not to reset a tripped breaker repeatedly, and to record the trip instead.
Spare Parts Planning
- Protection devices. A spare protection device allows a suspected faulty unit to be swapped and tested.
- Motor terminals and connections. These are inexpensive and a common cause of intermittent trips.
- Belts, where fitted. A worn belt can slip and cause the motor to run at the wrong load.
- Motor bearings. These wear and can add load, particularly on older motors.
What to Confirm When Buying a Mill
Motor rating against the material. Confirm the motor power is adequate for your material at the required throughput, not only for the rated capacity on a favourable material.
Supply requirement. Confirm the supply voltage, frequency and starting current the mill needs, and confirm your site can provide them.
Protection specification. Confirm the protection device type and setting, and that the setting is documented.
Trip record at acceptance. Confirm the mill is run with your material at the intended feed rate, and that current and any trips are recorded.
Documentation. Confirm the electrical drawings, the motor data sheet and the protection setting are handed over, because they are needed for future diagnosis.
If a pellet mill motor is tripping repeatedly and the cause is not clear from the checks above, send the machine model, the trip pattern, the current before the trip, the material condition and what changed before the trips started, and the motor, protection and mechanical condition can be reviewed against the machine.
AUTHOR / COMPANY INFORMATION
Shandong Changsheng Machinery Co., Ltd. is a manufacturer of biomass pellet production equipment, including ring die pellet mills, complete pellet lines and related process equipment, serving overseas importers, EPC contractors, engineering companies and biomass fuel producers.