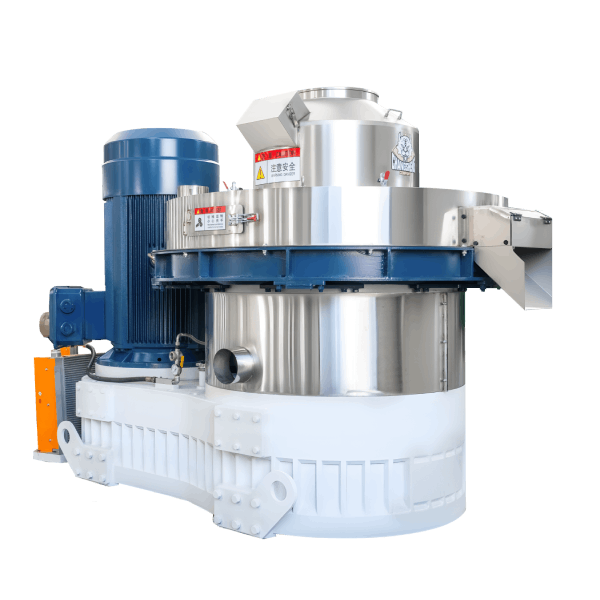
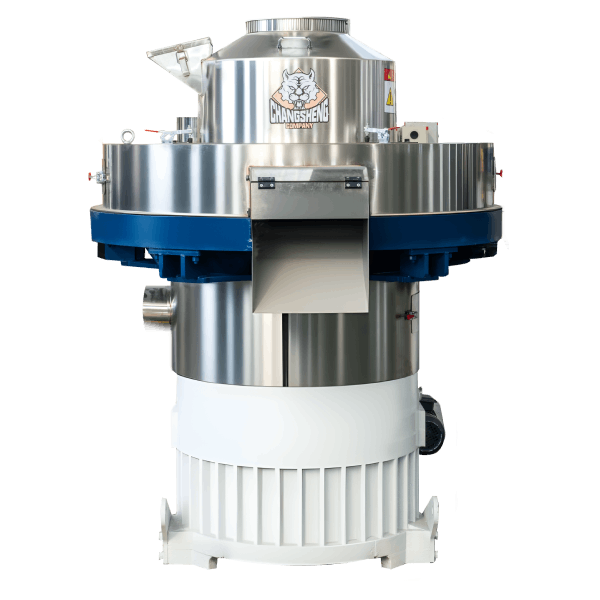
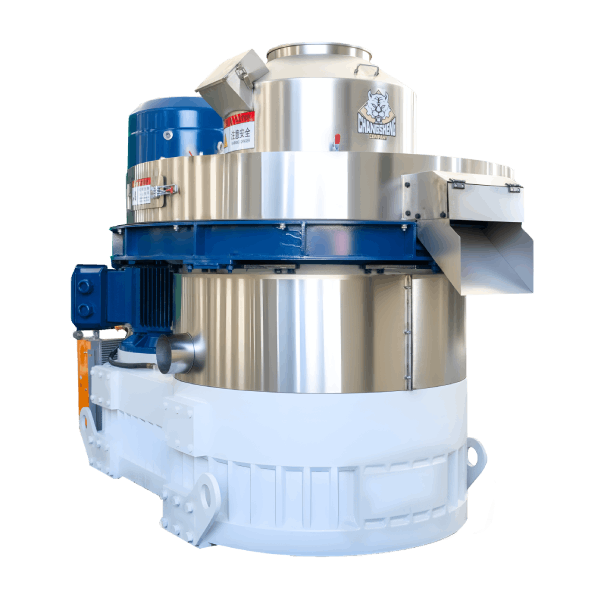
Jute Stick Pellet Machine: Process, Equipment and Selection
News 2026-07-28
Jute stick is the woody stem left after the fiber has been stripped from the jute plant. The jute industry is generally concentrated in a small number of countries, mainly Bangladesh and India, and for every ton of jute fiber produced, a larger tonnage of jute stick is generated as a by-product. That material has traditionally been used as domestic fuel, burned in the field, or left to decompose. It has good calorific value and moderate ash compared with high-ash residues such as rice straw, though higher than wood, which makes it a credible pellet feedstock where the supply is concentrated and the logistics are short.
It is also a feedstock that punishes a generic approach. Jute stick is a bast fiber material, tough and stringy, with different grinding, feeding, and die behavior from wood. This page is written for project developers and procurement teams who need to decide whether jute stick is suitable, how the line should be configured, and what to verify before committing to equipment. Shandong Changsheng Machinery works with agricultural residue projects of this type, and the guidance below reflects how those lines are configured and where projects typically run into trouble.
What is jute stick waste?
Jute stick is the stem of the jute plant after the fiber has been extracted. It is woody, relatively dense compared with straw, and available in large quantities in jute-growing regions. Published figures for the ratio of jute stick to jute fiber, usually quoted at roughly 1.5 to 2 tons of stick per ton of fiber, are indicative. The actual ratio depends on the variety, the retting method, and the harvest conditions. National jute fiber statistics, jute stick generation, the collectable share, and the volume that can actually be contracted as a commercial feedstock are four different numbers. National fiber output does not translate directly into usable stick, because collection rates, competing domestic fuel use, and the economics of gathering and transport all reduce the amount that reaches a plant. For project planning, the relevant figure is the jute stick you can secure within an economic transport distance.
Properties and challenges of jute stick
Fiber structure and hardness. Jute stick is tougher and more fibrous than most straws. It resists size reduction, wraps around shafts, and consumes more grinding energy. The fibers do not break down as cleanly as wood, so the grinder and the feeding system have to be designed for stringy material.
Moisture content and bulk density. Jute stick is usually drier at collection than many agricultural residues, but moisture still varies with storage and season, and the material is relatively light for its volume. Low bulk density affects conveying, storage, and the steadiness of feed into the mill, and it is one of the reasons feeding design matters more here than on a wood line.
Ash content and material contamination. Jute stick has moderate ash by agricultural residue standards, though higher than wood and lower than high-silica straws. It still arrives with soil, sand, and stones, and contamination accelerates wear on dies, rollers, and hammer mill parts. Cleaning and destoning ahead of the grinder are not optional.
Jute stick pre-processing requirements
Cleaning and shredding. Jute stick is cleaned of soil and stones before size reduction, then cut and shredded. A destoner or similar cleaning stage protects the downstream equipment, and the shredding stage reduces the stick to a size the dryer and grinder can handle.
Drying and moisture control. Jute stick often arrives within a workable moisture range, so drying may be minimal or unnecessary in some projects. When drying is required, the sizing basis should be the actual incoming moisture range and the target moisture at the die, not an average. The moisture target at the die should be established by testing the actual material. A reference range is sometimes quoted around 10–14 percent at the die, but this is a starting point for trials, and the correct value depends on the fiber condition, the die, the pellet diameter, and whether conditioning is used. Moisture at collection and moisture at the die should be treated as separate measurements, not as a single number.
Grinding and particle size. A hammer mill reduces the material to a particle size the die can accept. The right target is the one that feeds steadily and forms a durable pellet on your die. Over-grinding raises energy cost and can worsen feeding on fibrous material; under-grinding leaves long fibers that bridge and blind. Particle size and feed uniformity also affect pelletizing efficiency directly: a consistent, correctly sized grind lets the die fill evenly, holds die temperature stable, and supports the mill’s rated output, while a coarse or variable grind forces the operator to run slower to avoid blocking, so the same machine produces less on a poorly prepared material than on a well prepared one.
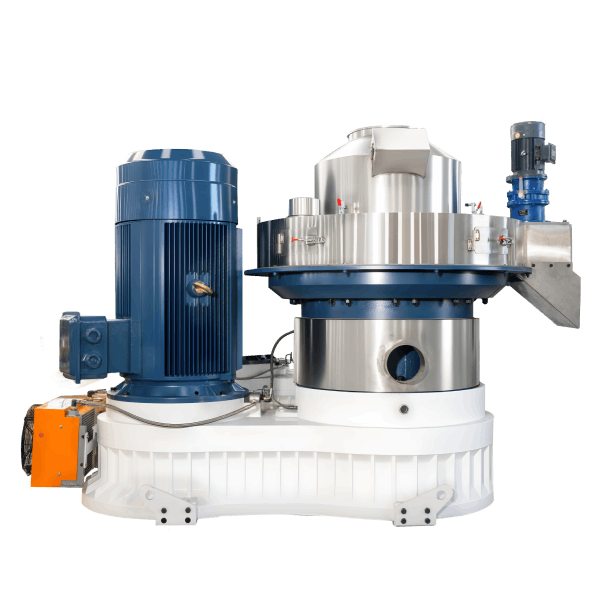
Jute stick pellet production process
A complete jute stick line typically runs through the following stages. Each stage has a defined role, and skipping or merging one usually shows up later as unstable output or poor pellet quality.
Raw material receiving and storage. Jute stick is received, weighed, and stored under cover where possible. Storage moisture and contamination at this stage set the load on everything downstream.
Pre-cleaning. Soil, sand, stones, and tramp material are removed before size reduction. A destoner or similar stage is the normal choice, and it protects the shredder, grinder, and die from avoidable wear.
Chipping and shredding. Whole stick is cut and shredded to a size the dryer and grinder can accept. This stage is what makes fibrous jute stick manageable for the rest of the line.
Drying. Thermal drying is applied where the incoming moisture is above what the die can work with. A rotary dryer is common; the sizing basis is the actual incoming moisture range and the target moisture at the die, not an average. Where the stick arrives dry enough, this stage may be reduced or omitted and capital directed toward cleaning, grinding, and dust control instead.
Hammer milling. The dried material is ground to a particle size the die can accept, matched to die hole diameter and confirmed in trial production.
Conditioning. Heat or steam conditioning may be used to soften fibers and improve binding. Whether it is needed, and at what temperature and settings, depends on the material and the mill and should be confirmed in trials.
Pelletizing. The prepared material is formed into pellets on a die selected for jute stick, the target diameter, and the confirmed moisture.
Cooling and screening. Pellets are cooled to stabilize them and screened to remove fines before storage.
Packaging and storage. Finished pellets are bagged or stored in silos, with dust control and moisture protection.
Configuration is not identical for every project, and incoming moisture is one of the main reasons. A line receiving dry stick may reduce or skip thermal drying. A line receiving wet material in a humid season needs enough drying capacity to cover the wet end of the range, and the dryer, not the pellet machine, becomes the throughput bottleneck when moisture is high. Where jute stick is blended with wood or another residue, a mixing stage is added and the die specification is set for the blend rather than for jute stick alone. Shandong Changsheng Machinery configures jute stick lines around the actual incoming moisture, the target output, the pellet diameter, and the site conditions, rather than around a standard equipment list.
How to choose a jute stick pellet machine
Motor power and production capacity. Motor power does not determine output by itself. Real capacity depends on the feedstock, its moisture at the die, fiber condition, pellet diameter, die specification, and how steadily the line is fed. There is no multiplier that converts a standard rating into a jute stick rating. Ask for capacity to be stated against a defined feedstock and moisture, and expect the figure to be confirmed in trial production. Where a supplier quotes capacity, confirm whether it refers to raw material throughput or finished pellet output. Capacity also shifts with pellet diameter: smaller diameter pellets restrict flow through the die and reduce output, while larger diameters generally raise it, so a capacity figure quoted without a stated pellet diameter is not a complete figure.
Ring die and roller configuration. Die material, hole diameter, open area, and compression ratio all need to match the jute stick being run. The ring die compression ratio should be selected according to jute stick fiber characteristics, moisture content, pellet diameter, and actual trial results. It should not be treated as a universal specification, and it should not be derived from lignin content alone. Abrasion-resistant die and roller materials are relevant, but the specific grade should be chosen against actual wear conditions rather than adopted as a blanket standard.
Feeding and conditioning system. Because jute stick is fibrous and relatively light, stable feeding is critical. Uneven feed destabilizes die temperature and produces inconsistent pellet quality, and on fibrous material it also raises the risk of blocking. Whether a force feeder or assisted feeding is needed depends on the bulk density of the material and on trial results with the specific mill. Conditioning with heat or steam can improve binding, but the need for conditioning, the temperature, and the settings depend on the material and the mill and should be confirmed in trials rather than assumed.
Wear resistance and maintenance. Jute stick and its contaminants wear parts faster than clean wood. Die and roller life, hammer mill component life, and the spare parts plan should be discussed at the quotation stage. Buyers should ask for the die material and heat treatment, the die hardness and wear performance, the roller material and surface treatment, and the expected replacement interval for dies and rollers, rather than accepting a material grade on trust.
Jute stick pellet quality and applications
Pellet quality should be described through test parameters rather than fixed promises. The relevant tests are moisture content, ash content, calorific value, pellet durability, bulk density, and pellet diameter and length. Published ranges for jute stick pellets often place calorific value around 16–18 MJ/kg and ash at roughly 3–6 percent, with durability and bulk density varying with the line and the material. These are indicative and should be confirmed by laboratory testing on pellets made from your jute stick, with the material source, equipment, and test conditions recorded.
The main applications are industrial combustion, power generation, and regional heating. Jute stick pellets are a reasonable fit for industrial boilers and co-firing where ash handling is available. Residential heating is a weaker fit where ash limits are strict. Export suitability depends on the destination market’s quality requirements and on consistency of production, which in turn depends on consistent feedstock and a line that is not being pushed beyond its capacity.
Jute stick pellet production line cost factors
Project cost in a jute stick line is driven by collection logistics and pre-processing more than by the pellet machine itself. The main cost elements are raw material collection and transport, reception and storage, pre-cleaning and destoning, chipping and shredding, drying system and its heat source where required, hammer milling, conditioning where used, the pellet machine and its die and roller configuration, cooling and screening, dust collection, packaging, civil works, and electrical infrastructure. Collection distance and raw material price can dominate the operating economics, and drying energy is the largest process cost when drying is required.
Investment is best built from a defined scope rather than quoted as a generic range. A developer should ask for a quotation that states the equipment scope, the capacity basis, the dryer sizing basis, the die specification, and the acceptance test, and should compare quotations on that basis rather than on headline price.
A payback period should not be quoted without a full cost and revenue model. A low raw material cost does not by itself make a project profitable. Payback depends on collection and transport cost, the equipment investment, the pellet selling price in the target market, capacity utilization, and the cost of energy, labor, and wear parts. The practical approach is to build the model with local figures for each input and to test how sensitive the result is to the two or three that carry the most uncertainty.
How to select a pellet machine supplier
Jute stick is not a feedstock where general biomass experience transfers automatically. A supplier should be able to explain how they would handle the fiber toughness, the low bulk density, the contamination, and the moisture variation, and should be willing to test your material rather than quote from a catalog. Ask whether the supplier has experience with jute stick or comparable fibrous residues, whether they can supply the complete line rather than the pellet machine alone, and how they will confirm capacity and pellet quality before shipment. A supplier who cannot describe the cleaning, grinding, and feeding stages in detail is a warning sign worth taking seriously, because those stages decide whether a fibrous feedstock line runs steadily.
Frequently asked questions
Can the machine process whole jute stick without prior crushing? Generally no. Jute stick needs cleaning, chipping, and shredding before it reaches the grinder and the pellet machine. Feeding whole stick into a mill designed for prepared material will block the feeder and damage the die.
Do I need a dryer for jute stick? Not always. Jute stick often arrives within a workable moisture range, so drying may be minimal. Whether a dryer is needed, and how large it should be, depends on the actual incoming moisture range and the target moisture at the die, both confirmed by testing your material.
How do I determine the real capacity of a jute stick pellet machine? Capacity should be quoted against a defined feedstock, moisture, and pellet diameter, and confirmed in trial production on your material. Ratings transferred from wood or straw are not reliable for jute stick.
Can you run a trial on my jute stick before I commit to equipment? A trial on your actual material is the right way to confirm capacity, die specification, and pellet quality. Ask for the test conditions and results to be documented, including moisture, equipment used, and pellet durability.
What should I check on the die and rollers before buying? Ask for the die material and heat treatment, die hardness and wear performance, roller material and surface treatment, and the expected replacement interval. Wear parts are a recurring cost on fibrous feedstock, and the replacement interval belongs in the commercial comparison.
How does a jute stick line differ from a wood line? A wood line is built around relatively uniform, free-flowing material. A jute stick line carries a heavier cleaning and shredding section, a feeding system designed for light and fibrous material, and a die specification set for jute stick rather than for wood. The upstream equipment usually accounts for a larger share of the line’s capital cost than it would on a wood line.
Is jute stick pelleting economically viable? It can be, where jute stick is available at low cost within a short collection distance and there is a market for industrial-grade pellets. Viability depends on collection and transport, drying energy where required, pellet price, realistic output, and wear part costs, and should be assessed with a project-specific cost model rather than a generic estimate.