Peanut Shell Pellet Mill: Grinding, Drying & Pellet Production
News 2026-04-26
Peanut shells are a dense, hard agricultural residue produced during peanut shelling. Their hardness, moisture variation, mineral contamination, and storage condition affect grinding energy, pellet mill capacity, and pellet quality. Peanut shell is not simply another wood substitute.
This guide is written for peanut shelling plants, peanut processing factories, agricultural biomass plants, industrial boiler fuel users, and biomass pellet producers. It covers peanut shell characteristics, cleaning, grinding energy, drying, machine configuration, pellet quality, storage safety, production process, capacity, applications, common problems, buying guide, and FAQ. For generic pellet mill selection, see the separate pellet mill guide on this site.
What Are Peanut Shell Pellets?
Peanut Shell as an Agricultural Residue
Peanut shell is the hard outer covering removed during shelling. It is produced in large volume at shelling plants and peanut processing factories. Because it is dry and has moderate energy content, it is a suitable feedstock for fuel pellet production when properly prepared.
Fuel Pellet Applications
Peanut shell pellets are used in industrial boilers with ash removal systems, in co-firing with coal, and in some biomass power applications. They are not recommended for home pellet stoves because of higher ash content compared with premium wood pellets.
Peanut Shell vs Wood Sawdust
Peanut shell is harder and more abrasive than wood sawdust. It requires more grinding energy, produces more hammer wear, and usually needs a harder die and roller material. Moisture range for pelletizing is also narrower than wood. These differences affect machine selection, operating cost, and spare parts planning.
Peanut Shell Characteristics
Shell Hardness
Peanut shell is harder than most wood materials. Hardness affects grinding energy, hammer wear, die load, and pellet density. Harder material requires more motor power for the same output.
Bulk Density
Bulk density of ground peanut shell is relatively low, often in the range of about 120 to 180 kg/m³ depending on moisture, particle size, and shell origin. This range should be confirmed with a laboratory test for your specific material. Low bulk density affects feeder design, storage volume, and transport cost. Feeder bridging is a common problem if the feeder is not designed for this material.
Moisture
Fresh shell moisture varies by region and storage condition. Typical target moisture before pelletizing is around 12 to 15 percent. This range depends on shell source, storage condition, die compression ratio, and machine configuration. Below 10 percent, fire risk increases. Above 15 percent, pellet quality drops, mold risk increases, and aflatoxin risk may rise. The exact target should be confirmed with a pelletizing test.
Mineral Contamination
Peanut shells often contain soil, sand, and small stones from harvesting and shelling. Mineral contamination accelerates die and roller wear and reduces pellet quality. Cleaning before grinding is important.
Storage Condition
Peanut shells stored in damp conditions can develop mold. Moldy shells may contain aflatoxin, which is a food safety and health concern. Storage condition directly affects both fuel quality and safety.
Peanut Shell Cleaning Before Pelletizing
Removing Soil and Stones
Soil and stones are removed by screening and air classification. This step reduces die wear and blockage. It is strongly recommended when shells contain visible sand or soil.
Magnetic Separation
Magnetic separators remove ferrous metal such as nails and wire. Double-stage separation is common in commercial lines.
Air Classification
An air classifier removes sand, stones, and heavy particles before grinding and pelletizing. This step extends die life and improves pellet quality.
Screening
Screening removes oversize and undersize material and improves feeding stability. Screen size should be selected based on shell condition and downstream equipment.
Why Peanut Shell Requires More Grinding Energy
Peanut shell requires more grinding energy than wood because of its hardness, density, and silica content. A hammer mill may draw significantly more current when grinding peanut shell than when grinding wood at the same screen size.
Key engineering points:
Shell hardness increases hammer load and wear.
Screen size affects grinding energy and final particle size. A 4 to 5 mm screen is common for peanut shell, finer than typical wood grinding.
Hammer wear is faster than with wood. Hammer inspection intervals of around 100 hours are common in commercial peanut shell grinding, compared with around 200 hours for wood, depending on shell condition and hammer quality.
Motor sizing must account for higher grinding load. Undersized motors cause overload and downtime.
Particle size affects pellet quality and die load. Consistent particle size improves feeding and compression.
Capacity loss compared with wood is common at the same motor power. Where shell volume is high, a parallel hammer mill configuration may be used to maintain throughput.
The exact grinding energy and hammer wear should be confirmed with a test using your shell condition, not assumed from general figures.
Peanut Shell Drying Before Pelletizing
Fresh Shell Moisture
Fresh shell moisture varies by region and harvest condition. It should be measured before drying, because moisture variation is a common cause of unstable output and poor pellet quality.
Field and Plant Storage
Shells stored outdoors or in damp conditions absorb moisture. Storage condition affects drying requirement and mold risk. Covered, ventilated storage is recommended.
Drying Temperature
A rotary dryer or air drying is commonly used. Dryer inlet temperature should be controlled to avoid burning the shell. Over-drying increases fire risk.
Over-Drying Risk
Shells below 10 percent moisture become more combustible and increase fire risk in the die. Moisture should be monitored at the feeder, not only after drying.
Peanut Shell Pellet Mill Configuration
Ring Die
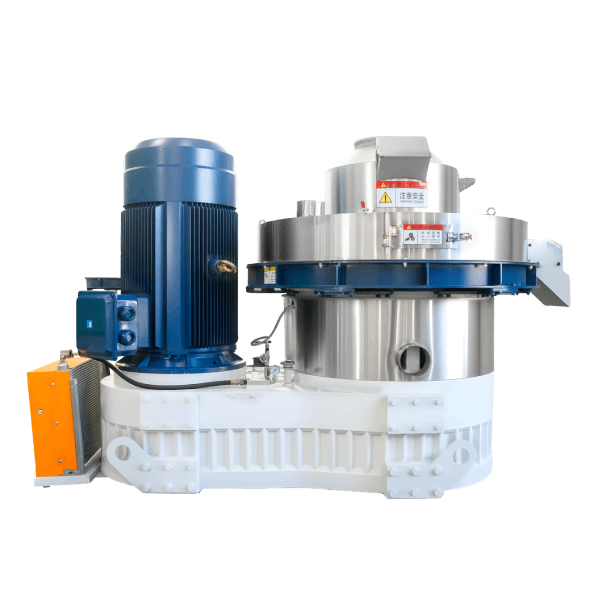
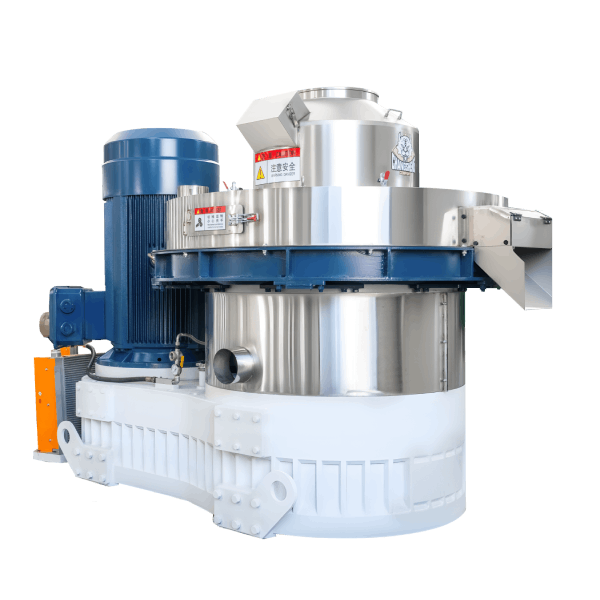
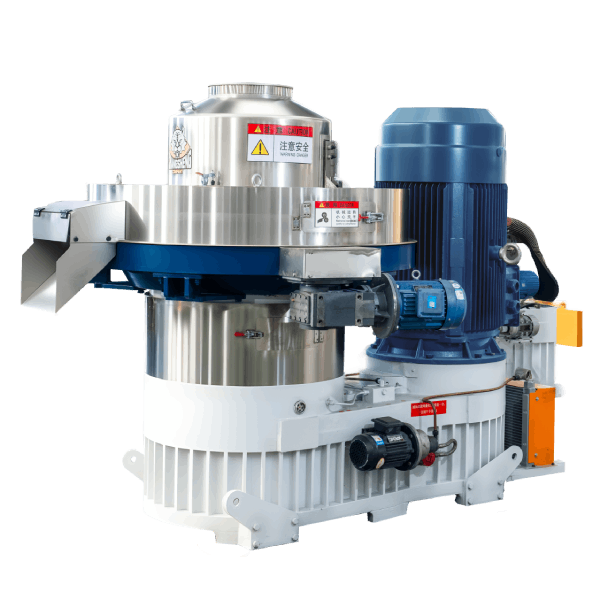
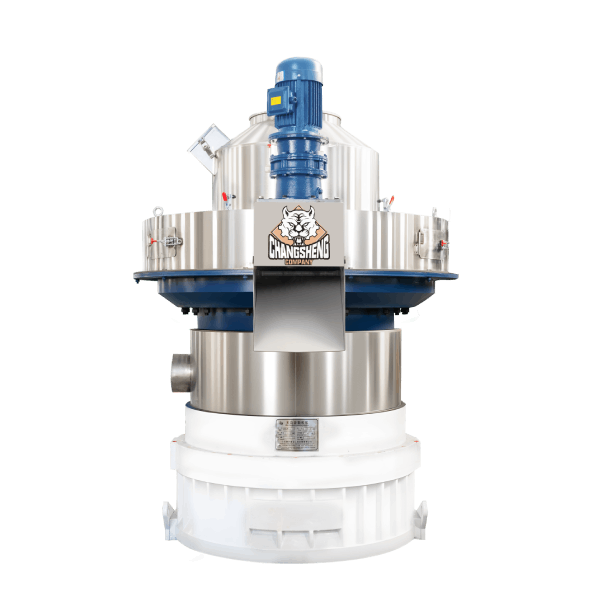
Ring die machines are used for commercial peanut shell pellet production. Die hole diameter, taper, and compression ratio must be selected for peanut shell, not for wood. Die material and heat treatment should be selected for abrasive service.
Roller
Roller shells should be selected for high abrasion. Hardfacing or carbide overlay extends roller life. Roller clearance should be checked regularly because shell abrasion changes clearance quickly.
Hammer Mill
Hammer mill selection should match shell hardness and target particle size. Screen size, hammer type, and motor power all affect grinding performance and energy consumption.
Feeder
Peanut shell is fibrous and low in bulk density, so feeder design must prevent bridging. A horizontal breaker shaft, variable pitch screw, or hopper vibrator may be required. Variable frequency feeding improves stability.
Cooler
Cooling hardens pellets and reduces fines. Cooling requirement depends on pellet diameter, initial pellet temperature, and ambient conditions.
Dust Collection
Peanut shell dust is fine and poses both health and explosion risks. Dust collection with high-efficiency cyclone and filters is required. Explosion venting, spark detection, grounding, and where applicable ATEX-rated equipment are recommended for commercial lines.
Peanut Shell Pellet Quality
Density
Bulk density of peanut shell pellets is typically in the range of about 900 to 1,200 kg/m³, depending on compression and material.
Durability
Durability depends on lignin content, compression ratio, moisture, and cooling. Peanut shell pellets are generally less durable than premium wood pellets and should be handled accordingly.
Ash
Ash content of peanut shell is typically in the range of 8 to 12 percent. This range depends on shell source and soil contamination, and should be confirmed by laboratory test. Ash affects boiler design and ash handling.
Moisture
Finished peanut shell pellets typically have moisture around 8 to 10 percent. Moisture above this range reduces fuel value and increases mold risk.
Pellet Size
Common pellet diameters are 6, 8, 10, and 12 mm, depending on boiler feeding system and application.
Fuel Performance
Peanut shell pellets have calorific value in a similar range to wood, typically around 16 to 18 MJ/kg, depending on shell source and ash content. Higher ash reduces fuel value and increases ash handling cost. These values should be confirmed by laboratory test for your specific shells.
Peanut Shell Storage and Aflatoxin Risk
Peanut shells stored in damp conditions can develop mold, which may produce aflatoxin. Aflatoxin is a food safety and health concern. Storage management is part of safe pellet production.
Practical measures:
Store shells in a covered, ventilated area.
Keep shells dry. Drying to below 12 percent moisture within 48 hours of shelling reduces mold risk.
Test incoming shells if there is any history of mold or damp storage. Common test methods for aflatoxin include ELISA for rapid screening and HPLC for confirmatory analysis.
Reject visibly moldy shells.
Keep dust collection enclosed and well maintained to reduce operator exposure.
If pellets are intended for animal bedding or feed-adjacent use, additional testing and regulatory compliance may be required. Exact limits, test methods, and regulatory requirements should be confirmed against current official standards and regulations, not assumed from general figures.
If pellets are intended for fuel use only, focus on moisture, ash, and combustion performance rather than bedding-grade requirements.
Peanut Shell Pellet Production Process
Peanut shell pellet production typically follows this sequence: peanut shell receiving, cleaning, drying, grinding, screening, pelletizing, cooling, screening, and storage.
Cleaning removes soil, stones, and metal. Drying reduces moisture to the target range. Grinding reduces particle size. Screening improves particle size consistency. Pelletizing forms pellets. Cooling hardens pellets. Screening removes fines and oversize. Storage must protect pellets from moisture and self-heating.
Each step is included for a specific reason. Skipping cleaning or moisture control is a common cause of short die life and poor pellet quality.
Peanut Shell Pellet Machine Capacity
Capacity is not a fixed number. It depends on shell hardness, moisture, particle size, motor power, die specification, and feed rate.
Rated capacity is only meaningful when material, moisture, particle size, pellet diameter, and die specification are stated. Actual capacity is usually lower than rated capacity because of shell hardness, moisture variation, and feeder stability.
Typical commercial peanut shell pellet lines range from about 0.5 to 3 t/h, depending on configuration and shell condition. Smaller lines are used by shelling plants processing their own shells, while larger lines are used by industrial fuel producers. The exact capacity for your project should be confirmed with test data at your actual shell condition.
A capacity margin of about 20 to 30 percent above the calculated requirement is a practical starting point. The exact margin depends on material consistency and operating hours.
Peanut Shell Pellet Machine Applications
Peanut shelling plants: converting shells into fuel for own boilers or sale.
Peanut processing factories: managing shell waste and reducing disposal cost.
Agricultural biomass plants: producing pellets from local residues.
Industrial boiler fuel: supplying pellets to industrial customers with ash handling systems.
Biomass pellet producers: adding peanut shell pellets to product range for specific markets.
These applications are common in peanut-producing regions such as the United States, China, India, Argentina, and Nigeria, where shell supply is concentrated and transport distance to the pellet line is short.
Common Peanut Shell Pelletizing Problems
High grinding load: caused by shell hardness and silica content. Motor sizing and screen size should be reviewed.
Die wear: caused by shell hardness and mineral contamination. Die material and cleaning should be reviewed.
Sand contamination: accelerates die and roller wear. Air classification is recommended.
Moisture fluctuation: causes unstable output and poor pellet quality. Moisture should be monitored before pelletizing.
Feeder bridging: caused by low bulk density and fibrous structure. Feeder design should be adapted.
Dust: poses health and explosion risks. Dust collection, explosion venting, and grounding are recommended.
How to Choose a Peanut Shell Pellet Mill
Shell volume: determines required capacity and operating hours.
Moisture: determines drying requirement.
Contamination: determines cleaning and air classification requirement.
Grinding requirement: determines hammer mill size and motor power.
Target capacity: determines pellet mill type and motor power.
Pellet diameter: determines die specification.
Fuel use: determines pellet quality and boiler compatibility requirements.
These seven inputs are enough to recommend a suitable configuration.
Frequently Asked Questions
Can peanut shells be made into pellets?
Yes. Peanut shells can be pelletized into fuel pellets with a ring die pellet mill configured for hard, abrasive material.
Are peanut shell pellets good fuel?
Yes, for industrial boilers with ash removal systems. Calorific value is in a similar range to wood, but ash content is higher, typically 8 to 12 percent. They are not recommended for home pellet stoves.
Do peanut shells need drying?
In most cases, yes. Target moisture before pelletizing is typically around 12 to 15 percent. Over-drying below 10 percent increases fire risk. Above 15 percent reduces pellet quality and increases mold risk.
Why are peanut shells difficult to grind?
Peanut shells are harder and more abrasive than wood. They require more grinding energy and cause faster hammer wear. A 4 to 5 mm screen and correctly sized motor are recommended.
What hammer mill is suitable?
A hammer mill with suitable screen size, hammer type, and motor power for peanut shell hardness. A 4 to 5 mm screen is common. Hammer inspection intervals should be shorter than for wood, around 100 hours in typical commercial peanut shell grinding.
What moisture is suitable?
Typical target moisture before pelletizing is around 12 to 15 percent. This range depends on shell source, storage condition, die compression ratio, and machine configuration. The exact target should be confirmed with a pelletizing test.
Can peanut shells be mixed with sawdust?
Yes. Mixing shells with sawdust reduces ash content and may extend die life. The mix ratio should be consistent and confirmed with a pelletizing test.
How do I remove soil from peanut shells?
Screening, magnetic separation, and air classification are used. Air classification is strongly recommended when shells contain visible sand or soil.
Does peanut shell cause die wear?
Yes. Peanut shell is harder than wood, and mineral contamination increases wear. Die material and heat treatment should be selected for abrasive service. Expected die life should be confirmed with test data at your shell condition. Die life varies widely by shell source and contamination level, so it should not be assumed from a general figure.
What capacity pellet mill do I need?
Calculate annual shell volume divided by annual operating hours, then add a capacity margin of about 20 to 30 percent. The exact margin depends on shell consistency and operating hours. Actual capacity depends on shell hardness, moisture, particle size, and die specification.
Author Introduction
This article was prepared by a technical content specialist with over ten years of experience in industrial equipment, biomass processing machinery, and B2B export projects. The author has worked with peanut shell pellet projects in peanut-producing regions such as the United States, China, India, Argentina, and Nigeria, including high-ash and high-silica shells, and understands the practical challenges buyers face in grinding, drying, cleaning, die selection, dust safety, and storage management.
The content reflects real engineering practice in peanut shell pellet mill selection, feedstock preparation, grinding energy management, and project execution. It is intended to help peanut shelling plants, peanut processors, agricultural biomass plants, and pellet producers make informed decisions and reduce project risk. The author is affiliated with Shandong Changsheng Machinery Co., Ltd.
Call to Action
If you are planning a peanut shell pellet project and need help confirming grinding, drying, cleaning, machine configuration, die material, dust protection, or spare parts plan, you can request a technical proposal based on your peanut shell and required output. Share your shell volume, moisture, ash content, soil contamination level, target capacity, pellet diameter, power supply, and final fuel application, and a suitable configuration can be recommended.
You can also request a quotation for a peanut shell pellet mill, ask for a process flow diagram, request a spare parts list, or arrange a video factory inspection before making a final decision. If you have a peanut shell sample, a pelletizing test can be arranged to confirm die selection and expected performance under your actual material conditions.