Pellet Machine Squealing Noise: Causes, Diagnosis and Fixes
News 2026-10-23
A pellet machine squealing noise is a high-frequency sound that comes from a small number of sources, but material squeal, electrical noise, and a faulty reading can produce a similar result. These must be ruled out before the squeal is treated as a mechanical fault. Belt slip, an early bearing failure, and a dry die surface are the three most common sources, and the actual frequency of each depends on the machine type and operating conditions.
The squeal type matters more than for other noises, because the three causes require completely different fixes. A belt slip is corrected by tension and alignment. A bearing at early failure is corrected by replacement. A dry die is corrected by feed and moisture. Treating one as another wastes parts and time, and a dry die left running can bake material onto the die surface.
This article covers how to locate and measure the squeal, how squeal and vibration differ, how to tell the three main causes apart, how belt and bearing type change what you hear, which checks to run before stopping, when to stop rather than adjust, what damage to inspect after a stop, and what information to send a supplier if the source cannot be found on site.
How to Locate and Classify the Squeal
A squeal should be located and classified before the machine is stopped, because it may not reproduce after cooldown.
| Measurement item | What to record | Why it matters |
|---|---|---|
| Location | Die chamber, belt drive, roller assembly, main shaft bearing, motor | Narrows the component |
| Behaviour with load | Worse under load, unchanged, or only when starved | Separates belt slip from bearing failure and dry die |
| Continuity | Continuous or intermittent | Separates a progressive fault from a load-dependent one |
| Frequency character | High-frequency squeal or lower-frequency rumble | Separates early bearing failure from advanced failure |
| Baseline | A recording of normal running noise | Confirms whether the squeal is new |
| Vibration at bearing housings | Direction and amplitude | Confirms whether a bearing is involved |
A mechanic’s stethoscope or a listening rod can localise the squeal to a specific housing. A non-contact vibration meter can confirm whether a bearing is vibrating. The boundary between a high-frequency squeal and a lower-frequency rumble is defined by the vibration measurement and the bearing supplier documentation, not by a general figure. The acceptable noise and vibration levels for the machine come from the machine manual and the supplier documentation for the specific model.
Squeal and Vibration Are Different Signals
Squeal and vibration often appear together, but they are different signals and are measured differently.
- Squeal is a high-frequency sound. It is produced by friction or by a small-amplitude vibration at a high frequency.
- Vibration is continuous motion. It is measured at the bearing housing or the frame in velocity or acceleration, at a lower frequency than the squeal itself.
- Resonance can make a small friction source produce a loud squeal at a specific operating condition, without a progressive mechanical fault.
A squeal without measurable vibration at the frame is often belt slip or a dry die, not a bearing fault. A squeal with measurable vibration at a bearing housing is more likely to be a bearing fault. The two should be recorded together.
Belt and Bearing Type Change What You Hear
Belt type and bearing type affect the squeal and the inspection method. The machine manual and the component supplier documentation take precedence over this section.
| Component type | Squeal pattern | What to inspect |
|---|---|---|
| V-belt | Intermittent squeal, worse under load, often at startup | Belt tension, groove wear, belt glazing |
| Synchronous (timing) belt | Sharper squeal, often at a specific speed, changes with load | Tooth wear, belt tension, pulley tooth condition |
| Flat belt | Continuous squeal, changes with load and alignment | Belt surface, alignment, tension |
| Deep groove ball bearing | High-frequency squeal at early failure, changes with speed | Bearing temperature, vibration, lubricant condition |
| Cylindrical roller bearing | Lower-frequency squeal than a ball bearing, often with vibration | Bearing temperature, vibration, roller condition |
| Tapered roller bearing | Squeal often accompanied by a temperature rise, changes with load | Bearing temperature, preload, lubricant condition |
A squeal from a V-belt is usually tension or glazing. A squeal from a synchronous belt is usually tooth wear or tension. A squeal from a flat belt is usually alignment or surface condition. A squeal from a deep groove ball bearing at early failure is usually the earliest warning available, and it is not the same as the rumble of an advanced failure.
Belt Slip
Why it squeals: A belt that is not tight enough, misaligned, or worn slips on the pulley. The slip produces a high-frequency squeal that changes with load. The squeal is worse under high load, because the transmitted torque increases and the friction demand rises, so a belt with insufficient tension slips more readily.
What to check: Belt tension against the machine manual specification. Belt alignment against the pulley groove. Belt surface condition for glazing, cracking, or wear. Pulley condition for groove wear.
What to do: Adjust tension and alignment to the manual specification. Replace the belt if it shows glazing, cracking, or wear. A belt with a bright, hard, cracked, or worn surface has already lost friction capacity, and adjusting tension on such a belt will not restore it. Replace the belt before adjusting tension on a glazed belt. Do not apply belt dressing unless the machine manual and the belt supplier documentation permit it, because dressing can change the friction characteristic of the belt and the pulley.
Bearing at Early Failure
Why it squeals: A bearing whose lubricant has broken down, or whose raceway has started to wear, produces a high-frequency squeal before it produces the lower-frequency rumble of advanced failure. The squeal follows rotation speed and is often accompanied by a small temperature rise that may not be obvious on a gauge.
What to check: Bearing temperature against the machine manual. Bearing noise with the machine stopped and locked out, by rotating the shaft by hand where this is permitted by the manual. Vibration at the bearing housing, in the direction and unit recorded in the baseline.
What to do: Stop the machine and inspect. Replace the bearing according to the machine manual. Do not continue running with a bearing squeal, because the squeal is the early stage and the failure that follows usually damages the shaft and the surrounding components.
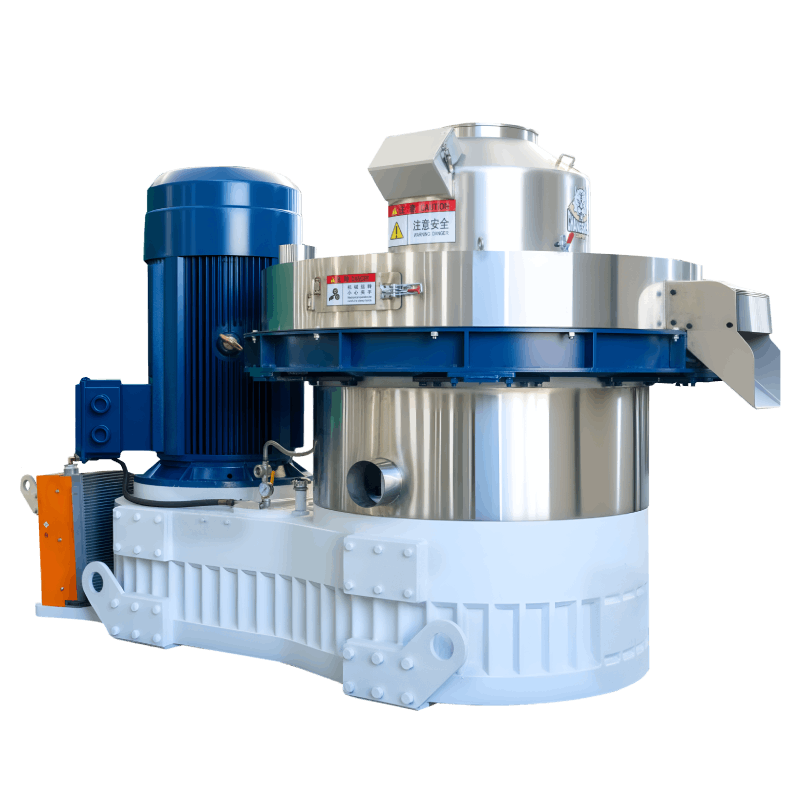
Dry Die Surface
Why it squeals: When the die chamber is starved, the rollers run against the die surface without a material cushion. The metal-to-material contact produces a squeal that is often described as a dry or scraping squeal. The squeal is accompanied by a rise in die temperature and a fall in motor current, because the die is not doing compression work.
What to check: Feeder delivery and hopper level. Die temperature trend. Motor current trend. Die surface condition after a stop.
What to do: Restore stable feed gradually. Do not raise feeder speed sharply to catch up, because a sudden feed surge can overload the die chamber and produce the opposite problem. If the die surface has baked material from running dry, inspect it for heat damage before returning to production.
Dry Die Squeal or Material Squeal
A squeal from the die chamber is not always a dry die. Some materials produce a squeal during normal compression, especially oily materials and high-fiber materials. The two are separated by the accompanying conditions.
| Observation | Dry die squeal | Material squeal |
|---|---|---|
| Motor current | Falling, because the die is underloaded | Normal for the material and feed rate |
| Die temperature | Rising | Normal for the material and feed rate |
| Feeder delivery | Starved or bridging | Normal |
| Pellet quality | Soft, uneven, or excessive fines | Normal for the material |
| Squeal after feed is restored | Reduces or stops | Continues at the same level |
A material squeal that continues after feed is confirmed stable is a property of the material, not a fault. Confirm this against the historical baseline for the material before treating it as a fault.
How to Separate the Three Causes
The three causes can be separated by observations made before the machine is stopped.
| Observation | Belt slip | Bearing at early failure | Dry die surface |
|---|---|---|---|
| Location | Belt drive area | Roller or main shaft bearing area | Die chamber area |
| Behaviour with load | Worse under high load | Continuous, worse under load | Present when the die is starved |
| Motor current | Normal or fluctuating | Normal or rising | Falling, because the die is underloaded |
| Die temperature | Normal | Normal, unless the bearing is near the die | Rising |
| Belt condition | Glazing or wear visible | Normal | Normal |
| Feed condition | Normal | Normal | Feeder starved or bridging |
If the squeal is at the belt drive and changes with load, check the belt first. If the squeal is at a bearing and follows rotation speed, check the bearing first. If the squeal is at the die chamber and motor current is falling, check the feeder first.
Immediate Checks Before Stopping
These checks can be made with the machine running and narrow the cause before a stop decision.
| Check | What to look for | What it tells you |
|---|---|---|
| Squeal location | Belt drive, bearing area, or die chamber | Narrows the cause |
| Squeal behaviour with load | Worse, unchanged, or only when starved | Separates belt slip from bearing failure and dry die |
| Motor current | Above, within, or below the manual range | Separates dry die from bearing and belt |
| Die temperature | Rising | Points to a dry die |
| Bearing temperature | Rising | Points to a bearing at early failure |
| Belt condition | Glazing or wear | Points to belt slip |
| Feeder delivery | Steady or starved | Points to a dry die |
If the squeal is at the belt drive and the belt shows glazing or wear, stop and replace the belt. If the squeal is at a bearing with a temperature rise, stop and inspect. If the squeal is at the die chamber with falling current, restore feed before stopping.
When to Stop Rather Than Adjust
Do not keep running to see whether the squeal clears. Stop the machine when any of the following applies. Limits must come from the machine manual.
| Condition | Action |
|---|---|
| Squeal at a bearing with a temperature rise | Stop immediately. Inspect the bearing. |
| Squeal at the belt drive with belt glazing or wear | Stop and replace the belt. |
| Squeal at the die chamber with die temperature rising | Stop feed first. If temperature does not fall, stop the main motor and inspect the die surface. |
| Squeal with motor current above the manual range | Reduce feed rate first. If squeal and current do not fall, stop. |
| Squeal with smoke or burning smell | Stop immediately and lock out power. |
Cooldown and Inspection Safety
Components that are at fault may be at a temperature that causes burns, and rotating parts must be stationary before inspection.
| Check area | Safety point before inspection |
|---|---|
| Die chamber | Allow the die chamber to cool before opening; lock out power |
| Roller assembly | Confirm the rotor is stationary and locked out before checking roller rotation by hand |
| Bearings | Allow housings to cool before touching; use a temperature reading first |
| Belt drive | Lock out power before checking belt tension or alignment |
| Motor | Lock out power before inspection |
Damage Inspection After a Squeal Event
A squeal can leave damage that is not visible from the control panel.
| Component | What to check |
|---|---|
| Die surface | Baked material, discoloration, or glass-like material adhering to the surface |
| Die hole entrance | Material hardened at the hole entrance |
| Rollers | Glazing, uneven wear, or baked material on the roller face |
| Roller bearings | Free rotation, noise, lubricant condition |
| Main shaft bearing | Temperature after cooldown, noise, lubricant condition |
| Belt | Glazing, cracking, or wear |
| Pulley | Groove wear or misalignment |
| Motor | Bearing noise, temperature, insulation check by a qualified person if electrical fault is suspected |
If the die or rollers show baked material, follow the die manufacturer procedure for baked material removal. If the hole geometry has changed after removal, treat the die as damaged and replace it.
Restart After a Squeal Event
Restarting is not the same as fixing. Confirm the following before returning to normal feed rate. Limits must come from the machine manual.
| Acceptance item | What to confirm |
|---|---|
| Squeal | No squeal at reduced or normal feed rate |
| Motor current | Stable and within the manual range |
| Die temperature | Stable, without a rising trend |
| Bearing temperature | Stable and within the manual range |
| Feeder delivery | Consistent material flow without bridging |
| Belt condition and tension | Within the manual specification |
| Die and roller surfaces | No baked material, no new discoloration |
| Pellet quality | Consistent with the historical baseline |
If the squeal returns at reduced feed rate, stop and check in this order before increasing feed:
- Squeal location and behaviour against the tables above.
- Feeder delivery and die temperature.
- Belt condition and tension.
- Bearing temperature and noise.
- Die and roller surface condition.
If all five checks are within the manual specification and the squeal still occurs at reduced feed rate, do not increase feed. Stop the machine, record the conditions, and contact the supplier. Continuing to run at this point adds wear without correcting the cause.
Preventing Squeal Faults
A squeal fault is usually a maintenance condition that builds over time.
| Check | Suggested frequency | Purpose |
|---|---|---|
| Squeal at each area | Each shift | Detect a new squeal before it becomes a fault |
| Squeal and vibration against the baseline | Each shift, or per the manual | Confirm whether the squeal has changed objectively |
| Belt tension and alignment | Weekly, or per the manual | Prevent belt slip |
| Belt surface condition | Weekly | Detect glazing and wear before slip starts |
| Bearing temperature and lubrication | Each shift, or per the manual | Detect bearing problems before failure |
| Roller free rotation | Weekly, with the machine locked out | Detect roller bearing problems |
| Feeder delivery and hopper level | Each shift | Prevent a dry die |
| Die temperature | Continuous, or each shift where no sensor is fitted | Detect a dry die before it damages the die surface |
General maintenance intervals should follow the machine manufacturer manual.
Spare Parts to Hold for Squeal Events
Squeal events can require replacement parts rather than adjustment. Exact part numbers and recommended stock levels must come from the machine manual and the supplier spare parts list.
| Spare part | Why it is needed after a squeal event |
|---|---|
| Belt | Glazing, cracking, or wear from slip |
| Pulley | Groove wear from slip and misalignment |
| Roller bearings | Early failure or heat exposure |
| Main shaft bearings | Early failure or heat exposure |
| Die and rollers | Baked material or surface damage from a dry die |
Whether the die, rollers, belt, pulley, or bearings need replacement depends on belt wear, pulley groove wear, bearing temperature and noise, die hole entrance diameter change, roller surface condition, and pellet density decline against the historical baseline. The limits must come from the machine manual and the supplier documentation, not from a general figure.
When a Squeal Is a Configuration Problem
If a squeal recurs despite belt condition, bearing condition, feeder delivery, die temperature, and die and roller condition all being confirmed within range, the machine configuration may not match the material or the operating pattern. Confirmation must come from the machine manual, a pelletizing test, and the supplier documentation.
This is more common when a machine selected for one material is now running a denser or more abrasive material, or when a machine selected for intermittent operation is now running continuous production.
In that case, operating adjustments will reduce how often the squeal occurs but will not eliminate it. The options are to change the die and roller configuration, or to change the drive configuration. A pelletizing test with the actual material is the most reliable way to confirm which option is suitable before making a change.
If the squeal cannot be located on site, send the material type, moisture, particle size, die specification, roller condition, feed rate, motor current at normal operation, squeal location, squeal behaviour with load, die temperature trend, bearing temperature, belt type and condition, and the conditions under which the squeal appears for a configuration review.
Maintenance parameters, torque specifications, belt tension values, temperature limits, and acceptance criteria in this article must be confirmed against the machine manual, the control cabinet setting, and the die, roller, belt, and bearing supplier documentation. This article does not provide universal values for these items.