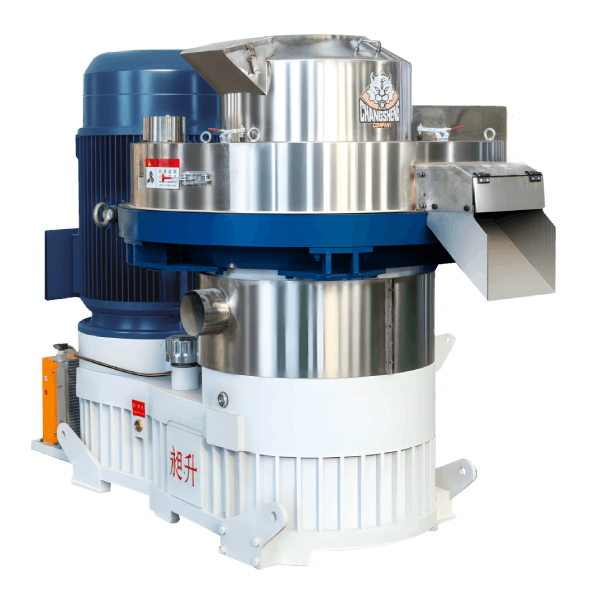
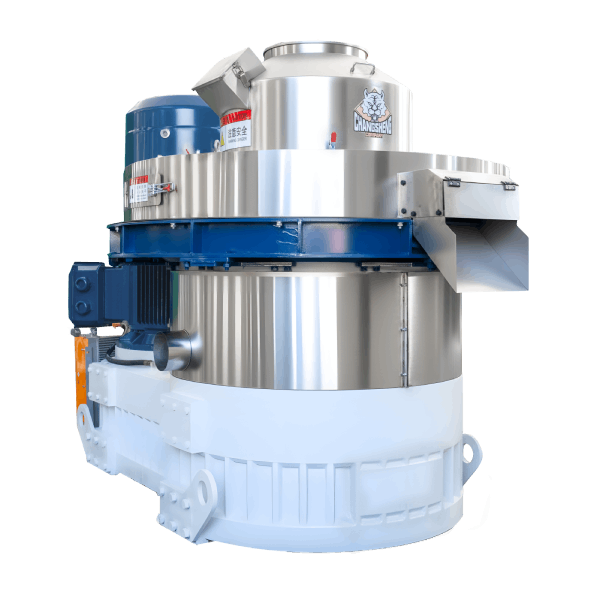
Biomass Hammer Mill for Pellet Production: Selection Guide
News 2026-07-16
A hammer mill for biomass pellet preparation is selected from the finished particle size, the material, the moisture, the screen, the motor power, and the pellet mill it feeds. That is the usual basis, but a special material, a special layout, or a special dust requirement can add other factors, and the test result and the supplier documentation decide the final configuration. The mill is not selected from the motor power alone, and a power figure without the material and the screen is a reference rather than a capacity commitment. If a supplier quotes a power figure without the material and the screen, the buyer should ask for the test result or the calculation behind it, stating the material, the screen, the moisture, and the throughput.
The particle size the mill produces affects the feed flow, the conditioning, the die wear, and the pellet quality, and the size is set by the screen and confirmed by a test.
This guide is written for procurement professionals and project engineers selecting a hammer mill for a biomass pellet line. It covers what the mill does, how to select the screen, how the material and the moisture affect the performance, how the motor power and the throughput are related, how to match the mill to the pellet mill, how to read the energy and the wear, how to handle the dust and the line integration, and what to confirm before the equipment is ordered.
What Does a Hammer Mill Do in Biomass Pellet Production?
The hammer mill reduces the raw material to a particle size that the pellet mill can accept. The reduction is made by the hammers that strike the material against the screen, and the material leaves the mill when it is small enough to pass through the screen openings.
The particle size it produces affects the process in three ways.
- The feed flow. A uniform particle size flows evenly into the die chamber, and an uneven size produces an uneven fill and a fluctuating load.
- The conditioning. A smaller particle has a larger surface area, which helps the steam and the heat reach the material and soften the lignin.
- The die wear and the pellet quality. A uniform particle compresses evenly, and an oversized particle blocks the die entry and increases the wear at that point.
Hammer Mill vs Other Grinding Equipment
The hammer mill is one grinding option among several, and the choice depends on the material and the target size.
| Equipment | How it works | When it fits |
|---|---|---|
| Hammer mill | Impact grinding by rotating hammers against a screen | Most biomass, including wood, straw, and husk, and a wide range of particle sizes |
| Knife mill | Cutting by rotating knives | Materials that need a cutting action, such as some fibrous materials that wrap in a hammer mill |
| Roller mill | Compression between rollers | Materials that need a narrow size distribution, and where the material is not too fibrous |
The hammer mill is the common choice for biomass pellet preparation because it handles a wide range of materials and produces a range of particle sizes by changing the screen. A material that is very fibrous and wraps around the rotor may need a knife mill or a special rotor, and a material that needs a very narrow size distribution may need a roller mill.
How to Select the Right Screen Size
The screen size is the main control on the finished particle size, and it is selected against the target size the pellet mill needs.
| Target application | Screen opening to start with | What to observe |
|---|---|---|
| Wood pellets, standard | 3–6 mm | The particle size distribution after the mill, and the flow into the die |
| Wood pellets, fine | 2–3 mm | The fines content and the conditioning behaviour |
| Agricultural biomass | 4–8 mm | The fibre length and the flow into the die |
| Rice husk pellets | 3–4 mm | The particle size and the wear on the screen |
The screen opening is an important factor in the particle size, but it is not the only one. The particle size also depends on the material, the hammer condition, the rotor speed, and the screen wear. The screen is a starting point for the selection, and the actual result is confirmed by the test.
How to Verify the Required Particle Size
The particle size is verified with a sieve analysis on a sample of the mill output, and the result is compared with the target size. The test should state the material, the moisture, the screen, the hammer condition, the rotor speed, and the sample size, so that the result can be compared with the production.
Screen Selection and Test Record
| Selection factor | What to record |
|---|---|
| Material type | The wood, the husk, the straw, or the blend |
| Target particle size | The size the pellet mill requires |
| Screen opening | The screen used in the test |
| Feed condition | The initial size, the moisture, and the contaminants |
| Measured result | The particle size distribution, the throughput, and the energy |
| Downstream verification | Whether the output meets the pellet mill requirement |
The table is a selection and test checklist. Where a test record exists, the measured values are entered. Where it does not, the table is completed during the trial, and the result is not assumed.
How Feedstock Moisture and Material Type Affect Performance
The material and the moisture change the mill performance more than the motor power.
| Material | What it does in the mill | What to check |
|---|---|---|
| Wood and sawdust | Grinds relatively easily, and the fibre is not too abrasive | The screen and the hammer condition |
| Rice husk | The mineral content and the abrasiveness increase the wear on the hammer and the screen | The hammer and the screen wear, and the cleaning before the mill |
| Straw and fibrous residues | The fibre can wrap around the rotor, and the grind is more difficult | The rotor design, the anti-wrapping feature, and the screen |
| Contaminated material | The sand and the stones accelerate the wear and can damage the screen | The cleaning before the mill, and the screen condition |
The rice husk is often described as high in silica, and the mineral content does increase the wear, but the exact content depends on the source and the test basis, and it should be confirmed by a chemical analysis or an ash analysis. The mineral content should not be assumed from the material name, and the wear rate should be confirmed by the wear record.
Moisture Content
The moisture affects the grinding efficiency, the screen blinding, and the dust.
| Moisture range | What happens in the mill | What to do |
|---|---|---|
| Below 10% | Grinding is efficient, and the dust increases | Standard operation, with the dust control |
| 10–15% | The grind is good for most materials | Normal operation |
| Above 15% | The grinding is harder, and the screen can blind | Reduce the feed rate, and consider pre-drying |
| Above 20% | The performance falls, and the blockage risk rises | Pre-drying is usually required |
When the material is outside the range, the response is to reduce the feed rate, to consider pre-drying, and to check the screen for the blinding. The moisture range is a general guide, and the actual range and the pre-drying requirement should come from a test on the material and the mill manual, not from a fixed value applied to every material.
Hammer Mill Motor Power and Throughput
The motor power and the throughput are related, but the throughput is not determined by the power alone. The throughput depends on the material, the moisture, the screen, the feed stability, the hammer condition, and the target particle size. A power figure without those conditions is a reference rather than a capacity commitment.
| Specification | What to confirm | Why it matters |
|---|---|---|
| Motor power | The power proposed for the material, the screen, and the target output | The power alone does not define the throughput |
| Rotor diameter and speed | The rotor diameter, the speed, and the tip speed | The tip speed is calculated from the diameter and the speed, and it affects the grind and the wear |
| Hammer configuration | The hammer number, the thickness, and the material | The configuration affects the grind and the hammer life |
| Screen | The screen opening and the screen area | The screen is the main control on the particle size |
| Feed system | The feeder type and the feed stability | An unstable feed produces an unstable output |
Rotor Speed and Tip Speed
The tip speed is calculated from the rotor diameter and the speed:
v = π × D × n ÷ 60
where v is the tip speed in m/s, D is the rotor diameter in metres, and n is the speed in RPM. The tip speed is used to compare the hammer impact energy between different rotor diameters and speeds, and the target value depends on the material and the target size. A range such as 80–110 m/s is a common reference, but it should not be applied without the rotor diameter, and the final value should come from the test and the manufacturer data.
How to Match the Hammer Mill with the Pellet Mill
The hammer mill is sized to feed the pellet mill, and the match is based on the material and the running pattern.
- Confirm the pellet mill target output and the running hours.
- Confirm the material, the initial size, and the moisture.
- Confirm the target particle size for the pellet mill.
- Select the mill capacity with a margin for the material variation, the screen wear, and the maintenance stops. A margin of 10–20% above the pellet mill demand is a common starting point, and the exact margin depends on the material, the running hours, and the maintenance plan, and it should be adjusted from the production record.
- Confirm the mill, the fan, and the conveying power against the line supply.
- Confirm the surge bin and the conveying capacity, so that the mill and the pellet mill can run at different rates.
A capacity figure should state the material, the moisture, the screen, and whether it is for the mill alone or the complete line.
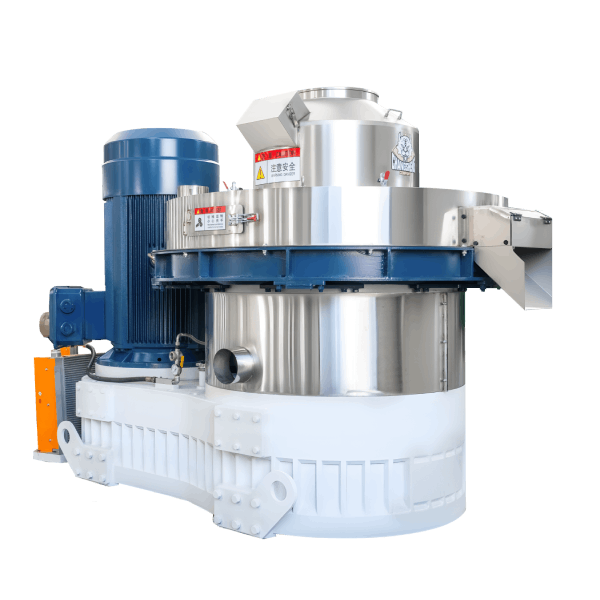
Selection Example
The following example shows the data a buyer should provide, not a delivered project.
| Item | Example entry |
|---|---|
| Pellet mill target output | The output and the running hours |
| Material | The type, the initial size, and the moisture |
| Target particle size | The size the pellet mill requires |
| Mill and fan power | The proposed power, with the calculation or the test |
| Operating pattern | Continuous or single shift |
| Auxiliary equipment | Screening, dust collection, and buffer storage |
The example is a data format. The actual figures come from the buyer’s material and the supplier’s test, and the result is confirmed by a trial.
Energy Consumption, Wear Parts and Maintenance
The energy and the wear are the two operating costs that follow the material and the screen.
What Affects Electricity Consumption
The energy per ton depends on the material, the moisture, the screen, the feed stability, the hammer condition, and the scope of the measurement. The figure should state whether it covers the mill only, or the mill with the fan and the conveying.
| Factor | Effect on the energy | What to do |
|---|---|---|
| Screen size | A smaller screen uses more energy | Use the largest screen that meets the particle size requirement |
| Feed rate | An unstable feed uses more energy | Keep the feed stable, and avoid the under- and over-loading |
| Hammer condition | Worn hammers use more energy | Rotate and replace the hammers at the planned interval |
| Air assist | The fan adds to the energy | Match the fan to the grinding requirement |
| Moisture | A higher moisture uses more energy | Pre-dry when the material requires it |
Hammer and Screen Wear
The hammer and the screen are wear parts, and their life depends on the material, the contaminants, and the operating conditions. A hammer life figure should state the material, the moisture, the screen, and the operating conditions it assumes. A rice husk or a contaminated material wears the parts faster than a clean softwood, and the difference should be confirmed by the wear record rather than assumed from a general figure.
How to Reduce Unplanned Downtime
- Keep the spare hammers and screens for the material in use.
- Record the hammer hours and the screen hours, and replace them at the planned interval.
- Check the screen for the wear and the holes at each maintenance.
- Keep the cleaning stage before the mill working, so that the sand and the metal do not reach the mill.
Dust Collection and Production Line Integration
The mill produces dust, and the dust is a health and an explosion hazard.
| Component | Purpose | What to confirm |
|---|---|---|
| Feeder | Regulated material input | Variable speed, and an anti-bridging design |
| Air assist | Discharge of the ground material | The fan capacity, and the cyclone or the filter |
| Cyclone or bag filter | Dust collection | The filter area and the explosion protection |
| Surge bin | Buffer between the mill and the pellet mill | The capacity, in minutes of the pellet mill demand |
| Conveying | Transfer to the pellet mill | The pneumatic or the mechanical type, and the distance |
| Dust hazard protection | Explosion venting, isolation, and grounding | The dust hazard assessment and the applicable standard |
The dust hazard measures should follow from a dust hazard assessment on the actual material, and the assessment should use the dust explosion testing, the material data, and the process conditions, with the applicable standard and a qualified assessor. A dust collector, a vent, or a grounding strap is one measure among several rather than a complete protection scheme.
Hammer Mill Selection Checklist
| Item | What to confirm |
|---|---|
| Material | Type, source, initial size, moisture, and contaminants |
| Target particle size | The size the pellet mill needs, and the screen to start with |
| Throughput | The required output, and the margin for the material and the maintenance |
| Motor power | The power proposed, and the test or the calculation behind it |
| Rotor and hammer | The rotor diameter, the speed, the tip speed, and the hammer configuration |
| Screen | The opening, the area, and the replacement plan |
| Dust control | The collector, the filter, and the explosion protection |
| Integration | The feeder, the conveying, the surge bin, and the pellet mill match |
| Supply | The voltage, the frequency, and the installed load |
| Service | The spare parts, the hammer and screen stock, and the warranty |
Frequently Asked Questions
How often should the hammers be replaced or rotated?
The interval depends on the material, the contaminants, and the operating conditions. The hammer and the screen life should be confirmed by the wear record for the same material, and the rotation and the replacement should be planned from that record rather than from a general figure.
What is the typical energy consumption for biomass hammer milling?
The energy per ton depends on the material, the moisture, the screen, the feed stability, and the scope of the measurement. A figure should state whether it covers the mill only or the mill with the fan and the conveying, and a figure without those conditions cannot be compared with another figure.
What particle size is required for biomass pellet production?
The particle size depends on the material and the pellet mill, and a common range is 2–5 mm before the pellet mill. Wood is usually 2–4 mm, and the agricultural residues may be 3–5 mm, but the correct size should come from the pellet mill requirement and a test on the material.
How do I size a hammer mill for my pellet line?
The mill is sized to feed the pellet mill with a margin for the material variation, the screen wear, and the maintenance stops. A margin of 10–20% above the pellet mill demand is a common starting point, and the exact margin depends on the material, the running hours, and the maintenance plan.
What screen size should I use for wood pellets?
A 3–6 mm screen is a common starting point for wood pellets, and a finer screen is used for a finer product. The screen opening is an important factor, but the actual particle size also depends on the material, the hammer condition, the rotor speed, and the screen wear, and it should be confirmed by a sieve analysis.
Request a Hammer Mill Configuration for Your Biomass
Send the material type and source, the initial size, the moisture, the contaminants, the target particle size, the pellet mill output, the running hours, the power supply, and the dust control requirement. A mill configuration and a line proposal can then be prepared against the actual material rather than against a general table.
Capacity figures, power figures, particle size values, energy figures, and acceptance criteria in this article must be confirmed against the material test report, the machine manual, the screen and hammer supplier documentation, and the applicable dust and electrical standards. This article does not provide universal values for these items.