New Die Not Producing Pellets: Causes, Fixes and What to Check First
News 2026-11-10
A new die that does not produce pellets is one of the most common complaints in the first days after a die change, and it is rarely a defective die. The die has to be run in before it produces a saleable pellet, the roller gap has to be reset on every roller after the change, the moisture has to be tuned to the new die, and the die temperature has to reach the operating range before the output is judged. The operator who changes the die again, or blames the machine, before the break-in is finished usually makes the problem worse.
This page is about a new die after a die change, and the checks are focused on the die, the roller gap after the change, the die specification against the order, and the die change sheet, while a new machine and a low formation rate are covered on their own pages with their own checklists. It is written for the operator and the maintenance engineer who have just fitted a new die and are trying to get it to run.
The short answer
A new die that does not produce pellets is caused by one of six things: the die has not been run in, the roller gap is not set correctly for the new die, the moisture at the die is outside the workable range, the feedstock is not what the die was selected for, the die temperature has not reached the operating range, or the die specification does not match the order.
The practical rule: run the die in with a prepared loading material, set the roller gap on every roller, hold the moisture at the die, bring the die temperature into the range, and check the die specification against the order before the output is judged. A new die that produces nothing in the first hours is a normal break-in symptom, and a new die that still produces nothing after a proper run-in and the six checks below is a real fault.
Why a new die produces nothing at first
A new die is not the same as a run-in die, and the difference is in the hole surface and in the compression.
A new die has hole surfaces that are rougher and entry edges that are less polished than a run-in die, and the material does not slide through them as easily. The resistance is higher, the throughput is lower, and the pellet does not form until the die is polished by the material passing through it.
The die temperature also takes time to reach the operating range, because the die body has to heat up through the friction of the material, and a cold die does not soften the lignin enough to bind the pellet. A new die fed production material at full rate before it is warm produces dust and unformed material, and the operator often reads this as a die fault.
The die change itself is the other reason. A die that has just been fitted has a new roller gap and a new seating, and the gap has to be reset and re-checked after the first hours, because the new parts settle under the initial load.
The six causes and how to tell them apart
| Cause | What points to it | What to check |
|---|---|---|
| Die not run in | Nothing forms in the first hours, and the die is new | Whether a prepared loading material was used before the production material |
| Roller gap not set | Material passes without being pressed, and the die stays cool | The gap on every roller against the manufacturer’s specification |
| Moisture outside the range | The material slips (too wet) or comes out as dust (too dry) | The moisture at the die inlet, not at the dryer outlet |
| Feedstock not matching the die | The material is coarser, wetter, or more abrasive than the die was selected for | The particle size, the moisture, and the contamination against the die specification |
| Die temperature not reached | The die stays below the operating range, and the pellets are soft or absent | The die temperature against the range recorded on the previous run |
| Die specification not matching the order | The die has been run in properly and the five other checks are correct, but nothing forms | The hole diameter, the compression ratio, the effective working length, and the material against the order |
How to run in a new die
The run-in is the step that most operators rush, and it is the step that decides whether the new die produces pellets or blinds.
The loading material is normally a dry material of the same family as the production material, prepared so that it slides through the die holes. The loading starts at a low feed rate and continues until the die is producing pellets steadily at the operating temperature and the current has stabilized. The production material is introduced only after that, and the feed is then brought up in steps rather than in a single jump.
The loading should not be skipped on the assumption that the new die is the same as the old one. A die that matches the old one on the diameter and the compression ratio is still a new die, and the material, the heat treatment, and the effective working length should also be confirmed before it is assumed to behave like the old one.
How to set the roller gap on a new die
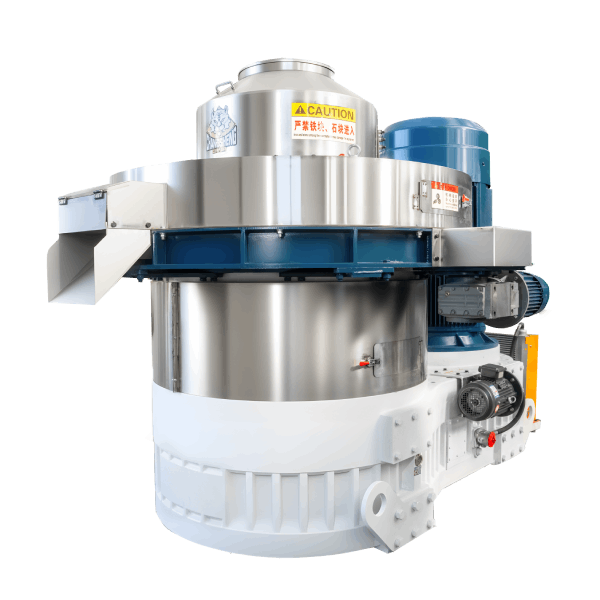
The roller gap is set on every roller, not on one, and it is set to the manufacturer’s specification for the new die. The gap is checked again after the first hours of running, because the new parts settle and the gap opens.
A gap that is too wide leaves the material unpressed and the die produces nothing; a gap that is too tight overloads the motor and blinds the die. The gap should be recorded on the die change sheet, so that the next check can be compared with the setting.
How to check the moisture and the feedstock
The moisture is measured at the die inlet, not at the dryer outlet, because the material changes between the two points. The target is set from the break-in on the new die rather than taken from the old die, because the new die has a different workable range.
The feedstock is checked against the specification the die was selected for: the particle size against the die hole diameter, the moisture against the die range, and the contamination against the die’s tolerance. A material that is coarser, wetter, or more abrasive than the specification will not form on a new die even after a proper run-in.
How to bring the die temperature into the range
The die temperature is brought into the range by the feed rate rather than by forcing the output. A die that is below the range is fed more slowly until the friction raises the temperature, and a die that is above the range is fed more slowly until the temperature settles. The temperature is monitored against the range recorded on the previous run, and it is recorded on the die change sheet.
How to check the die specification against the order
The die specification is checked against the order before the die is blamed on the machine. The hole diameter, the compression ratio and its definition, the effective working length, and the die material should be compared with the order and with the die that was removed.
A die that is the wrong diameter, the wrong compression ratio, or the wrong material will not produce the expected pellet regardless of the run-in, and the specification should be checked against the order before the machine is inspected. The compression ratio definition varies between suppliers, so the effective working length should be compared rather than the ratio number alone.
When it is a fault and not a break-in
A new die that still produces nothing after a proper run-in and the six checks is a fault, and the feeder, the roller gap, the die seating, and the drive should be checked in that order.
The feeder is checked first, because a feeder that does not deliver the material to the die looks like a die that does not form. The roller gap is checked second, because a gap that has opened after the first hours looks like a die that has stopped working. The die seating is checked third, because a die that is not seated correctly does not receive the pressure. The drive is checked last, because a drive problem is the least common cause and it shows as a motor overload rather than as a die that does not form.
What to record on the die change sheet
The die change sheet is what turns the next die change from a guess into a procedure, and it should record the die specification, the roller gap on every roller, the moisture at the die, the feedstock, the die temperature, the loading material, the loading duration, the first production output, and the pellet quality.
The sheet is compared with the next change, and a die that behaves differently from the record is a die that has changed, and the change is traced to the cause rather than to a general suspicion.
What to specify when buying a replacement die
Before the die is ordered, confirm the machine model, the die dimensions, the die hole diameter, the compression ratio and its definition, the effective working length, the die material and heat treatment, and the expected life on the specified material. Ask the supplier to state the roller gap setting for the new die, the loading material recommendation, and the run-in procedure, and to confirm the acceptance terms if the die does not reach the agreed life.
A die that is the correct dimension but the wrong compression ratio or the wrong material will not produce the expected pellet, and the lower price is not a saving over the replacement cycle.
If you have fitted a new die and it is not producing pellets, send the die specification and the order, the roller gap setting, the moisture at the die, the feedstock, the die temperature record, and the loading procedure, and the Shandong Changsheng Machinery team can review the run-in and the settings and propose the correction and the acceptance test.
Bottom line
A new die that does not produce pellets is usually a run-in problem, not a defective die, but the die specification against the order should be checked before the machine is inspected. The die has to be run in with a prepared material, the roller gap has to be set on every roller and re-checked after the first hours, the moisture at the die has to be set for the new die, the feedstock has to match the die specification, the die temperature has to reach the operating range, and the die specification has to match the order before the output is judged. A new die that produces nothing in the first hours is a normal break-in symptom, and a new die that still produces nothing after a proper run-in and the six checks is a fault, with the feeder, the roller gap, the die seating, and the drive checked in that order. Record the die specification, the gap, the moisture, the feedstock, and the temperature on the die change sheet, and specify the roller gap, the loading material, the die specification, and the run-in procedure when the die is ordered, so that the next change is planned rather than forced by a failure.